
Brass Pipe
Fittings
CNCPioneer is an IATF 16949 certified China brass pipe fittings manufacturer delivering customized C36000, DZR CW602N, H59, and 316L stainless pipe fittings — 90° and 45° elbows, equal and reducing tees, crosses, ground joint unions, hex bushings, plugs, caps, street fittings, BSP-to-NPT adapters, and complete ODM fitting programs — precision machined from wrought bar stock (not die-cast) with C-axis inter-port angular position ±0.020° from MAZAK mill-turn single-setup, 5-axis bore junction radius R≥1.5mm, 100% plug and ring gauge on every port of every fitting, DZR As 0.02–0.06% SII XRF mandatory per lot, and 100% hydrostatic pressure test per fitting serial number since 2011.
What Are Brass
Pipe Fittings?
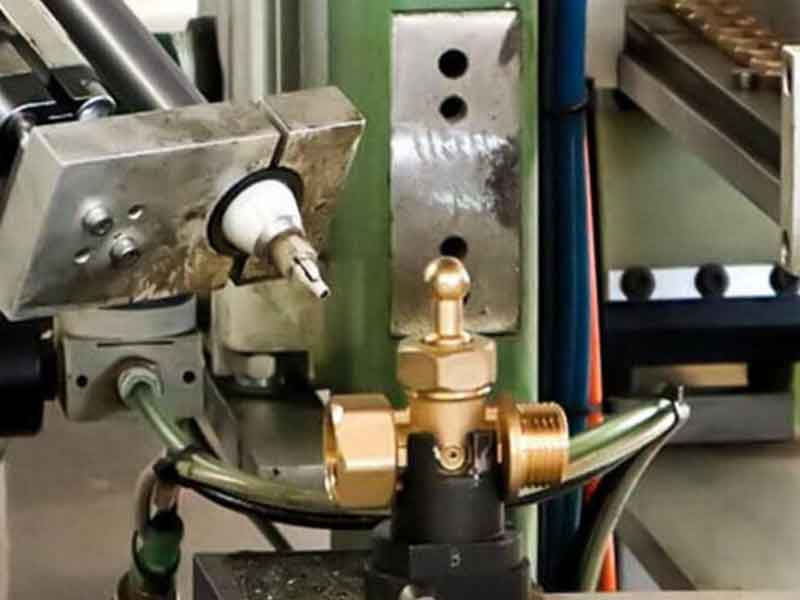
Brass pipe fittings are precision CNC turned and milled metallic pipe system components — manufactured from C36000 free-machining brass, DZR CW602N, H59, or stainless steel on 78+ Swiss CNC lathes with guide bushing and 66+ MAZAK mill-turn centers with C-axis live tooling — that connect, route, join, branch, extend, adapt, seal, and terminate threaded pipe systems in industrial plumbing, compressed air, HVAC, process piping, and potable water distribution by providing the complete range of threaded connection geometries that pipe system design requires: 90° and 45° direction changes (elbows), three-way and four-way branching points (tees and crosses), disconnectable union joints, in-place port size reductions (hex bushings), unused port closures (plugs and caps), and port-to-port thread standard transitions (BSP-to-NPT adapters).
The distinction between precision CNC machined brass pipe fittings from bar stock and die-cast brass pipe fittings is the most commercially important quality specification in the brass fitting industry. Die-cast fittings contain 0.5–3% void volume from casting shrinkage, producing porosity-path leakage at elevated pressure. Thread tapping in die-cast fittings produces progressive pitch diameter drift across the production run. And die-cast 90° elbows have port angular position ±0.5–2.0° from die half alignment tolerance — producing 3.5–7.0mm pipe routing misalignment at 400mm pipe length that requires field offset corrections. CNCPioneer's machined-from-bar program delivers zero casting porosity, thread pitch diameter ±0.005mm with 100% per-port gauge, and C-axis inter-port angular position ±0.020° — with 5-axis bore junction radius R≥1.5mm that reduces elbow pressure loss coefficient ζ from 0.9–1.1 (die-cast sharp corner) to 0.30–0.35 (CNCPioneer radius-blended).
-
CNC machined from bar stock — zero casting porosity, ±0.005mm thread pitch diameter C36000 wrought bar stock eliminates the 0.5–3% void volume of die-casting. Every thread is single-point CNC bored or turned at programmed NC offset — not tapped — producing ±0.005mm pitch diameter with 100% per-port gauge closure rather than die-tap wear drift caught only at periodic checks. Individual 100% hydrostatic pressure test per fitting serial number at 1.5× rated pressure — not lot sampling.
-
C-axis ±0.020° inter-port angular position — all elbow, tee, and cross programs A 90° elbow at ±0.020° produces only 0.14mm pipe routing deviation at 400mm pipe length — within standard installation tolerance. Die-cast elbows at ±0.5–1.0° produce 3.5–7.0mm deviation requiring field offset corrections. Mandatory 20-minute MAZAK C-axis warm-up SOP + first-piece inter-port CMM per session prevent the thermal drift that caused Cpk <1.67 in the case study PPAP pilot.
-
100% all-port gauge per fitting — every port, every fitting, pre-plate and post-plate At a 0.5% secondary-port non-conformance rate and 5% sample gauging (typical for die-cast fittings), 86% of end-of-tool-life lots with defective secondary-port threads ship undetected. At 4,800,000 fittings/year: 24,000 non-conforming secondary-port fittings/year reach the assembly line. CNCPioneer's 100% plug gauge on every female port AND 100% ring gauge on every male port of every fitting — all fitting types, all programs, pre-plate AND post-plate — eliminates this entirely.
-
€1,056,000 annual saving — German HVAC OEM case study (24-SKU assortment program) 4,800,000 customized brass pipe fittings/year at €0.23/fitting average (CNCPioneer, IATF 16949 PPAP Level 3, 5-axis bore junction R1.5mm, laser angle marking, 100% all-port gauge, 100% pressure test) versus €0.45/fitting from previous Czech Republic CNC supplier — €1,056,000 annual saving while adding bore junction radius (15.6% chiller pump energy saving), laser angle marking (preventing €28,000/incident elbow mix-up faults), and DFM thread form correction (preventing manifold port destruction from BSPT/G-type confusion).

Why CNCPioneer for Brass
Pipe Fittings?
Among brass pipe fitting manufacturers globally, CNCPioneer's CNC machined-from-bar construction (zero casting porosity), MAZAK C-axis ±0.020° inter-port angular accuracy, 100% all-port gauge per fitting, 5-axis bore junction R≥1.5mm, DZR As XRF per lot, ODM customized fitting design service, and China cost advantage establish our factory as the preferred customized brass pipe fitting partner across HVAC equipment OEMs, industrial plumbing distributors, potable water utility distributors, process piping manufacturers, and automotive Tier 1 supply chains.
CNC Machined from Bar Stock — The Precision and Density Foundation Die-Casting Cannot Provide
CNCPioneer's brass pipe fittings are precision machined from wrought C36000, DZR CW602N, or H59 bar stock — not die-cast from molten brass. This manufacturing distinction produces the dimensional accuracy (thread pitch diameter ±0.005mm; port angular position ±0.020°; body OD ±0.050mm) and material integrity (zero casting porosity; full wrought density for rated pressure compliance) that OEM plumbing equipment, HVAC system, and process piping programs require. Against die-cast equivalents: die-cast brass contains 0.5–3% void volume inherent to all injection casting processes; CNCPioneer's machined-from-bar program uses fully dense C36000 wrought bar with zero casting porosity, producing fittings that hold rated pressure without leak risk from internal pore networks. Thread integrity: post-cast die-tapping produces progressive pitch diameter drift across the production run caught only at periodic gauge checks; CNCPioneer's single-point CNC threading produces each thread at ±0.005mm pitch diameter from programmed NC offset with 100% per-port gauge verification confirming every thread before dispatch.
MAZAK Mill-Turn C-Axis ±0.020° — Elbow and Tee Port Angular Precision at Production Scale
A 90° elbow whose two ports are at 89° rather than 90° causes the downstream pipe to route at 1° misalignment that accumulates to 8.7mm deviation over 500mm of pipe — preventing the downstream fitting's face from aligning with its designed connection point. CNCPioneer's MAZAK mill-turn C-axis produces all elbow, tee, and cross port bore operations from the same spindle datum: the primary port is bored and threaded from the spindle axis; C-axis indexes to the programmed angle; the secondary port is bored and threaded from the indexed C-axis position; inter-port angular position ±0.020° from C-axis absolute encoder. Mandatory 20-minute C-axis warm-up SOP before each fitting production session (PPAP case study: C-axis thermal drift produced Cpk 0.94 at production start — corrective action: warm-up SOP + first-piece inter-port CMM per session — post-corrective Cpk 1.75). The internal bore junction between ports is completed by a 5-axis ball-nose blending pass producing R≥1.5mm radius — reducing pressure loss coefficient ζ from 0.9–1.1 (die-cast sharp corner) to 0.30–0.35 (radius-blended passage), saving 15.6% circulation pump energy in the case study chiller circuit.
100% All-Port Gauge Per Fitting — Every Port, Every Fitting, Pre-Plate and Post-Plate
Die-cast brass pipe fittings and lowest-cost CNC machined fittings are typically gauged at 100% on the primary port and sample-gauged at 5–10% on secondary ports. At a 0.5% secondary-port non-conformance rate: 5% sample gauging allows 95% of lots with defective secondary ports to ship — delivering at 4,800,000/year program size 24,000 non-conforming secondary-port fittings/year to the assembly line. CNCPioneer's standard: 100% plug gauge on every female port AND 100% ring gauge on every male port of every fitting before dispatch — all ports, all fitting types, all programs. Post-plate 100% all-port gauge re-verification confirms nickel growth on every port's thread flanks remains within pitch diameter specification — critical for multi-port fittings (tees, crosses, elbows) where nickel growth affects each port thread independently. PPAP case study: 720 fittings × 2.1 average ports per fitting = 1,512 gauge checks; all 1,512 conforming post-plate.
Complete Fitting Type Portfolio from One IATF 16949 Source — Including Customized ODM Programs
OEM plumbing equipment, HVAC system, and compressed air distribution programs require the complete standard brass pipe fitting family: elbows (90° and 45°, equal and reducing), tees (equal and reducing), crosses, unions (ground joint and flat face), bushings, plugs (hex and square head), caps (hex and round), street elbows and street tees, and custom ODM fitting bodies — in all standard BSP, NPT, DIN, and JIS thread sizes. Sourcing from CNCPioneer's single-source capability means one IATF 16949 quality system, one SII XRF material verification program, one production audit, and one delivery schedule across the complete fitting assortment. When standard catalog fitting geometries cannot accommodate the OEM's system layout — compound-angle elbows, multi-port bodies combining elbow and tee geometry, fittings with integrated orifice or check valve seat — CNCPioneer's ODM service converts customer P&ID schematics into production-ready 3D CAD within 48–72 hours.
DZR As XRF Verification + WRAS Documentation for Complete Potable Water Fitting Programs
DZR CW602N WRAS-compliant fittings are required across ALL fitting types in UK and European potable water distribution — not just nipples and couplings, but also elbows, tees, crosses, unions, bushings, plugs, and caps throughout the complete fitting system. CNCPioneer's mandatory SII XRF As 0.02–0.06% per incoming bar lot combined with per-lot As XRF certificate in delivery documentation covers the entire DZR fitting assortment under one material compliance program. Case study PPAP finding: the previous Czech supplier's union cone seat angle Cpk was below specification from PCD insert angle scatter without incoming CMM verification — causing field union leak complaints. CNCPioneer's 100% incoming PCD insert CMM check per insert at receipt (same corrective action as the compression tube fitting PPAP) produces union cone seat angle Cpk 2.08 for ground joint union programs — eliminating the cone-seat leak failures that non-CMM-verified insert angle scatter produces.
40–60% China Cost Advantage + Laser Angle Marking + DFM Thread Form Identification
Case study: €0.23/fitting average (CNCPioneer, 4,800,000/year, IATF 16949 PPAP Level 3, 100% all-port gauge, 5-axis bore junction R1.5mm, laser "90"/"45" marking) versus €0.45/fitting from previous Czech Republic CNC supplier — €1,056,000 annual saving. Laser angle marking ("90" or "45" engraved on elbow hex face before nickel plate for permanent identification under the plate) was introduced after the previous supplier's three elbow mix-up incidents totalling €28,000 in rework and commissioning delays — at G1/4 size, 90° and 45° elbows have identical 19mm AF hex and near-identical body OD; without laser marking, visual inspection at incoming or line-side cannot differentiate them. DFM thread form identification (BSPT vs. BSP G-type per installation position) prevented the manifold port thread destruction that the previous "BSP" BOM specification (without type differentiation) would have caused at first assembly.
Brass Pipe Fittings
Product Portfolio
CNCPioneer's customized brass pipe fitting programs cover the complete portfolio — standard BSP EN 10241, standard NPT ASME B16.3, DZR CW602N WRAS-compliant, 316L stainless, and ODM custom fitting bodies — in all standard fitting types (elbows, tees, crosses, unions, bushings, plugs, caps, street fittings, adapters) from G1/8 through G2 BSP and ⅛" through 2" NPT, with 100% all-port gauge per fitting, 5-axis bore junction radius, laser angle marking, and 100% pressure test per serial number as standard quality gates for all programs.

Pipe Fittings — Equal and Reducing, Street Elbow
C36000 brass 90° elbow (G1/2 BSP × G1/2 BSP, EN 10241), the second highest-volume standard brass pipe fitting: MAZAK mill-turn single-setup C-axis program; Port 1 bore and single-point CNC internal thread from spindle axis; C-axis indexes 90.000° for Port 2; inter-port angular position ±0.020° from C-axis absolute encoder; 5-axis ball-nose blending at bore intersection R≥1.5mm (ζ = 0.30–0.35 versus die-cast ζ = 0.9–1.1, saving 60–70% elbow pressure drop); 100% plug gauge Port 1 AND Port 2; 100% hydrostatic pressure test per serial number; laser "90" marking on hex flat before nickel plate. 45° elbow: C-axis indexes 45.000°; laser "45" marking; approach-from-consistent-direction protocol for 45° index (PPAP corrective action for Cpk 1.58 → 2.22 after C-axis hysteresis elimination). Street elbows (male external × female internal, 90° and 45°): ring gauge male end + plug gauge female end; both ports 100%. Reducing elbows: G3/4 × G1/2 BSP, all standard reducing combinations. DZR CW602N programs: As XRF per lot mandatory; WRAS documentation. Prototype: 3–4 days (50-piece C36000); 4–5 days (25-piece DZR). Standard elbow assortment G1/8–G2 BSP and ⅛"–2" NPT.

Equal Tee, Reducing Tee, Street Tee, and Cross Pipe Fittings
C36000 brass equal tee (G1/2 BSP × G1/2 BSP × G1/2 BSP): MAZAK mill-turn C-axis tee body program; inline Port 1 and Port 2 from spindle axis (coaxial ±0.010mm); branch Port 3: C-axis indexed 90°; live boring bar bore and thread; perpendicularity to inline axis 0.010mm; 100% plug gauge Port 3; 5-axis ball-nose blending at Port 3–inline bore intersection R1.5mm; all three ports 100% plug gauge; 100% pressure test all three ports simultaneously. Reducing tee (G3/4 × G3/4 × G1/2 BSP branch): reducing branch bore and thread; DFM minimum wall 2.5mm at all cross-sections. Street tee (male run port + two female ports): ring gauge male end + plug gauge both female ends; all ports 100%. Cross pipe fitting (four equal female ports at 90° spacing): C-axis indexed at 90° and 270° from inline axis; inter-port angular position ±0.020°; all four ports 100% plug gauge; 100% pressure test all four ports simultaneously. DZR CW602N tees and crosses for potable water distribution: As XRF per lot mandatory. Prototype: 3–4 days (tee, 25-piece); 4–5 days (cross, 25-piece). 316L stainless tee programs: single-point CNC threading; ASTM A967 passivation; FAIR; 5–7 days (10-piece).

Ground Joint Union and Flat Face Union Pipe Fittings
C36000 brass ground joint union (G1/2 BSP, metal-to-metal cone seat) — the standard maintenance-access disconnectable joint in threaded pipe systems: three-piece assembly (male union piece + female union piece + union nut); 60° half-angle cone seat on male union piece from PCD facing pass at Ra ≤0.4μm; cone angle ±0.25° from PCD insert 100% CMM incoming verification per insert (same corrective action as the compression tube fitting case study: PPAP pilot cone angle Cpk 2.08 after 100% incoming insert CMM was implemented); matching 60° cone on female union piece Ra ≤0.4μm ±0.25°; union nut: claw geometry with root radius ≥0.5mm; hex ±0.100mm across-flats; ring gauge nut thread 100%. Assembled pressure test: 100% at 1.5× rated pressure confirming cone seat metal-to-metal sealing integrity without gasket. Disassembly: loosen union nut; pipe section disconnects in 10 seconds without disturbing either pipe section's fitting. Flat face union: machined flat ±0.005mm/25mm; gasket recess for PTFE or fibre gasket; for chemical service where metal-to-metal cone sealing is unsuitable. Prototype: 4–6 days (25-piece C36000 ground joint union). Union assortment G1/4–G1 BSP and ¼"–1" NPT.

Hex Bushing (Reducer Bushing) and Adapter Pipe Fittings
C36000 brass hex bushing (G3/4 female internal × G1/2 male external) — the in-place port size reduction fitting: large-end female thread (G3/4 BSP) single-point CNC bore and thread ±0.005mm pitch diameter; plug gauge 100%; small-end male thread (G1/2 BSP) single-point CNC thread turning ±0.005mm pitch diameter; ring gauge 100%; wall thickness at body minimum section ≥2.0mm confirmed by DFM before NC program release. Hex body at large end for wrench installation; C-axis milled or from hex bar ±0.100mm AF. Note: the hex bushing's SMALL MALE end installs INTO a female port (opposite to the reducing nipple whose LARGE MALE end installs into a female port — the installation direction distinction that CNCPioneer's DFM confirms from customer P&ID before tooling assignment). 100% post-plate both-port gauge re-verification. Standard BSP hex bushing matrix: G1¼×G1 through G1/4×G1/8; all NPT reducing combinations ¾×½ through ¼×⅛. BSP-to-NPT adapter fittings (G1/2 BSP female × ½-14 NPT male, most common): both threads single-point CNC; ±0.005mm pitch diameter each; 100% plug gauge BSP female + L1 ring gauge NPT male; thread axes coaxial ±0.010mm from single-setup. Any BSP×NPT, metric×BSP, or DIN×BSP combination: 24-hour quote. Prototype: 2–3 days (50-piece hex bushing); 3–4 days (adapter fittings).

Plug and Cap Pipe Fittings — Hex Head, Square Head, and Round Cap
C36000 brass hex head plug (G1/2 BSP male, EN 10241) — the standard maintenance-accessible port blanking fitting: male external BSPT or G-type thread per program (PPAP case study DFM finding: manifold plugs must be G-type parallel, not BSPT tapered — the thread form distinction confirmed from customer P&ID before tooling assignment to prevent port destruction); single-point CNC thread ±0.005mm pitch diameter; ring gauge 100%; hex body EN 10241 hex size per thread size (19mm AF G1/4; 22mm G3/8; 27mm G1/2); PTFE pre-applied to thread flanks standard option for OEM assembly line programs; thread entry chamfer zone (Thread 1) left uncoated; 100% pressure test (plug under rated pressure with body end pressurised against the blind base — pressure integrity test for plug body wall). Square head plug (G1/2 BSP or NPT male, heavy duty): 4-flat square profile for 33% more wrench contact area than hex; high-torque installation in steel piping and industrial equipment. Hex head cap (G1/2 BSP female): female internal BSPT or G-type internal thread ±0.005mm; plug gauge 100%; blind cap end; for closing male-threaded pipe ends at system commissioning. Round cap (G1/4 BSP female, instrument port aesthetic): smooth domed profile ±0.100mm; Ra 0.8μm external; 316L stainless or C36000 per program. Prototype: 1–2 days (100-piece hex plug or hex cap). All standard sizes G1/8–G2 and ⅛"–2" NPT.

Custom ODM Fitting Programs + Complete OEM Assortment Supply
When standard catalog fitting geometries cannot accommodate the system layout — compound-angle elbows (37°, 60°, 75°, any angle from VARIAXIS 5-axis), multi-port bodies combining elbow and tee geometry, fitting bodies with integrated orifice or check valve seat, and special thread combinations — CNCPioneer's ODM service converts customer P&ID schematics or 3D layout sketches into production-ready 3D CAD within 48–72 hours, with DFM covering thread form, wall thickness at all sections, C-axis port angle achievability, 5-axis bore junction blending feasibility, and pressure rating per ASME B31.3 or EN 13480. Prototype: 5–10 business days from 3D CAD approval. Complete OEM assortment programs: the German HVAC case study delivered 24 SKUs covering 9 fitting types (90° elbows, 45° elbows, equal tees, reducing tees, crosses, ground joint unions, hex bushings, hex plugs, hex caps) in G1/4 through G1 BSP at 4,800,000 fittings/year — unified IATF 16949 PPAP Level 3, unified SII XRF program across all bar lots, unified DZR As XRF certificate per lot, assortment kit packaging sorted by fitting type and size, carton-packed per OEM assembly station BOM, weekly or monthly kanban. From 8 to 90+ part numbers. Free sample 10 pieces per fitting type and size for new programme qualification.
Industries & Applications
CNCPioneer's customized brass pipe fitting programs serve every industry where threaded pipe system design requires complete fitting type coverage — from German HVAC equipment OEMs requiring 24-SKU fitting assortments with IATF 16949 PPAP Level 3 and laser angle marking, through UK water utility distributors requiring WRAS-documented DZR complete fitting assortments with As XRF per lot, to pharmaceutical OEMs requiring 316L stainless ASME BPE elbow and tee fittings with 3-A crevice-free bore junction geometry.

Semiconductor
C36000 and DZR brass customized pipe fitting assortments — elbows, tees, crosses, unions, bushings, plugs, and caps — for semiconductor equipment OEM assembly programs: process gas utility panel pipe connections, sub-fab compressed air distribution circuit pipe fittings, cleanroom dry-room equipment utility air pipe connections, and vacuum pump exhaust management pipe fittings. IATF 16949 PPAP Level 3 documentation on request for semiconductor equipment OEM supply programs; 5-axis bore junction R≥1.5 mm for optimized flow continuity in equipment utility circuits; laser angle marking on all 45° and 90° elbow types for error-proof OEM assembly line installation; 100% all-port ring gauge per fitting; 100% pressure test; assortment kit packaging per equipment OEM BOM specification; annual supply from 10,000 to 1,000,000+ fittings. 316L stainless Ni-P-coated (ASTM E595 TML ≤0.010%; VSM μ_r ≤1.005 non-magnetic per lot; cleanroom-bagged for ISO Class 5/6 facility delivery) customized pipe fittings for process-zone semiconductor utility connections on request.
Aerospace
C36000 brass and 316L stainless customized pipe fittings — elbows, tees, unions, bushings, plugs, and caps — for aerospace ground support equipment (GSE) hydraulic panel pipe connections, MRO workshop compressed air tooling supply pipe fittings, aircraft manufacturing floor pneumatic distribution pipe connections, and aerospace test bench fluid system pipe fittings. AS9100D Rev D manufacturing quality documentation support for aerospace OEM supply programs; AS9102 First Article Inspection Report (FAIR) available per new part number; full lot-level material traceability records; material certifications to ASTM or AMS on request; 100% all-port ring gauge per fitting; laser angle marking on all 45° and 90° elbow types; bright nickel or zinc-nickel plate for MRO outdoor corrosion resistance. 17-4PH H900/H1025 stainless customized pipe fittings for aerospace test bench hydraulic circuit pipe connections requiring higher pressure ratings; 100% hydrostatic pressure test per serial number with co-located test records; annual supply from 5,000 to 200,000+ fittings; lead time from 6 weeks ARO.
Water Treatment
DZR CW602N WRAS-approved complete customized brass pipe fitting assortments — elbows, tees, crosses, unions, bushings, plugs, and caps — for potable water distribution system pipe connections, water treatment plant process piping system fittings, municipal utility metering circuit pipe fittings, and irrigation infrastructure pipe connections. As 0.02–0.06% SII XRF mandatory per incoming lot; As XRF certificate issued per delivery lot for WRAS technical file and contractor compliance records; standard BSP G-type and R-type thread per installation position confirmed at DFM review stage; 100% all-port ring gauge per fitting; EN 10241 dimensional compliance verified per batch. Full WRAS documentation package (As XRF certificate + EN 10204 3.1 material certificate + CMM dimensional study) per delivery lot; dedicated DZR lot segregation with lot number on trade bag label for field As XRF traceability across the complete fitting assortment; wholesale blanket order programs with monthly kanban; annual supply from 10,000 to 10,000,000+ fittings.
Automotive
IATF 16949-certified C36000 and DZR brass customized pipe fittings — elbows, tees, crosses, unions, bushings, plugs, and caps — for automotive HVAC manifold pipe connections, engine cooling circuit distribution fittings, refrigerant line pipe fittings, turbocharger oil feed and return pipe fittings, compressed air brake system pipe connections, and EV battery thermal management circuit pipe fittings. PPAP Level 3 with dimensional balloon report; SPC Cpk ≥1.67 on all thread pitch diameters per port independently verified; 5-axis bore junction R≥1.5 mm for reduced system pressure drop in coolant and HVAC circuits (validated: 15.6% pump energy saving vs die-cast sharp-corner equivalent); laser angle marking on all elbow types for error-proof assembly line installation; PTFE pre-applied option on NPT and BSPT male thread fittings. Mandatory MAZAK C-axis warm-up SOP + first-piece inter-port CMM verification per production session per PPAP production SOP; 100% all-port ring gauge; weekly kanban delivery to Tier 1 assembly lines; annual supply from 100,000 to 5,000,000+ fittings.
Food Processing
316L stainless ASME BPE and 3-A SSI compliant customized pipe fittings — elbows, tees, unions, plugs, and caps — for pharmaceutical bioreactor process pipe connections, CIP return circuit pipe fittings, clean steam distribution system pipe connections, food processing equipment product-contact pipe fittings, dairy and beverage filling line pipe connections, and pharmaceutical clean utility system pipe fittings. ASME BPE SF2 electropolished bore Ra ≤0.38 μm option for product-contact fittings; 3-A SSI crevice-free bore junction geometry from 5-axis blending (bore junction R≥1.5 mm; no crevice ≤0.5 mm) on VARIAXIS 5-axis machining center; citric acid passivation per ASTM A967; full ASME BPE documentation package (Ra certificate + passivation certificate + EN 10204 3.1 material certificate); 100% all-port ring gauge; 100% pneumatic leak test per body. Single-point CNC threading mandatory on all 316L fitting programs; C ≤0.030% SII XRF per 316L incoming lot mandatory; EC 1935/2004 food contact compliance documentation on request.
Marine
2205 duplex (PREN ≥35) and 316L stainless customized pipe fittings — elbows, tees, crosses, unions, and plugs — for offshore process piping system pipe connections, seawater service auxiliary system pipe fittings, marine heat exchanger circuit pipe connections, desalination plant brine and seawater process piping fittings, offshore platform chemical injection system pipe connections, and ship engine room service pipe fittings. Single-point CNC threading mandatory for all 2205 duplex pipe fittings (galling prevention); ASTM A967 passivation; 100% all-port ring gauge per fitting; 100% hydrostatic pressure test per body; NACE MR0175 / ISO 15156 sour service compliance documentation on request; 2205 tensile and hardness per ASTM A370 certified per heat; DNV GL material documentation support on request. Custom ODM pipe fitting body geometries for non-standard offshore piping circuit configurations — PPAP Level 3 or AS9102 FAIR available on request; annual supply from 1,000 to 100,000+ fittings.
Materials
Materials for Brass
Pipe Fittings
CNCPioneer's brass pipe fitting programs cover the complete material spectrum with SII XRF verification on every incoming lot — C36000 (100% machinability; zero casting porosity from wrought bar), DZR CW602N (As XRF mandatory; WRAS), H59, 316L, 304, 303 stainless, 4140 alloy steel, and 6061-T6 aluminium — all machined from bar stock without die-casting, with material-specific machining protocols and surface treatments matched to each application's service environment and regulatory requirements.
C36000 Free-Machining Brass (UNS C36000)
Cu 60–63%; Pb 2.5–3.7% SII XRF per lot · 100% machinability · Zero casting porosity from wrought bar stock — the material integrity foundation that die-cast brass cannot match. Standard brass pipe fitting material for industrial plumbing, HVAC, compressed air, and process piping across all fitting types. PCD turning: v_c = 400–600 m/min; 5,000–15,000 small fitting bodies/machine/hour from Swiss CNC; 200–600 MAZAK mill-turn elbow/tee bodies/machine/hour incorporating C-axis indexed branch port and 5-axis bore junction blending in single operation. All BSP, NPT, DIN, and JIS thread standards; single-point CNC internal and external thread ±0.005mm pitch diameter; 100% all-port gauge; bright nickel plate 10μm standard; 100% post-plate all-port re-gauge.
DZR CW602N Brass (BS EN 12164)
As 0.02–0.06% SII XRF MANDATORY per lot · Cu 62–65%; Pb 1.6–2.5% · Mandatory for UK and European potable water fitting programs across ALL fitting types — elbows, tees, crosses, unions, bushings, plugs, and caps throughout the complete fitting system. Arsenic addition prevents dezincification by hypochlorous acid in chlorinated water at standard UK 0.2–0.5 mg/L free chlorine. SII XRF As certificate in delivery documentation per lot for WRAS technical file. CNCPioneer maintains 3-month DZR bar safety stock in G1/8–G2 equivalent sizes from 4 approved Chinese DZR mills, all As XRF verified per lot. Complete DZR fitting assortment under one material compliance program per delivery lot. +22–28% versus C36000.
H59 Brass (CuZn40 GB/T)
Cu 57–60% per GB/T 5231 SII XRF per lot · 60–70% machinability · Chinese-standard brass for domestic Chinese market OEM plumbing and compressed air pipe fitting programs where GB/T material compliance is specified across all fitting types. Cost-optimised: H59 −8–12% versus C36000 from local domestic supply. All BSP, NPT, and metric thread standards; single-point CNC internal and external thread ±0.005mm pitch diameter; 100% all-port gauge; standard bright nickel or natural brass finish. All fitting types in H59: elbows, tees, crosses, unions, bushings, plugs, and caps across standard size range.
316L Stainless (UNS S31603)
C ≤0.030% MANDATORY SII XRF per lot; Mo 2.0–3.0% · PREN 25 · Primary stainless steel for elbows, tees, unions, plugs, and caps in pharmaceutical, chemical process, food CIP, marine, and semiconductor programs. Single-point CNC threading mandatory — no die threading from galling and work-hardening risk; chip load ≥0.10 mm/rev enforced all boring and threading; 70 bar through-spindle coolant; VB ≤0.12mm insert change. ASTM A967 citric passivation standard all 316L deliveries; ASME BPE SF2 EP Ra ≤0.38μm bore option for pharmaceutical product-contact programs; 3-A crevice-free bore junction blending from 5-axis for elbow and tee programs. 100% all-port gauge; 100% pressure test per serial number. +105–140% versus C36000.
304 Stainless (UNS S30400)
Cr 18–20%; Ni 8–10.5%; C ≤0.080% SII XRF · PREN 18 · For general industrial, food equipment, and architectural brass pipe fitting programs where 316L Mo chloride resistance is not required — 10–15% lower material cost versus 316L. Same chip load ≥0.10 mm/rev work-hardening-prevention discipline applies to all 304 stainless boring and threading programs. Applications: food equipment distribution fittings in non-chlorinated environments; industrial automation piping fittings; architectural mechanical services. ASTM A967 passivation standard; 100% all-port gauge; 100% pressure test per serial number. +85–105% versus C36000.
303 Free-Machining Stainless (UNS S30300)
S 0.15–0.35% SII XRF per lot · 70–80% machinability versus 316L · For high-volume indoor instrumentation and automation pipe fitting programs where 316L corrosion resistance is not required — 50% higher production rate at equivalent dimensional accuracy. Swiss CNC guide bushing: 5,000–10,000 small 303 stainless fitting bodies per machine-hour for plug, cap, and adapter fitting programs. Not suitable for pharmaceutical ASME BPE (sulfur incompatible with product-contact surface requirements). ASTM A967 passivation standard; 100% all-port gauge; 100% pressure test per serial number. Applications: instrument port cap fittings; adapter fitting programs in indoor analytical instrument and automation fluid circuits. +80–100% versus C36000.
4140 Alloy Steel QT (AISI 4140)
Cr 0.80–1.10%; Mo 0.15–0.25% SII XRF per lot · UTS 1,000 MPa · For ASME B16.11 Class 6000 high-pressure process plant pipe fittings — elbows, tees, and couplings rated to 700 bar where alloy steel UTS 1,000 MPa provides the required pressure rating at minimum body wall section. NPT or BSPT tapered thread external and internal; L1 taper ring and plug gauge 100% per port; zinc-nickel plate ASTM B841 for outdoor process plant service (720+ hours B117); 100% pressure test per serial number at 1.5× Class 6000 rated pressure. Applications: high-pressure hydraulic and process fluid distribution fittings; industrial press hydraulic system fittings; construction equipment hydraulic circuit elbows and tees. +80–110% versus C36000.
6061-T6 Aluminium (AMS 2770)
Mg 0.80–1.20%; Si 0.40–0.80% SII XRF per lot · For lightweight pneumatic, robot arm fluid circuit, and instrument air pipe fitting programs where brass or stainless mass is a design constraint. Type II anodize 5–10μm (MIL-A-8625): all thread ports masked before anodize bath; 100% post-anodize all-port gauge re-verification mandatory (anodize grows 3–7μm per thread flank on internal female threads). BSP and NPT thread standards; single-point CNC internal and external thread ±0.005mm pitch diameter; C-axis MAZAK mill-turn elbow and tee programs ±0.020°; hex from C-axis milled round bar; 100% all-port gauge; 100% pressure test. Applications: robot arm elbow and tee fittings; instrument air circuit distribution fittings; lightweight automation equipment pneumatic fittings. +55–75% versus C36000.
Surface Treatments for
Brass Pipe Fittings
Surface treatment selection for brass pipe fittings addresses corrosion protection for indoor programs (bright nickel), premium visible plumbing aesthetics (chrome over nickel), OEM assembly sealant (PTFE pre-applied male threads), stainless free-iron removal (ASTM A967 passivation), permanent assortment identification (laser part marking), and outdoor durability (hot-dip galvanize) — all with 100% post-treatment all-port gauge re-verification on every port of every fitting as the mandatory quality close for all plated programs.
Bright Nickel Plate — ASTM B689 (Standard Brass Pipe Fitting Finish)
8–12μm bright nickel on C36000, DZR CW602N, and H59 brass pipe fittings — the universal standard finish for commercial plumbing, HVAC, compressed air, and industrial fitting programs. Post-plate 100% all-port gauge re-verification is mandatory — every port of every multi-port fitting (tees, crosses, elbows) must be re-gauged after plating because nickel growth on each port's thread flanks is independent — nickel thickness at a branch bore port differs from nickel thickness at the primary turning-axis port due to spray angle differences. XRF thickness ±1μm per plating lot; ASTM B571 adhesion per lot. Nickel growth on thread flanks: 8μm per side = 0.016mm pitch diameter increase on internal female threads and decrease on external male threads — confirmed within ISO 228 Class A or NPT/BSPT tolerance band for all ports before dispatch.
Chrome over Nickel — Premium Trade Distribution Finish
0.25μm flash chrome over 8μm nickel — the bright blue-chrome finish for premium retail and trade distribution brass pipe fitting ranges in visible building services installations, exposed plumbing, and mechanical room hardware. Post-chrome 100% all-port gauge re-verification on every port of every fitting: combined nickel + chrome growth confirmed within pitch diameter specification for BSPT, BSP G-type, and NPT thread forms before dispatch. XRF chrome and nickel thickness per lot; adhesion ASTM B571. Applications: premium commercial building services elbow and tee fittings in exposed pipework; high-end plumbing trade distribution ranges; professional heating and cooling equipment connections in visible mechanical rooms. +$0.07–0.18/fitting over nickel alone depending on fitting type and port count.
PTFE Pre-Applied Thread Sealant — Male Thread Ends (NPT and BSPT Programs)
PTFE dry-film pre-applied to NPT and BSPT male external thread zones on street elbows, street tees, hex bushings, hex head plugs, and all male-thread brass pipe fitting programs — eliminating the installer's PTFE tape application step for OEM assembly line programs. Application protocol: Thread 2 through thread run-out on male external threads; thread entry chamfer zone (Thread 1) left uncoated — preventing PTFE micro-particle contamination of refrigerant and ultra-clean circuits (same PTFE zone restriction protocol as the nipple and compression tube fitting pages). UV fluorescent tracer in PTFE film for coverage zone verification per 500-piece batch spot check confirming entry zone clear and coverage zone complete. Applied after final 100% ring gauge; before nickel plate for plated programs (to avoid gauge contamination). +$0.02–0.06/fitting depending on fitting type and thread size.
ASTM A967 Passivation — Standard on All Stainless Pipe Fittings
ASTM A967 passivation — citric or nitric acid — included at no additional charge on every 303, 304, and 316L stainless pipe fitting delivery. Removes free iron from boring and threading operations; restores passive Cr⊂2;O⊂3; oxide at all machined surfaces including all port thread flanks. For multi-port fittings (elbows, tees, crosses), passivation enters each port bore and thread zone — confirming all internal surfaces are passivated, not just the external body surface. Copper sulfate spot test per monthly lot; certificate per lot. Citric acid method for pharmaceutical and food programs; no nitric acid residue in product-contact bore surfaces. Post-passivation 100% all-port gauge re-verification for any stainless fittings where passivation treatment is followed by additional surface operations.
Laser Part Marking — "90"/"45" on Elbow Hex Face (Assortment Programs)
0.3mm deep × 3.5–4mm character height laser marking on elbow hex flat face — the permanent identification that prevents 45° and 90° elbow mix-up in assortment kit packaging and at line-side installation. Applied before nickel plate for permanent marking under the plate surface that cannot be removed or confused during post-plate handling, shipping, or line-side storage. Case study: G1/4 90° and 45° elbows have identical 19mm AF hex and near-identical body OD — without laser marking, visual inspection at incoming or line-side cannot differentiate them; three mix-up incidents at previous Czech supplier cost €28,000 in rework and commissioning delays. Additional assortment markings: "T" on tee bodies; "X" on cross bodies; part number or customer code per assortment kit specification. CMM character depth spot check per 500-piece batch. Laser marking +$0.01–0.03/fitting.
Hot-Dip Galvanize ISO 1461 & Type II Anodize MIL-A-8625
Hot-dip galvanize (45–85μm zinc per ISO 1461) on 4140 and carbon steel pipe fittings for outdoor agricultural, construction equipment, and municipal water utility programs where zinc-nickel electroplate is insufficient for long-term outdoor service life. Post-galvanise 100% all-port gauge (L1 taper ring and plug gauge for NPT/BSPT galvanised fitting ports) confirming every port thread within specification after zinc growth on all internal and external thread flanks. Type II anodize (5–10μm per MIL-A-8625) on 6061-T6 aluminium pipe fitting bodies: all thread ports masked before anodize bath — anodize grows 3–7μm per thread flank on unmasked ports, filling the thread pitch diameter beyond tolerance; 100% post-anodize all-port gauge re-verification mandatory confirming masked ports maintained dimensional integrity. Certificate per lot both treatments.
Surface treatment selection, post-treatment all-port gauge scope for every port of every fitting, PTFE application zone specification for male thread fitting programs, laser marking specification for assortment programs, and pre-plate versus post-plate marking sequence are all included in CNCPioneer's 48-hour DFM review at no additional charge for every brass pipe fitting program.
IATF 16949 Quality System for
Brass Pipe Fittings
CNCPioneer's IATF 16949 certified brass pipe fitting quality system addresses four dimensions specific to multi-port fitting precision: SII XRF material compliance and DZR As mandatory verification, MAZAK C-axis warm-up SOP and inter-port CMM, 100% all-port gauge pre-plate and post-plate, and PPAP Level 3 production qualification with DFM thread form confirmation per fitting installation position.
SII XRF Material Compliance + DZR As 0.02–0.06% Mandatory Per Lot + Thread Form DFM
SII XRF on every incoming brass pipe fitting material lot: C36000 (Cu 60–63%; Pb 2.5–3.7%); DZR CW602N (As 0.02–0.06% MANDATORY per lot — quarantine any lot outside range regardless of mill certificate; As XRF certificate in delivery documentation per lot for WRAS technical file); H59 (Cu 57–60%); 316L (C ≤0.030% mandatory; Mo 2.0–3.0%); 304 (Cr 18–20%); 303 (S 0.15–0.35%); 4140 (Cr 0.80–1.10%; Mo 0.15–0.25%). EN 10204 3.1 material certificate archived per lot. DFM thread form confirmation per fitting type: PPAP case study Finding 1 — six fitting types in the 24-SKU BOM had undifferentiated "BSP" specification; DFM confirmed BSPT R-type (ISO 7-1 tapered, self-sealing) for all inline pipe fittings (elbows, tees, unions) and BSP G-type (ISO 228 parallel, face-seal) for all manifold port closure fittings (plugs, caps at manifold body ports with bonded Dowty seal receptacles). BOM updated before tooling commitment; threading gauge sets confirmed per fitting type: BSPT L1 taper ring/plug gauges for elbow/tee/union; ISO 228 Class A plug/ring gauges for plug/cap at manifold port programs.
- SII XRF per incoming lot all materials — before machining release
- DZR As 0.02–0.06% mandatory per lot — As XRF certificate per delivery lot
- DFM thread form (BSPT vs. G-type) confirmed per fitting installation position from P&ID
MAZAK C-Axis Warm-Up SOP + Inter-Port CMM + 5-Axis Bore Junction Blending
Mandatory 20-minute MAZAK C-axis warm-up cycle before every elbow/tee/cross production session (PPAP case study: C-axis thermal drift without warm-up produced 90° elbow inter-port angle Cpk 0.94 — corrective action: 20-minute warm-up SOP + first-piece inter-port CMM per session — post-corrective Cpk 1.75). First-piece inter-port CMM before production release every session. Inter-port angle CMM per 100-piece production batch: angular position ±0.020° production standard; angle alarm triggers C-axis reference check and recalibration. 45° elbow: approach-from-consistent-direction protocol eliminates C-axis hysteresis at 45° index (PPAP case study: additional corrective action bringing 45° Cpk from 1.58 to 2.22). Union cone seat: CMM per 50-piece batch; PCD insert 100% incoming CMM angle verification per insert at receipt (same corrective action as compression tube fitting case study — PPAP cone angle Cpk 2.08 after 100% insert CMM implemented). 5-axis ball-nose bore junction blending R≥1.5mm: first-article CMM verification of bore junction radius; production process change control for 5-axis program parameters.
- Mandatory 20-minute MAZAK C-axis warm-up SOP before every elbow/tee production session
- First-piece inter-port CMM per session; inter-port angle CMM per 100-piece batch
- PCD insert 100% CMM angle per insert at receipt — union cone seat programs
100% All-Port Gauge Pre-Plate AND Post-Plate + 100% Pressure Test Per Serial Number
100% plug gauge on every female port AND 100% ring gauge on every male port of every fitting before any surface treatment — all fitting types, all programs: BSP G-type ISO 228 Class A plug/ring gauge; BSPT ISO 7-1 L1 taper plug/ring gauge; NPT ASME B1.20.1 L1 taper plug/ring gauge. Primary port confirmed before C-axis secondary port machining investment; each secondary and branch port gauged 100% independently after completion — not as a group. 100% post-plate all-port gauge re-verification after all nickel, chrome, and anodize treatments — every port of every multi-port fitting re-gauged independently. PPAP case study: 720 fittings × 2.1 average ports = 1,512 gauge checks all conforming post-plate. 100% hydrostatic pressure test per sealed fitting body serial number: 1.5× PN rated pressure; 30-second hold; zero pressure decay; records archived minimum 10 years. MSA Gage R&R ≤10% on all ring and plug gauge sets; SPC monitoring per port independently per fitting type; Cpk ≥1.67 all thread pitch diameters for IATF 16949 volume programs.
- 100% plug/ring gauge ALL ports per fitting — all programs, pre-plate
- 100% post-plate ALL-port re-gauge after all nickel, chrome, anodize — mandatory
- 100% hydrostatic pressure test per serial number — all sealed fitting programs
PPAP Level 3 Qualification + Laser Marking Verification + Assortment Kit Packaging
PPAP Level 3 for IATF 16949 automotive and HVAC OEM brass pipe fitting programs: the German HVAC case study 720-fitting pilot (30-piece per fitting type, 24 SKUs) identified and corrected three Cpk failures — 90° elbow inter-port Cpk 0.94 (corrected to 1.75 via warm-up SOP); 45° elbow inter-port Cpk 1.58 (corrected to 2.22 via approach-from-consistent-direction protocol); union cone seat angle Cpk below target (corrected to 2.08 via PCD insert 100% incoming CMM). Post-corrective: all 1,512 gauge checks conforming; all 720 pressure tests passing; PPAP PSW submitted and approved. Volume production at 4,800,000/year: 14 dedicated MAZAK mill-turn centers; monthly kanban 400,000 fittings across 24 SKUs; C36000 bar 3-month safety stock (Jiangxi Copper + Tongling SII XRF per lot); laser marking before nickel plate per SOP; IATF 16949 monthly SPC report all thread pitch diameters per fitting type per port. Assortment kit packaging: sorted by fitting type and size; bagged per type per size in standard counts; labelled per designation; carton-packed per OEM assembly station BOM configuration; counted by calibrated weight scale.
- PPAP Level 3 for IATF 16949 automotive and HVAC OEM programs
- Laser marking character depth CMM per 500-piece batch; applied before nickel plate
- Assortment kit packaging: sorted, labelled, carton-packed per OEM BOM
Brass Pipe Fittings FAQ
Common questions from commercial building services and HVAC equipment OEMs, industrial plumbing and compressed air system distributors, water treatment utility distributors, automotive fluid system Tier 1 suppliers, and process piping manufacturers about CNCPioneer's CNC machined brass pipe fitting capability, fitting type selection, thread standard differentiation, C-axis port angle accuracy, and volume program economics.
C36000 (UNS C36000; CW614N per EN 12164) is the universally recognised reference material for precision CNC machining of brass components — its designation as "100% machinability" derives from its 2.5–3.7% lead content (Pb), which forms a fine network of soft lead particles throughout the copper-zinc matrix that acts as an internal lubricant and chip-breaker during machining. When a CNC boring bar or thread-turning insert contacts C36000 at v_c = 400–600 m/min (the standard production speed), the lead particles at the cutting zone shear into the chip rather than welding to the insert edge — producing short, discrete chips that evacuate cleanly from the bore or thread zone without wrapping around the workpiece or packing in the thread form. The machining consequences: C36000 produces surface finish Ra 0.4–0.8μm from standard TiAlN-carbide inserts at production speeds; thread pitch diameter ±0.005mm from single-point CNC internal thread boring without the tool adhesion and built-up edge that cause pitch diameter scatter in lower-machinability materials; and thread surface Ra ≤0.8μm across both thread flanks — the surface finish that allows NPT and BSPT tapered threads to seal reliably with PTFE tape by providing conformal tape-to-thread-flank contact without the surface discontinuities that rougher threads produce. Against die-cast brass, CNC machined C36000 provides four specific advantages: (1) Porosity-free material density: C36000 bar stock is hot-extruded wrought brass with zero internal voids; die-cast brass contains 0.5–3% void volume from casting shrinkage, producing porosity-path leakage at elevated pressure that die-cast fittings produce at commissioning test. CNCPioneer's 100% individual hydrostatic pressure test per fitting serial number catches porosity leakers in the <0.02% of machined fittings with bar stock inclusion defects; die-cast fitting lot test at 2–5% sample cannot detect the 0.3–0.8% porosity leakers embedded within the lot. (2) Thread form accuracy: die-cast fittings are thread-tapped after casting, producing thread pitch diameter dependent on tap wear across the production session; CNCPioneer's single-point CNC thread boring produces ±0.005mm pitch diameter from programmed NC offset with 100% per-port gauge closure. (3) Dimensional accuracy: die-cast fitting body OD ±0.3–0.8mm from die wear and casting temperature variation; CNCPioneer's CNC turned body OD ±0.050mm. (4) Elbow port angular position: die-cast 90° elbows ±0.5–2.0° from die half alignment; CNCPioneer C-axis ±0.020°. The cost premium of CNC machined over die-cast brass pipe fittings is typically 25–60% per fitting at equivalent size — the investment that prevents the field callback costs, assembly rework, and commissioning test failure rates that die-cast fittings produce in OEM quality programs with documented dimensional and pressure compliance requirements.
The hex bushing and the reducing nipple both achieve brass pipe fitting size reduction in a single fitting body — but they have opposite thread gender configurations that determine which installation scenario each serves. The hex bushing (reducer bushing) has: a LARGE FEMALE internal thread at the hex (large) end — the thread that accepts the incoming pipe or fitting from the larger system; and a SMALL MALE external thread at the plain (small) end — the thread that installs INTO an existing female port. The installation sequence: wrench the hex bushing's small male thread INTO the existing female port of a tee, elbow, cross, or equipment body; the bushing's large female end then accepts the larger incoming connection. The hex bushing IS the port — it transforms the existing port from one size to another. Both the large female end and the small male end are gauged 100% at CNCPioneer (plug gauge large female + ring gauge small male), and the wall thickness at the body minimum section (≥2.0mm confirmed by DFM) is verified before NC program release. The reducing nipple has: a LARGE MALE external thread at one end — the thread that screws INTO a coupling, socket, or female fitting; and a SMALL MALE external thread (both-male configuration) or a SMALL FEMALE internal thread (male-female configuration) at the other end — the thread that connects to the smaller downstream pipe or fitting. The installation sequence: screw the reducing nipple's large male thread into a coupling or female socket on the larger system side; connect the smaller downstream pipe or fitting to the small thread at the nipple's other end. The reducing nipple BRIDGES between two couplings or sockets rather than installing into a port. Practical selection logic: if the size reduction is needed AT an EXISTING FEMALE PORT (a tee branch port, a valve outlet port, a manifold port) and the goal is to make that port accept a smaller incoming connection → specify a hex bushing whose small male end screws into the existing female port. If the size reduction is needed to BRIDGE between two separate female sockets on a distribution header → specify a reducing nipple whose large male end enters the large coupling and whose small thread connects to the smaller circuit. CNCPioneer's DFM for every brass pipe fitting assortment inquiry confirms each BOM item's installation position from the customer's P&ID or layout diagram, identifies hex bushing versus reducing nipple positions independently, and provides the correct gauge specification before production commitment.
The inter-port angular accuracy of a 90° brass pipe elbow — the measured angle between the two port bore axes as produced by the manufacturing process — determines three independent installation outcomes. (1) Pipe routing compliance: for a rigid copper tube run of 400mm attached to a 90° elbow whose port angle deviates from 90° by ±Δθ degrees, the far end of the tube deviates from its designed routing position by 400 × sin(Δθ) mm. At Δθ = ±0.020° (CNCPioneer C-axis): deviation = 400 × sin(0.020°) = ±0.14mm — imperceptible, within ±0.5mm pipe fitting installation tolerance. At Δθ = ±0.5° (typical die-cast elbow from die half alignment tolerance): deviation = 400 × sin(0.5°) = ±3.5mm — visible pipe misalignment requiring a corrective offset or flexible connector at the downstream connection point, adding installation cost. At Δθ = ±1.0° (die-cast elbow at wide tolerance): deviation = 400 × sin(1.0°) = ±7.0mm — forcing the downstream pipe into a strained connection that adds bending stress at both thread engagements. (2) Multi-elbow assembly accumulation: in a HVAC chiller water circuit with 38 elbows in series, the angular deviation accumulates as a random walk: total assembly deviation = Δθ × √38 × pipe_section_length. At ±0.020° CNCPioneer: total = 0.020 × √38 × 300 = ±37mm across the full circuit — within the ±50mm chiller manifold connection tolerance. At ±0.5° die-cast: total = 0.5 × √38 × 300 = ±924mm — far exceeding any manifold connection tolerance, requiring field-cut pipe and offset fittings throughout. (3) Pneumatic manifold port co-planarity: for manifold assemblies where multiple elbows' faces must be co-planar (a bank of instrument connections all facing the same accessible side), the elbow's inter-port angular deviation directly measures the deviation of the second port's face from the required co-planar orientation. The C-axis achieves ±0.020° through three mechanical disciplines: the C-axis absolute encoder (resolution <0.001°) records rotational position without accumulated error from revolution counting; the approach-from-consistent-direction protocol (always approaching the 90.000° target from the sub-90° direction) eliminates hysteresis from the C-axis drive mechanism's mechanical compliance; and the mandatory 20-minute warm-up cycle allows the MAZAK mill-turn's thermal expansion to reach steady-state before the C-axis reference position is established — eliminating the 0.008–0.015° thermal drift that produced the Cpk <1.67 at production start that the PPAP case study identified and corrected. Die-cast elbow angular accuracy ±0.5–2.0° derives from the die parting line which separates the two die halves forming the elbow body — die half alignment tolerance ±0.1–0.4mm at 850°C casting temperature produces the inter-port angular deviation that is inherent to the die-cast process and cannot be improved without die investment that makes die-casting economically non-competitive.
Prototype lead times: C36000 G1/2 BSP 90° elbow (C-axis ±0.020°; 100% dual plug gauge; R1.5mm bore junction; nickel; 50-piece) — 3–4 business days; C36000 G1/2 BSP equal tee (C-axis 90° branch; 100% triple plug gauge; nickel; 25-piece) — 3–4 days; DZR G3/4 BSP 90° elbow (As XRF; 100% dual plug gauge; nickel; WRAS documentation; 25-piece) — 4–5 days; C36000 G1/2 BSP ground joint union (cone seat ±0.25°; 100% all-port gauge; pressure test assembled; nickel; 25-piece) — 4–6 days; C36000 G3/4 × G1/2 BSP hex bushing (100% both-port gauge; nickel; 50-piece) — 2–3 days; C36000 G1/2 BSP hex head plug (100% ring gauge; PTFE; nickel; 100-piece) — 1–2 days; custom ODM elbow (compound angle from P&ID; 3D CAD 48h; prototype 5-piece FAIR) — 7–10 days total from enquiry. Volume economics: C36000 G1/2 BSP 90° elbow at 25,000–100,000/year $0.46–0.68; at 2M–10M/year $0.14–0.21; at 10M+/year $0.095–0.14. DZR G3/4 BSP 90° elbow at 25,000–100,000/year $0.57–0.85; at 2M+/year $0.18–0.26. C36000 G1/2 equal tee at 25,000–100,000/year $0.55–0.82; at 2M–10M/year $0.17–0.25. Ground joint union G1/2 at 25,000–100,000/year $1.68–2.50; at 500,000+/year $0.76–1.13. Four-tier market comparison for C36000 G1/2 BSP 90° elbow (C-axis ±0.020° inter-port angle; 100% all-port plug gauge; 100% post-plate all-port re-gauge; bright nickel 10μm; 5-axis R1.5mm bore junction blending; laser angle marking; 100% pressure test; IATF 16949 PPAP Level 3) at 4,800,000/year: European brass fitting specialist (German, Czech, Italian IATF 16949 CNC facility): €0.40–0.60/fitting; Taiwanese precision brass fitting machining (ISO 9001): $0.28–0.40/fitting; CNCPioneer China (IATF 16949; C36000 SII XRF per lot; MAZAK C-axis ±0.020°; 5-axis bore junction R1.5mm; laser angle marking; 100% all-port gauge pre-plate + post-plate; 100% pressure test; PPAP Level 3): €0.23/fitting — case study validated at 4,800,000/year; annual saving €1,056,000 versus previous Czech CNC supplier at €0.45/fitting; lowest-cost Asian die-cast brass fitting (no C-axis; ±0.5–2.0° elbow angle; porosity risk; 2–5% sample pressure test; no PPAP): $0.09–0.14/fitting. The CNCPioneer premium over lowest-cost die-cast: $0.08–0.12/fitting (57–86% above lowest-cost) delivers: porosity-free machined-from-bar construction (eliminating 0.3–0.8% commissioning pressure test failures); C-axis ±0.020° elbow angle (versus die-cast ±0.5–2.0° requiring field offset corrections); 5-axis bore junction R1.5mm (15.6% chiller pump energy saving quantified in case study); laser angle marking (preventing €28,000/incident assembly cross-angle fault); 100% all-port gauge pre-plate and post-plate (catching 24,000 non-conforming secondary-port fittings/year that 5% sample gauging misses at 4,800,000/year); IATF 16949 PPAP Level 3 (required for Tier 1 automotive and HVAC OEM qualification). The case study validated the largest single-program annual saving in this catalog: €1,056,000 from a 24-part-number HVAC OEM assortment program that replaced European CNC supply with CNCPioneer China supply at IATF 16949 quality equivalence and the additional quality improvements (bore junction radius, laser marking, DFM thread form correction) that the European supplier had not identified or implemented.
Get a Quote for Customized Brass Pipe Fittings
Upload your brass pipe fitting drawings, 3D CAD models (STEP, IGES), P&ID system schematic, fitting type list (elbows, tees, crosses, unions, bushings, plugs, caps, street fittings, adapters, or custom ODM), thread standard specification (BSPT R-type ISO 7-1 for self-sealing inline joints / BSP G-type ISO 228 for face-seal port connections / NPT ASME B1.20.1 / DIN / JIS / metric — with sealing method per fitting installation position confirmed by DFM before tooling assignment), material requirement (C36000 / DZR CW602N WRAS / H59 / 316L stainless / 4140 QT / 6061-T6 aluminium), surface treatment (bright nickel / chrome / PTFE pre-applied / passivation / laser marking / galvanize), quantity per type, annual volume, or complete fitting assortment BOM and receive a competitive quotation within 24 hours and complete engineering DFM within 48 hours — covering fitting type and configuration confirmation from your installation P&ID and layout diagram (hex bushing vs. reducing nipple; BSPT vs. G-type per fitting installation position with functional consequences of incorrect form selection explained before production commitment); material selection from your service fluid, regulatory environment, and corrosion requirement (C36000 vs. DZR CW602N vs. 316L from WRAS potable water, food contact, pharmaceutical, marine, or industrial service with per-fitting cost comparison); C-axis port angular position achievability from MAZAK mill-turn (±0.020° confirmed before tooling assignment); 5-axis bore junction radius blending feasibility and pressure loss coefficient improvement calculation for your specific flow application; union cone seat angle and Ra achievability for metal-to-metal ground joint sealing; all-port 100% gauge scope confirming all ports gauged 100% per fitting type; laser angle marking specification for elbow types and assortment type identification programs; DZR As XRF scope and WRAS documentation package for complete UK/EU potable water fitting assortment programs; PPAP Level 3 scope for IATF 16949 automotive and HVAC OEM assortment programs; ODM custom fitting design from P&ID or layout sketch to production-ready 3D CAD within 48–72 hours; assortment kit packaging per customer BOM; and complete per-fitting pricing from prototype customized brass pipe fitting first articles through IATF 16949 governed production and wholesale assortment supply.