Hydraulic Cylinder
Piston Machining
CNCPioneer is a precision hydraulic piston parts manufacturer and certified China hydraulic piston parts specialist delivering cylinder piston machining programs — custom hydraulic piston parts in 4140 alloy steel, 17-4PH stainless steel, aluminum, brass, and bronze; precision piston machining for single-acting and double-acting cylinders; multi-groove seal pocket machining for O-ring, U-cup, T-seal, and piston ring seal configurations; hard chrome OD surface programs; and complete custom hydraulic piston parts packages.
What Is Hydraulic Cylinder
Piston Machining?
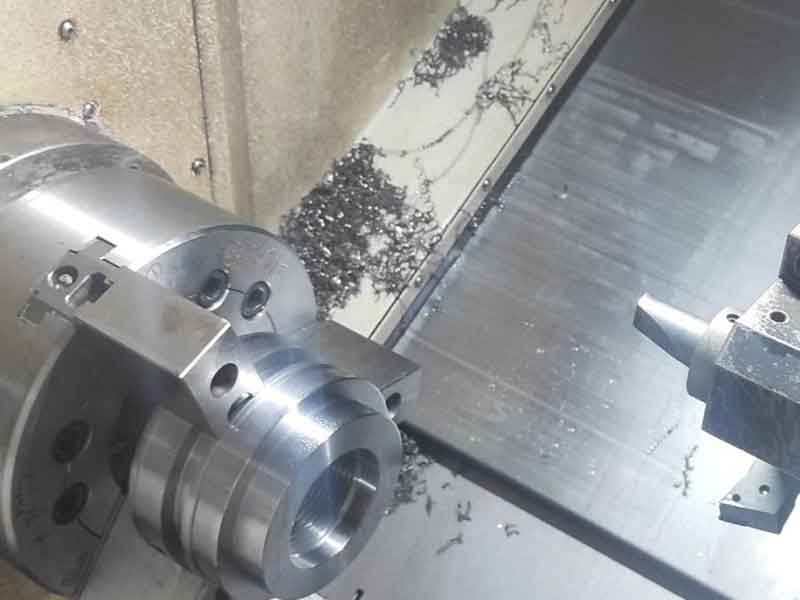
The hydraulic piston is the primary moving element inside a hydraulic cylinder barrel — the precision-machined disc or spool that slides within the cylinder bore, converts hydraulic fluid pressure into linear mechanical force, and maintains the sealed pressure boundary between the high-pressure and low-pressure sides of the cylinder through precision-machined seal grooves that retain the piston seals. Every hydraulic cylinder — regardless of type, size, or application — depends on the dimensional accuracy of its piston for the pressure containment, force output, bearing stability, and service life the hydraulic system was designed to deliver.
Cylinder piston machining encompasses three distinct precision requirements that together determine whether an assembled cylinder functions to specification. First, OD diameter accuracy: the piston OD must fit the cylinder barrel bore within a defined running clearance — typically 0.050–0.100mm for standard hydraulic cylinders with piston seals, or 0.005–0.020mm for close-clearance pistons in servo hydraulic and precision motion applications. Diameter error outside the clearance specification causes seal over-compression (OD too large) or seal extrusion under pressure (OD too small), both of which produce leakage within the first operating cycles. Second, seal groove geometry: the circumferential grooves machined into the piston OD that receive and retain the piston seals are dimensionally the most critical features on the piston body — groove width ±0.020mm governs whether the seal fits correctly in the groove, groove depth ±0.020mm governs the seal compression ratio, and groove corner radii govern whether the seal lip is cut during installation. Third, OD surface finish: Ra 0.2–0.4μm on the piston OD is the finish specification for seal contact surfaces — the finish at which dynamic piston seals develop the thin lubrication film that prevents seal dry-running while maintaining the seal's designed leak-down rate between inspections.
-
Single-setup MAZAK mill-turn concentricity guarantee CNCPioneer's precision piston machining programs integrate all three requirements in single-setup MAZAK mill-turn programs — OD turning, seal groove machining, and all related features completed from one datum in one chucking, ensuring that groove positions are concentric to the piston OD axis within ±0.010mm and that the machined OD surface finish is uniform across the complete seal contact length without the surface discontinuities produced by tool changes between setups.
-
Seal groove geometry as the primary precision discipline The seal groove is the most functionally critical feature on every hydraulic piston and the most common source of in-field hydraulic cylinder leakage attributable to machining quality. CNCPioneer's sealing groove machining programs apply dedicated groove tooling with ground-form profile controlling groove width ±0.020mm and groove floor radius simultaneously; in-process air gauge measurement of groove width and depth at every groove; and groove concentricity verification by CMM confirming all grooves are co-axial with piston OD within ±0.010mm.
-
Ra 0.2–0.4μm OD surface finish directly from CNC turning The piston OD seal contact surface requires Ra 0.2–0.4μm finish — smooth enough that dynamic piston seals develop a lubrication film without excessive oil film thickness that would allow controlled leakage. CNCPioneer achieves this finish directly from precision CNC turning using CBN or polycrystalline diamond (PCD) inserts at optimized cutting parameters, eliminating the external cylindrical grinding step that most hydraulic piston parts manufacturers require as a separate operation for this surface.
-
40–60% China hydraulic piston parts cost advantage 40–60% below equivalent precision piston machining from US, European, and Japanese hydraulic component machining facilities at identical dimensional accuracy and IATF 16949 documentation. Engineering DFM review, seal groove dimension pre-loading from ISO/JIS/DIN catalogs, and coating allowance planning are included in CNCPioneer's program pricing — decisive economics for hydraulic cylinder OEMs whose per-unit piston cost determines product competitiveness in global hydraulic equipment markets.

Why CNCPioneer — Hydraulic
Piston Parts Manufacturer
Among hydraulic piston parts manufacturers globally, CNCPioneer's seal groove geometry discipline, single-setup OD + groove concentricity foundation, Ra 0.2–0.4μm direct-from-turning surface finish, complete material portfolio, 24-hour DFM capability, and China cost advantage establish our factory as the preferred hydraulic piston parts manufacturer across the full hydraulic cylinder supply chain.
Seal Groove Geometry as the Primary Quality Discipline
The seal groove is the most functionally critical feature on every hydraulic piston and the most common source of in-field hydraulic cylinder leakage attributable to machining quality. CNCPioneer's sealing groove machining programs apply: dedicated groove tooling with ground-form profile controlling groove width ±0.020mm and groove floor radius simultaneously; in-process air gauge measurement of groove width and depth at every groove; and groove concentricity verification by CMM confirming all grooves are co-axial with piston OD within ±0.010mm. The combination eliminates the groove dimensional errors that produce premature seal failure in service.
Single-Setup OD + Groove Program as the Concentricity Foundation
Rechucking a piston between OD turning and groove machining introduces ±0.010–0.030mm concentricity error between OD and groove positions — error that appears as groove depth variation around the circumference. CNCPioneer's MAZAK mill-turn programs machine piston OD and all seal grooves in one chucking, holding groove-to-OD concentricity at ±0.005mm by machine positioning rather than chuck re-registration — a structural guarantee that extends through volume production without degradation.
Ra 0.2–0.4μm OD Surface Finish Directly from CNC Turning
The piston OD seal contact surface requires Ra 0.2–0.4μm finish — smooth enough that dynamic piston seals develop a lubrication film without excessive oil film thickness. CNCPioneer achieves this finish directly from precision CNC turning using CBN or polycrystalline diamond (PCD) inserts at optimized cutting parameters, eliminating the external cylindrical grinding step that most hydraulic piston parts manufacturers require as a separate operation — reducing lead time and cost while avoiding grinding setup errors.
Complete Material Portfolio for All Hydraulic Piston Applications
4140 alloy steel for high-pressure industrial and mobile hydraulic pistons; 17-4PH H900 stainless for corrosion-resistant pistons in marine, chemical, and food processing hydraulic systems; aluminum 6061-T6 for lightweight mobile and aerospace hydraulic pistons; brass C36000 for non-sparking and non-magnetic piston programs; and bronze C93200 for self-lubricating pistons in applications with limited seal lubrication — all from one China hydraulic piston parts manufacturer under one IATF 16949 quality system.
Custom Hydraulic Piston Parts DFM in 24 Hours
Every custom hydraulic piston inquiry receives engineering DFM covering: seal groove dimensions from the customer's specified seal catalog number (ISO 5597, JIS B8354, DIN 24336 seal groove dimensions pre-loaded in CNCPioneer's design library); OD running clearance from barrel bore specification; surface finish achievability; material recommendation per operating pressure and environment; chrome or anodize allowance in machined OD dimensions; and volume production cost optimization. This fluency elevates DFM from generic machinability comment to hydraulic cylinder design value.
Hydraulic Piston Parts China Cost Advantage
CNCPioneer delivers precision piston machining at 40–60% below US, European, and Japanese hydraulic component machining facilities at identical dimensional accuracy and IATF 16949 documentation. Single-setup completeness eliminates secondary operation subcontractor costs — pistons exit CNCPioneer complete. Engineering DFM, seal groove standard pre-loading, PPAP documentation, and coating allowance planning are all included in program pricing without surcharges. For a hydraulic cylinder OEM producing 10,000 cylinders annually, China hydraulic piston parts savings of $35–60 per piston produce $350,000–$600,000 annual BOM cost reduction.
Hydraulic Piston Types —
Complete Portfolio
CNCPioneer's custom hydraulic piston parts programs cover the complete hydraulic piston architecture — from standard single-piece pistons for industrial cylinders through stepped multi-diameter pistons, composite piston assemblies with wear rings, lightweight aluminum pistons, marine-grade stainless pistons, and self-lubricating bronze pistons for every pressure class and operating environment.

Standard Single-Piece Hydraulic Pistons
The most common hydraulic piston configuration — one-piece machined body with all seal grooves and connection features. OD range: Ø20mm–Ø500mm standard (above Ø500mm: special program). Length: up to 5× OD in single turning operation; longer pistons in multi-chuck programs. Seal groove count: 1–6 grooves per piston depending on pressure class and seal configuration. Material: 4140 steel (default); 17-4PH stainless; aluminum 6061-T6; brass C36000. Rod connection: internal thread, through-bore for nut, or flanged face with bolt circle. Standard programs available: ISO 6020/1 (metric medium pressure), ISO 6020/2 (medium pressure compact), ISO 6022 (high pressure), NFPA T3.6 (inch dimensions).

Stepped and Multi-Diameter Pistons
Pistons with different OD zones for differential-area applications or multi-stage pressure designs. Step transition: ±0.020mm step position; transition radius ±0.050mm for stress concentration control. Each diameter zone: independent OD tolerance ±0.005mm and seal groove network. 5-axis mill-turn for complex step geometries. Common in regenerative cylinder circuits, telescopic cylinder stages, and differential-area actuators where the same piston body must seal at two different bore diameters within one cylinder assembly.

Composite Piston Assemblies
Pistons assembled from a machined steel body with separate PTFE or bronze wear rings pressed into external ring grooves — common in high-load, high-speed cylinder applications. Wear ring groove: ±0.005mm for controlled interference fit of ring in groove. Wear ring OD (finished assembly): ±0.010mm for barrel bore running fit. Material pairing: 4140 steel body + cast bronze or filled PTFE wear rings. Composite assemblies extend piston service life in abrasive environments and high-cycle automation applications where direct steel-to-bore contact would accelerate barrel wear.

Lightweight Aluminum Pistons
For mobile hydraulics, aerospace actuators, and weight-critical hydraulic systems. Material: 6061-T6 aluminum (yield 276 MPa; 1/3 density of steel). Pressure limitation: aluminum pistons rated to 200 bar without reinforcement; 350 bar with steel thread insert in rod connection bore. Anodize: Type III hard anodize on OD seal contact surface — HV 400+ wear resistance compensating aluminum's lower hardness versus steel barrel bore; anodize growth allowance incorporated in machined OD dimensions. Mass: verified ±2g for balanced piston-in-cylinder inertia.

Marine and Chemical Service Pistons (17-4PH Stainless)
For hydraulic cylinders exposed to seawater, chemical splash, food processing wash-down, or other corrosive service environments. Material: 17-4PH H900 stainless — 1,310 MPa yield; HRC 44–47; corrosion resistance. Pressure rating: to 700 bar (among the highest achievable in precision piston machining). Passivation: ASTM A967 mandatory post-machining. Surface finish: Ra 0.2μm on OD seal contact; electropolish option for biological purity applications. The practical optimum for corrosion-resistant hydraulic pistons where chrome plating is unacceptable for food safety or marine immersion.

Bronze Self-Lubricating Pistons (C93200 Bronze)
For hydraulic cylinders in applications with limited seal lubrication, low-speed high-load, or where elastomeric seals are replaced by metal ring designs. Material: C93200 bronze (SAE 660) — self-lubricating from embedded graphite reservoirs in porous bronze structure. Application: hydraulic/pneumatic cylinders in dust-laden environments; cylinders requiring service-free maintenance intervals. OD surface: Ra 0.4μm for maximum bronze-to-barrel bore contact area at low lubrication level. Sacrificial wear on piston protects barrel bore — extending cylinder service life in abrasive operating conditions.
Industries & Applications
CNCPioneer's hydraulic piston parts manufacturer capability serves every industry consuming precision piston machining at documented dimensional accuracy — from hydraulic cylinder manufacturers coordinating complete per-cylinder piston kit programs to marine hydraulic system builders requiring 17-4PH stainless pistons with ASTM A967 passivation.
Hydraulic Cylinder Manufacturers
Complete custom hydraulic piston parts portfolios — standard single-piece, stepped, and composite piston assemblies in 4140 steel, 17-4PH stainless, aluminum, brass, and bronze with prototype-to-volume manufacturing continuity. Complete piston kits per cylinder build slot delivered synchronized to assembly schedules. Volume programs at 500,000+ annual units with PPAP Level 3 documentation, 100% groove dimensional verification, and blanket order monthly delivery.
Mobile Equipment OEMs
Precision hydraulic piston parts for excavator, loader, and agricultural machinery hydraulic cylinders — 4140 steel pistons with hard chrome OD plating for barrel bore wear resistance; aluminum 6061-T6 pistons for weight-critical boom and arm actuators; and composite piston assemblies with bronze wear rings for high-cycle construction equipment operating in abrasive environments. Supply chain programs at 100,000+ annual unit volumes.
Industrial Automation Builders
Close-clearance servo hydraulic pistons at ±0.005mm OD tolerance for precision motion cylinders in press, forming, and material handling automation. Seal groove machining for compact seal and T-seal configurations at ±0.020mm groove width and depth. Hard chrome OD surface programs for long-cycle press cylinder pistons. Preload spacer matched sets for angular contact bearing pairs in precision actuator output shafts.
Agricultural Machinery Producers
Hydraulic piston parts for tractor lift cylinders, harvester header actuators, and sprayer boom cylinders — 4140 steel standard pistons with hard chrome plating for corrosion resistance in field environments; bronze C93200 self-lubricating pistons for cylinders in dusty agricultural conditions where conventional elastomeric seals fail. Volume production at 50,000+ annual units with dedicated MAZAK mill-turn capacity.
Construction Equipment Companies
High-pressure hydraulic piston parts for crane, piling, and tunneling equipment cylinders — 4140 steel pistons rated to 350 bar; 42CrMo4 through-hardened pistons for maximum torque capacity; and composite piston assemblies with PTFE wear rings for high-load, high-speed cylinder applications. Induction-hardened OD surface options for maximum wear resistance with tough core. PPAP Level 3 for OEM hydraulic cylinder supply chains.
Marine Hydraulic System Manufacturers
17-4PH H900 stainless steel hydraulic pistons for marine winch, steering, and deck machinery cylinders exposed to seawater and salt spray — corrosion resistance equivalent to 304 stainless without chrome plating. Passivation ASTM A967 mandatory post-machining. Pressure rating to 700 bar for deep-sea hydraulic systems. Electropolish option for biological purity in food processing and pharmaceutical hydraulic applications.
Hydraulic Piston Machining
Process & Capabilities
CNCPioneer's precision piston machining process runs on 66+ MAZAK Integrex and Quick Turn mill-turn machining centers — thermal-stabilized spindles maintaining ±0.005mm diameter compliance across multi-hour production runs, sub-spindle transfer for single-setup completeness, and live tooling for milling, drilling, and threading operations within the same turning setup.
24-Hour Hydraulic Piston DFM & Engineering Review
Single-setup concentricity feasibility for every piston · Seal groove standard identification and groove dimension pre-loading from ISO 5597, JIS B8354, DIN 24336, Parker, Trelleborg, SKF, and Freudenberg seal groove standards · OD running clearance from barrel bore specification · Surface finish achievability for O-ring, U-cup, T-seal, compact seal, and piston ring seal configurations · Material selection for pressure, temperature, and fluid compatibility · Chrome or anodize allowance in machined OD dimensions · Volume production cost optimization specific to hydraulic piston geometry.
Single-Setup Piston OD + Groove Machining
Standard piston sequence on MAZAK sub-spindle platforms: face left end; center drill for tailstock support → OD rough turn to +0.3mm stock → bore center bore or internal thread rough → thermal stabilization pause → OD finish turn to ±0.010mm diameter (prepare for groove machining reference) → all seal grooves in sequence: one groove tool, single plunge per groove (±0.020mm width and depth) → in-process groove measurement between groove passes → OD finish pass with CBN or PCD insert at final diameter ±0.005mm; Ra 0.2–0.4μm → internal thread finish tap or bore → part-off / sub-spindle right face machining for rod connection features. All groove relationships governed by machine positioning accuracy rather than rechucking uncertainty.
Sealing Groove Machining — Dedicated Process
Groove tool selection: ground-form groove insert matched to target groove geometry; insert profile verified on optical comparator before piston batch. Piston OD finish turning in same setup: OD turned to final diameter ±0.005mm as reference datum for all groove positions. Groove plunge sequence: each groove machined in single plunge-and-feed cycle — entry chamfer → groove plunge to depth ±0.020mm → groove floor traverse to width ±0.020mm → exit chamfer. In-process groove width measurement: telescoping gauge at 3 angular positions per groove after machining. CMM groove network verification: all groove center positions measured relative to OD datum; concentricity ±0.010mm per groove.
In-Process Control & Final Inspection
First-off laser micrometer and air gauge verification before batch release · Adaptive offset correction for tool-wear diameter drift maintaining ±0.005mm compliance without operator intervention · Roundness measurement after finish-turning on all seal contact OD surfaces · SPC Cpk ≥1.33 (≥1.67 IATF special characteristics) on all OD and groove dimensions · 100% groove width telescoping gauge at 3 positions per groove per piston during production · Groove depth depth micrometer per groove per piston · In-process OD air gauge before and after groove machining · Thermal stabilization protocol documented for all aluminum piston programs.
Hydraulic Piston Parts Materials
4140 alloy steel (normalized; quench + temper to HRC 28–34; induction-hardened OD HRC 54–60) · 17-4PH H900 stainless (1,310 MPa yield; HRC 44–47; corrosion resistance to 700 bar) · Aluminum 6061-T6 (yield 276 MPa; Type III hard anodize OD; to 350 bar with steel thread inserts) · Brass C36000 (free-machining; non-sparking ATEX; non-magnetic) · Bronze C93200 (self-lubricating; sacrificial wear; dust-laden environments) — all XRF-verified per lot. SII XRF composition confirmation on every material lot before turning operations begin.
IATF 16949 / AS9100D Documentation
Certificate of Conformance · Laser micrometer OD diameter records (per journal, per lot) · Air gauge bore diameter records · Groove width and depth records per groove per piston · CMM dimensional report (concentricity, perpendicularity, shoulder positions, groove positions) · Profilometer OD seal contact surface Ra records · Thread gauge records · Material certifications with heat lot traceability · Heat treatment hardness certificates · Plating/coating certifications with post-treatment dimensional verification · PPAP Level 3 for volume hydraulic piston parts programs · FAIR per AS9102 for aerospace/defense · All records retained 20 years.
Materials for Hydraulic
Piston Parts
Hydraulic piston parts material selection is governed by yield strength at operating pressure, hardness requirement for barrel bore running, corrosion resistance for operating environment, mass sensitivity for mobile and aerospace systems, and machinability for seal groove precision. 4140 alloy steel dominates as the default hydraulic piston material for industrial and mobile applications.
Steel 4140 Alloy Steel
Composition: Cr 0.80–1.10%; Mo 0.15–0.25%; C 0.38–0.43% · Yield strength: 655 MPa (normalized); 900–1,000 MPa (quench + temper to HRC 28–34) · Machinability: 65% of free-machining 1212 · The most widely specified material for hydraulic piston machining — providing the combination of strength, machinability, and case-hardenability that most industrial and mobile hydraulic piston applications require. Surface hardness options: through-hardened HRC 28–34 for service wear resistance; induction-hardened OD surface HRC 54–60 for maximum wear resistance with tough core. Hard chrome plating: standard substrate for hard chrome OD plating (0.025–0.050mm chrome).
Steel 17-4PH H900 Stainless
Composition: Cr 15.0–17.5%; Ni 3.0–5.0%; Cu 3.0–5.0%; Nb 0.15–0.45% · Yield strength: 1,310 MPa (H900 precipitation hardened condition) · Hardness: HRC 44–47 — provides adequate OD wear resistance for steel barrel bore running without chrome plating · Corrosion resistance: equivalent to 304 stainless in marine and mild chemical environments · Machined in solution-annealed condition, then precipitation hardened to H900 — minimizing distortion of precision groove dimensions during aging treatment. Post-aging dimensional change: ±0.003–0.008mm on piston OD — machined slightly undersize accounting for predictable aging growth.
Stainless 303
Composition: Cu 60–63%; Zn 35.5–38%; Pb 2.5–3.7% (free-machining leaded brass) · Machinability: 100% of free-machining 1212 steel — the most machinable engineering alloy; complex groove geometries and tight tolerances achievable at minimum cycle time · Non-sparking: brass pistons certified for ATEX Zone 1 and Zone 2 explosive atmosphere hydraulic actuators · Non-magnetic: brass is diamagnetic — correct for pistons in MRI and precision magnetic measurement environments · Corrosion resistance: good in hydraulic oil, water-glycol, and HFA hydraulic fluids; inadequate for seawater immersion without further protection.
Aluminum 6061-T6
Yield strength: 276 MPa — adequate for hydraulic pistons to 200 bar in standard designs; 350 bar with steel thread inserts at rod connection · Density: 2.70 g/cm³ (35% of 4140 steel) — aluminum piston 35% of equivalent steel piston mass · Thermal expansion management: CTE 23.6 ppm/°C versus steel 11.7 ppm/°C — running clearance between aluminum piston and steel barrel changes 5–8μm per 10°C temperature change; CNCPioneer's aluminum piston programs incorporate this differential in OD tolerance targeting · Type III hard anodize: mandatory OD surface treatment for aluminum pistons in steel barrel bores — anodize provides HV 400+ surface hardness protecting soft aluminum from barrel bore contact wear.
Bronze C93200 (SAE 660)
Composition: Cu 81–85%; Sn 6.3–7.5%; Pb 6.0–8.0%; Zn 2.0–4.0% · Self-lubrication: lead phase in bronze microstructure provides boundary lubrication at piston-to-barrel contact surfaces when oil film is absent or marginal · Hardness: HB 60–90 (softer than steel barrel — sacrificial wear on piston protects barrel bore) · Application: vertical hydraulic cylinders with minimal seal lubrication; cylinders in dusty and abrasive environments where elastomeric seals fail but metal-to-metal running is acceptable · OD surface: Ra 0.4μm for maximum bronze-to-barrel bore contact area at low lubrication level.
Brass C36000
Free-machining brass for hydraulic pistons in non-sparking (ATEX), non-magnetic, or instrument-quality applications · Machinability: 100% of free-machining 1212 steel — the most machinable engineering alloy; complex groove geometries and tight tolerances achievable at minimum cycle time · Non-sparking: brass pistons certified for ATEX Zone 1 and Zone 2 explosive atmosphere hydraulic actuators · Non-magnetic: brass is diamagnetic — correct for pistons in MRI and precision magnetic measurement environments · Corrosion resistance: good in hydraulic oil, water-glycol, and HFA hydraulic fluids; inadequate for seawater immersion without further protection.
Surface Treatments for
Hydraulic Piston Parts
Hydraulic piston parts surface treatment selection addresses wear resistance at barrel bore running interfaces (hard chrome, nitriding), corrosion resistance in chemical and marine environments (electroless nickel, passivation), wear protection for aluminum pistons (Type III hard anodize), and mild corrosion protection for storage and shipping (black oxide) — coating allowances are machined-in and verified post-treatment.
Hard Chrome Plating — ASTM B177
The standard OD surface treatment for 4140 steel hydraulic pistons — chromium electrodeposit 0.025–0.075mm thickness providing: OD hardness HV 800–1,000 (HRC 65–72) for barrel bore wear resistance; surface finish Ra 0.05–0.2μm from chrome-plated and ground/superfinished surface — below the Ra 0.4μm of unplated CNC-turned surfaces; corrosion resistance in hydraulic oil and water-glycol fluid environments. Piston OD machined undersize by chrome thickness allowance ±0.010mm; post-chrome OD verified to ±0.005mm of target by 100% measurement. CNCPioneer coordinates the chrome deposition + post-plate grind sequence as a complete program deliverable.
Electroless Nickel — MIL-C-26074
Uniform corrosion protection for hydraulic pistons in chemical, food processing, and offshore hydraulic systems where hard chrome corrosion resistance is insufficient. Hardness: HV 500 (as-deposited); HV 900+ (heat-treated to 400°C) — adequate for moderate wear. Coating uniformity: ±0.003mm across complex groove geometry — no masking required at grooves. Dimensional allowance: ±0.008mm per side; piston OD machined accordingly. Post-plate air gauge verification on all journal diameters confirms bearing interference class compliance before lot release. Critical for piston seal-contact zones: electroless nickel's smooth deposition surface reduces running-in wear against lip seals.
Type III Hard Anodize — MIL-A-8625 (Aluminum Pistons)
Mandatory wear protection for aluminum hydraulic piston OD surfaces running in steel or aluminum barrel bores. Hardness: HV 400+ for aluminum 6061-T6; HV 300+ for 7075-T6 at standard parameters. Thickness: 0.025–0.050mm per side; OD machined with anodize growth allowance. Seal groove masking: grooves must be masked during anodize to prevent anodize dimensional growth within groove — anodize in grooves would reduce groove width below seal specification. Post-anodize bore air gauge confirms final bore within H6/H7 specification. Type III anodize on aluminum pistons provides wear resistance at housing-to-outer-race interface without the mass penalty of steel pistons.
Passivation — ASTM A967 (Stainless Pistons)
Mandatory for all 17-4PH and 316L stainless hydraulic pistons — restores passive oxide layer at all machined surfaces. Zero dimensional change. Standard mandatory treatment for all 17-4PH, 303, and 316L stainless hydraulic piston parts — removes machining free iron, enhances the passive chromium oxide layer for maximum corrosion resistance across hydraulic cylinder service life, and applies zero dimensional change (passivation adds no measurable dimension). Applied after all machining is complete on pistons, including cross-holes, grooves, threads, and bores machined in the MAZAK single-setup program; passivation liquid penetrates all internal features uniformly. Passivation certificates included in standard shipment documentation.
Black Oxide — Mild Corrosion Protection
Mild corrosion protection for short-term storage and shipping; removed by hydraulic oil on first filling cycle. Dimensional change ≤0.0002mm — no dimensional allowance required. Low-reflectance finish for hydraulic pistons in instrument-quality applications where bright steel surfaces create undesirable optical effects. Applied in conjunction with passivation on stainless piston programs requiring both low reflectance and corrosion resistance. Cost-effective alternative to electroless nickel for low-load indoor hydraulic cylinder hardware where corrosion resistance is secondary to storage protection and optical suppression.
Nitriding — Case-Hardened Surface Without Distortion Risk
Ion or gas nitriding (HRC 58–62 surface, 0.1–0.3mm case depth) for hydraulic pistons requiring enhanced surface fatigue resistance without the distortion risk of through-hardening — achievable on 4140 and 17-4PH pistons already finish-turned to near-final dimensions, with post-nitriding journal finish-grinding restoring ±0.005mm journal accuracy. Nitriding's shallow case depth and low process temperature (480–550°C) minimize dimensional distortion versus through hardening (800–900°C quench), making nitriding the fatigue-enhancement treatment of choice for pistons whose seal groove concentricity cannot absorb the ±0.010–0.030mm distortion typical of through hardening. CNCPioneer coordinates pre-nitriding machining, nitriding vendor, and post-nitriding grinding as a complete program deliverable.
All surface treatments on hydraulic piston parts programs — hard chrome ASTM B177, electroless nickel MIL-C-26074, Type III hard anodize MIL-A-8625, passivation ASTM A967, black oxide, and nitriding — are documented with treatment certifications and post-treatment dimensional verification in the shipment package. Plating and coating allowances are machined-in to journal and bore dimensions at the CNC turning stage and confirmed post-treatment by air gauge or laser micrometer — ensuring dimensional specifications are met in the final delivered condition. Treatment selection guidance and dimensional allowance calculation are included in CNCPioneer's 24-hour DFM review at no additional cost.
Quality Assurance for
Hydraulic Piston Parts
Hydraulic piston parts quality assurance addresses seal groove geometry with in-process air gauge verification, OD diameter with laser micrometer resolution, groove-to-OD concentricity with CMM measurement, and surface finish with profilometry — combined with SPC control charts and PPAP Level 3 documentation for volume hydraulic cylinder OEM supply chains.
Engineering Contract Review & DFM
24-hour DFM review covering: seal groove standard identification and groove dimension pre-loading from ISO/JIS/DIN catalog; OD running clearance from barrel bore specification; surface finish achievability for O-ring, U-cup, T-seal, compact seal, and piston ring seal configurations; material selection for pressure, temperature, and fluid compatibility; chrome or anodize allowance in machined OD dimensions; and volume production cost optimization. All drawing ambiguities resolved before machining — non-conforming pistons scrap expensive materials and lose lead time that prototype schedules cannot recover.
Material Verification
SII XRF composition confirmation on every hydraulic piston parts material lot — 4140, 17-4PH, 6061-T6, C36000, and C93200 confirmed before turning operations begin. Hardness verification post-aging (17-4PH H900: HRC 44–47) and post-heat-treatment (4140: HRC 28–34) — per lot before final groove machining. Bar stock OD and straightness incoming check before MAZAK loading. Full mill-certificate-to-shipment lot traceability on all hydraulic pistons.
In-Process Piston Machining Control
First-off laser micrometer OD and air gauge groove verification before batch release. Adaptive offset correction for tool-wear diameter drift maintaining ±0.005mm compliance on OD turning programs without operator intervention. Groove width telescoping gauge at 3 angular positions per groove after machining; groove depth depth micrometer per groove per piston. In-process OD air gauge before and after groove machining. Thermal stabilization protocol documented for all aluminum piston programs. SPC Cpk ≥1.33 (≥1.67 on IATF 16949 special characteristics) on all OD and groove dimensions.
Final Inspection — 100% Groove & OD Verification
100% groove width telescoping gauge at 3 positions per groove per piston during production. Groove depth depth micrometer per groove per piston. 100% laser micrometer OD verification on all hydraulic piston programs — every part, not sampled. CMM: OD diameter and cylindricity; all groove positions, widths, and depths; internal thread position and concentricity; face flatness; overall length. Profilometry: OD seal contact surface Ra. Thread gauges: GO/NO-GO all threads. Eddy current: chrome or anodize thickness where specified. Mass verification per piston for balanced sets.
Matched Piston Set Verification
For hydraulic cylinder programs requiring matched piston-and-rod assemblies: individual pistons turned to specification with measured OD, groove dimensions, and bore concentricity recorded. Matched assembly verification on precision comparator — piston-to-rod concentricity and face perpendicularity confirmed before shipment. Each matched assembly tagged with measured dimensions and verified fit records, enabling cylinder assembler to confirm running clearance and seal compression before assembly. For high-pressure cylinders where dimensional variation governs seal life and leakage performance, matched assembly accuracy compresses variation below individual-tolerance outcomes.
Documentation Package
Certificate of Conformance · Laser micrometer OD diameter records (per lot) · Groove width and depth records (per groove per piston) · CMM dimensional report (concentricity, perpendicularity, shoulder positions, groove positions) · Profilometer OD seal contact surface Ra records · Thread gauge records · Material certifications with heat lot traceability · Heat treatment and coating certifications · PPAP Level 3 for volume hydraulic piston parts programs · FAIR per AS9102 for aerospace and defense programs · All records retained 20 years.
IATF 16949 Quality System for
Hydraulic Piston Parts
CNCPioneer's IATF 16949 and AS9100D certified hydraulic piston parts quality system addresses the four quality dimensions specific to precision piston machining: single-setup concentricity governance, in-process groove dimensional verification, OD surface finish direct from turning, and PPAP Level 3 bridge to volume hydraulic cylinder supply chain qualification.
Single-Setup Concentricity Governance
Groove-to-OD concentricity ±0.010mm and OD diameter ±0.005mm are structural guarantees — not outcomes of skilled operators achieving best possible results through multiple setups. CNCPioneer's MAZAK mill-turn single-setup piston programs make concentricity a machine-positioning accuracy outcome rather than a rechucking-uncertainty outcome: all grooves and OD features share the same spindle axis, eliminating re-registration error from the concentricity budget entirely. This structural guarantee extends through volume production without degradation — the ten-thousandth piston is as concentric as the first prototype, because the same programs run on the same machine spindle.
- Groove-to-OD concentricity ±0.010mm structural
- OD diameter ±0.005mm single-setup
- No rechucking error in concentricity budget
100% In-Process Groove Verification
Every hydraulic piston parts lot — every piston, every groove — receives in-process dimensional verification: telescoping gauge at 3 angular positions per groove for width; depth micrometer per groove for depth; and CMM groove network verification for concentricity. 100% verification rather than sampling eliminates the escape probability that sample-based inspection cannot eliminate when specification bandwidth is ±0.020mm and lot size ranges from 1 (prototype) to 100,000 (volume). This instrument suite resolves all three seal groove dimensions (width, depth, concentricity) that determine seal fit and hydraulic cylinder leakage performance.
- 100% groove width verification per groove per piston
- 100% groove depth verification per groove per piston
- CMM groove concentricity ±0.010mm per groove
Ra 0.2–0.4μm OD Surface Finish Direct from Turning
CNCPioneer's precision piston machining finish-turning achieves Ra 0.2–0.4μm directly on MAZAK spindles using CBN or PCD inserts — eliminating the post-turning grinding operations most hydraulic piston parts manufacturers require to reach seal-contact surface specifications. The single-finish-pass discipline is critical: each re-entry of the cutting tool produces a micro-step at the re-entry point that shows as periodic Ra deviation; the single-pass produces a clean spiral finish without re-entry artifacts. This capability distinguishes CNCPioneer from suppliers who must subcontract grinding, introducing lead time, cost, and grinding-setup dimensional variation.
- Ra 0.2–0.4μm direct from CNC turning
- CBN/PCD single-pass finish discipline
- No post-turning grinding for standard seal surfaces
PPAP Level 3 & Volume Supply Chain Qualification
PPAP Level 3 qualification for hydraulic cylinder OEM supply chains: design records, process flow (including single-setup sequence documentation), PFMEA (covering tool wear diameter drift, rechucking elimination, groove form failure modes), control plan, MSA Gage R&R on telescoping gauge and depth micrometer measurement systems, initial capability studies (Cpk ≥1.67 on IATF special characteristics: OD diameter, groove width, groove depth, groove concentricity), and part submission warrant. Generated on the same MAZAK programs used in volume production — prototype to PPAP qualification represents statistical progression on proven single-setup processes, not supplier transition with dimensional discontinuity. Volume blanket production at 500,000+ annual units per program.
- PPAP Level 3 for hydraulic cylinder OEM supply
- Cpk ≥ 1.67 on OD / groove width / groove depth
- MSA Gage R&R on groove gauging systems
Hydraulic Cylinder Piston Machining FAQ
Common questions from hydraulic cylinder manufacturers, mobile equipment OEMs, industrial automation builders, agricultural machinery producers, construction equipment companies, and marine hydraulic system manufacturers about CNCPioneer's hydraulic piston parts capability, seal groove tolerances, surface finish requirements, lead times, and volume program economics.
Seal groove tolerances for hydraulic pistons are specified by the seal manufacturer and vary by seal type and cross-section size. For O-ring seals (the most common): groove width = seal cross-section diameter × 1.35–1.45 to ±0.020mm; groove depth = seal cross-section diameter × 0.70–0.80 to ±0.020mm. When groove width is too narrow (below tolerance), the O-ring is laterally compressed into an oval cross-section, increasing rolling friction and creating asymmetric contact zones that wear the seal rapidly. When groove width is too wide, the O-ring sits in excess clearance and can twist, fold, or extrude into the gap between piston OD and barrel bore at operating pressure — the failure mode called O-ring extrusion that produces sudden complete leakage. When groove depth is too shallow (seal sticks out of groove), the barrel bore compresses the seal excessively — exceeding the seal's elastic limit and causing permanent set within the first few operating hours, after which the seal is insufficiently compressed to seal at low pressure. When groove depth is too deep, the seal drops into the groove with insufficient protrusion, producing inadequate contact stress against the barrel bore and leakage from the first operating cycle. CNCPioneer's ±0.020mm groove width and depth tolerance is the machining precision that keeps all groove dimensions within the seal manufacturer's functional range, regardless of dimensional variation between individual groove cutting passes.
Piston OD surface finish requirements differ by seal type based on how each seal develops its sealing contact. Dynamic O-rings (piston reciprocating in barrel) operate best on Ra 0.2–0.4μm piston OD — smooth enough that the elastomer's natural compliance creates a sealing contact zone without the asperity valleys that allow micro-leakage, but not so smooth that the oil film becomes too thin and seizes the rubber against the bore. Polyurethane U-cup seals and T-seals: Ra 0.1–0.3μm — these seals have harder lip geometry requiring smoother surface for uniform lip-to-surface contact. PTFE-bronze composite seals: Ra 0.1–0.2μm — PTFE seals work by direct polymer-to-metal contact at minimal oil film; rougher surface produces PTFE wear debris. Cast iron piston rings: Ra 0.3–0.6μm with specific profile (not just Ra) — ring seals require micro-waviness that retains oil film under ring scraping contact. CNCPioneer achieves Ra 0.2μm directly from CNC turning on MAZAK platforms using polycrystalline diamond (PCD) inserts on aluminum pistons and CBN inserts on hardened steel pistons. PCD cutting edge geometry produces Ra 0.1–0.15μm at optimized parameters (v_c = 800–1,200 m/min for aluminum, f = 0.08mm/rev, a_p = 0.05mm single finish pass); CBN achieves Ra 0.15–0.25μm on steel (v_c = 150–200 m/min, f = 0.05–0.08mm/rev). The single-finish-pass discipline — not multiple passes at reducing depth — is critical: each re-entry of the cutting tool produces a micro-step at the re-entry point that shows as periodic Ra deviation; the single-pass produces a clean spiral finish without re-entry artifacts.
Prototype lead times: standard 4140 steel single-groove hydraulic piston — 3–5 business days; 4140 + hard chrome plating — 5–7 days; 17-4PH H900 stainless piston — 5–7 days including aging heat treatment; aluminum 6061-T6 + Type III anodize — 4–6 days; brass C36000 — 3–4 days; bronze C93200 self-lubricating piston — 4–6 days. Multi-groove or complex geometry pistons (4+ grooves, internal milling features) add 1–2 days. Volume production: at 500–2,000 units annually, 30–45% per-unit reduction from prototype; at 2,000–10,000 units, 45–58% reduction with dedicated MAZAK program and zero-point fixture; at 10,000–50,000 units, 58–66% reduction with blanket order 2-week releases; above 50,000 units, maximum discount with safety stock buffer. Economics at representative scale: a 4140 hydraulic piston Ø80mm × 80mm long, 3-groove O-ring configuration (normalized, unplated) costs approximately $28 at CNCPioneer's prototype price and $8–10 at 10,000 annual units in hydraulic piston parts China production — versus $65–90 from a US hydraulic component machining facility at equivalent volume, and $45–70 from a European supplier. For a hydraulic cylinder OEM producing 10,000 cylinders annually with one piston each, China hydraulic piston parts savings of $35–60 per piston produce $350,000–$600,000 annual BOM cost reduction — a structural manufacturing cost advantage that enables hydraulic cylinder OEMs to compete on price in global hydraulic equipment markets.
Rechucking a piston between OD turning and groove machining introduces ±0.010–0.030mm concentricity error between OD and groove positions — error that appears as groove depth variation around the circumference (the groove is at correct depth at 0° but 0.020mm shallower at 180° from eccentricity). This error is not correctable by operator skill: it is a geometric consequence of rechucking uncertainty that accumulates independently at every setup change. CNCPioneer's MAZAK mill-turn programs machine piston OD and all seal grooves in one chucking, holding groove-to-OD concentricity at ±0.005mm by machine positioning rather than chuck re-registration. In volume production, this structural guarantee is decisive: the ten-thousandth piston machined on the same program has the same concentricity as the first prototype, because the concentricity is governed by machine positioning accuracy (±0.002mm repeatability) rather than by setup variation that drifts with operator change, chuck wear, and thermal state. Multi-setup suppliers cannot offer this guarantee — their concentricity is a statistical outcome of setup discipline, not a structural outcome of machine geometry.
For standard industrial and mobile hydraulic pistons to 350 bar: 4140 alloy steel (normalized or quench + temper to HRC 28–34) — the default material providing the best combination of strength, machinability, and case-hardenability. For hard chrome plating programs: 4140 is the standard substrate — chrome provides HV 900+ OD hardness and Ra 0.1–0.2μm seal contact finish. For corrosive service (seawater, chemical splash, food processing wash-down) where chrome plating is unacceptable: 17-4PH H900 stainless — 1,310 MPa yield, HRC 44–47, corrosion resistance equivalent to 304 stainless, machined in solution-annealed condition then aged to H900 with predictable dimensional growth of ±0.003–0.008mm. For lightweight mobile and aerospace actuators: aluminum 6061-T6 — 35% of steel mass, rated to 200 bar standard or 350 bar with steel thread inserts, with Type III hard anodize (HV 400+) on OD for barrel bore wear resistance. For self-lubricating or dust-laden environments: bronze C93200 (SAE 660) — sacrificial wear protects barrel bore, operates with minimal or no seal lubrication. For non-sparking ATEX or non-magnetic applications: brass C36000 — 100% machinability, certified for Zone 1 and Zone 2 explosive atmospheres, diamagnetic for MRI environments. CNCPioneer's 24-hour DFM review includes material selection guidance per piston against pressure class, corrosion environment, mass target, and seal type requirements.
Get a Quote for Hydraulic Cylinder Piston Machining
Upload your hydraulic piston drawings or specifications and receive a free DFM review and competitive hydraulic piston parts quotation within 24 hours — covering seal groove dimensions from your specified seal catalog number, OD running clearance from your barrel bore, surface finish achievability for your seal type, material recommendation for your pressure and environment, chrome or anodize allowance in machined dimensions, and complete pricing from prototype custom hydraulic piston parts through volume hydraulic piston parts China OEM supply.