
eVTOL Propeller &
Blade Grip Machining
CNCPioneer is an AS9100D certified eVTOL propeller and blade grip turn-mill machining specialist delivering fixed-pitch hub blade bore angular pitch ±0.010° (all blade bores from single C-axis MAZAK indexed program without rechucking), variable-pitch hub pitch bearing seat pair ±0.003mm concentricity single-setup, blade grip barrel OD ±0.003mm / inner bore coaxiality ±0.003mm, pitch horn angular position ±0.010°, and mass ±1g verified — for multirotor fixed-pitch hubs, variable-pitch propeller systems, tiltrotor prop-rotor heads, and folding cruise propellers at prototype through AS9100D wholesale supply.
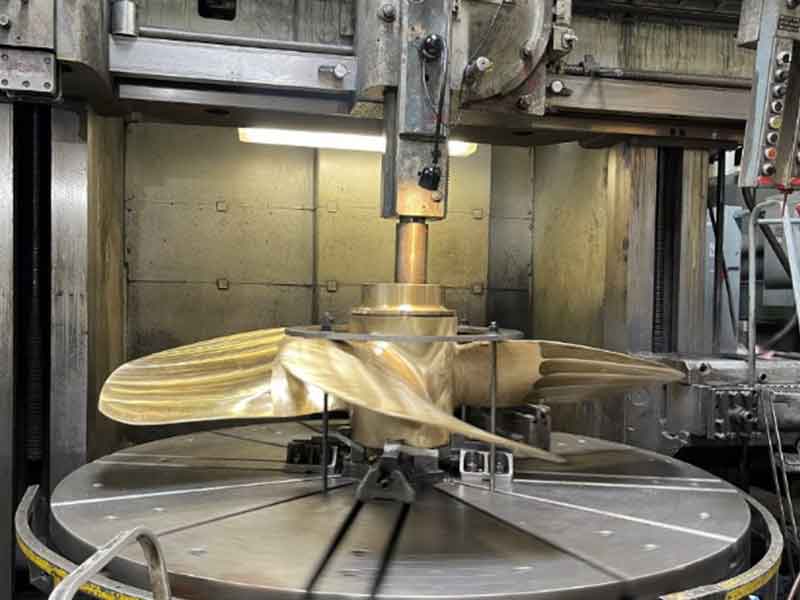
What Is eVTOL Propeller &
Blade Grip Turn-Mill Machining?
eVTOL propeller and blade grip turn-mill machining is the precision CNC manufacturing process — executed on MAZAK mill-turn centers in single-setup C-axis indexed programs, MAZAK VARIAXIS 5-axis simultaneous machining platforms, Swiss CNC turning systems, and wire EDM — that produces the hub bodies, blade grip assemblies, pitch control mechanisms, and rotor head structural components constituting the propulsion and rotor interface hardware of electric vertical takeoff and landing aircraft. The term "turn-mill" is deliberately specified because it identifies the most critical process architectural decision for propeller hub quality: the single-setup mill-turn program that machines all blade bores, all pitch bearing seats, and the central hub bore from one chucking without rechucking.
eVTOL propeller and rotor hub machining occupies a unique technical position — bridging helicopter rotor head precision and commercial eVTOL volume production requirements. Three engineering domains define the machining requirements. First, blade pitch angular symmetry: every blade must be at exactly the same pitch angle relative to the hub rotation plane. Angular error between blade stations produces once-per-rev vibration at blade passage frequency — for a 3-blade propeller at 2,000 RPM (33.3 Hz), ±0.010° angular accuracy from CNCPioneer's C-axis indexed single MAZAK program produces < 0.55 N lateral vibration force versus 14.8 N from ±0.054° multi-setup indexing approaches. Second, pitch bearing seat precision for variable-pitch systems: seat bore accuracy ±0.003mm governs bearing press-fit contact stress and pitch axis running accuracy — the prerequisite for 10,000+ flight hour pitch bearing life. Third, blade grip barrel geometry: outer OD ±0.003mm for pitch bearing engagement, inner bore coaxiality ±0.003mm, pitch horn angular position ±0.010° from blade axis — all from single-setup to eliminate rechucking eccentricity.
-
Single-setup C-axis indexed blade bore angular pitch accuracy All blade bores in an eVTOL propeller hub are drilled in one C-axis indexed MAZAK mill-turn program from one chucking without table repositioning — C-axis angular positioning accuracy ±0.001° per commanded position versus ±0.020–0.060° from multi-setup indexing fixture approaches. For a 3-blade hub at 2,000 RPM, CNCPioneer's ±0.002° inter-blade angular error from C-axis servo positioning produces < 0.55 N lateral vibration force at the hub — versus 14.8 N from conventional indexing fixture angular errors that are perceptible to aircraft passengers. Pitch bearing seat pair concentricity ±0.003mm is governed by the same single-setup principle.
-
Pitch bearing seat concentricity ±0.003mm from single-setup turn-mill Variable-pitch blade grip pitch bearing seat pairs (upper and lower, separated by 80–150mm axial distance) must be concentric to ±0.003mm — the specification that governs blade pitch axis running accuracy and prevents imposed bending moment on bearing outer rings that accelerates raceway fatigue. CNCPineer machines both pitch bearing seats from one MAZAK mill-turn spindle datum without rechucking, achieving ±0.003mm concentricity by machine positioning accuracy versus ±0.012–0.018mm eccentricity from rechucking between separate lathe operations.
-
Hub centrifugal stress DFM and TC4 material specification Every eVTOL propeller hub DFM review includes centrifugal stress calculation at the hub arm root cross-section at maximum hover RPM × safety factor 1.5 (per proposed FAA AC 21.17-1). Stress compared to TC4 AMS 4928 allowable (880/1.5 = 587 MPa tension) or TC4 AMS 6931 STA (1,000/1.5 = 667 MPa). If arm root stress exceeds AMS 4928 allowable — CNCPioneer recommends material upgrade to STA condition (no dimensional change; heat treat condition only) backed by engineering calculation. Missing shot peen specification on TC4 life-limited hub bodies is flagged in 35% of first-submission DFMs.
-
Blade grip mass matching and rotating imbalance control Commercial eVTOL aircraft production requires motor component supply with dedicated MAZAK capacity allocation, pre-purchased TC4 and 6063-T5 material stock, monthly blanket order releases with 2-week lead time, 100% critical dimension air gauge per component, and AS9100D production documentation per serial number. CNCPioneer's wholesale eVTOL motor component supply infrastructure operates at 100,000+ annual unit capacity — the supply chain continuity that eVTOL motor OEMs need for commercial production scaling.

Why CNCPioneer for
eVTOL Propeller Machining?
Among eVTOL propeller machining facilities globally, CNCPioneer's C-axis single-setup blade bore angular pitch accuracy, pitch bearing seat concentricity precision, 5-axis compound hub geometry capability, rotor engineering DFM, blade grip mass matching discipline, and China cost economics establish our facility as the preferred eVTOL propeller and blade grip machining partner across all propulsion configurations.
C-Axis Single-Setup Blade Bore Angular Pitch
All blade bores in an eVTOL propeller hub — 2, 3, 4, 5, or 6 blades — are drilled and reamed in one C-axis indexed MAZAK mill-turn program from one chucking without table repositioning. C-axis angular positioning accuracy ±0.001° per commanded position produces ±0.002° inter-blade pitch error versus ±0.020–0.060° from indexing fixture approaches. This quantitative difference translates to: lateral vibration force < 0.55 N versus 14.8 N in a representative 1,600 kg manned eVTOL at 2,000 RPM — below any passenger vibration perception threshold.
Pitch Bearing Seat Concentricity ±0.003mm Single-Setup
eVTOL propulsion components have compound-angle blade attachment interfaces, non-orthogonal bearing seat arrangements, and asymmetric structural geometries requiring 5-axis simultaneous machining for all critical features from one datum reference. CNCPioneer's MAZAK VARIAXIS programs machine eVTOL components with compound angle accuracy ±0.020°, bore-to-bore concentricity ±0.003mm from single setup, and blade pitch reference face perpendicularity 0.005mm — the geometric accuracy governing rotor track-and-balance performance and vibration levels in the assembled eVTOL aircraft.
5-Axis Compound Hub Geometry Machining
Modern eVTOL propeller hubs and rotor head bodies have compound blade attachment geometries — preconed blade attachment interfaces, asymmetric hub structures for fairings and actuator integration, articulated flapping and lag hinge arrangements — requiring 5-axis simultaneous machining at ±0.020° angular accuracy for all critical features from one datum reference. CNCPioneer's MAZAK VARIAXIS programs machine variable-pitch hub bodies, tiltrotor prop-rotor heads, and swash plate assemblies with compound feature relationships that 3-axis programs cannot achieve without fixture re-registration error.
eVTOL Rotor and Propeller Engineering DFM in 48 Hours
Variable-pitch propeller hubs for eVTOL have design-for-manufacture complexity that standard machining facilities cannot assess — pitch bearing seat accessibility from tool lengths, blade grip barrel L/D machinability at ±0.003mm bore, pitch horn attachment angular feasibility from 5-axis reference datum, hub arm root centrifugal stress adequacy. CNCPioneer's 48-hour DFM covers all these assessments: centrifugal stress calculation at arm root; C-axis blade bore angular program verification; pitch bearing seat tool reach analysis; pitch horn 5-axis collision check; mass estimate versus design target — returning actionable DFM before any material is committed.
Blade Grip Mass Matching as Production Standard
CNCPioneer verifies every blade grip to ±1g against the matched-set mean mass, and every propeller hub against design model mass ±1g, on calibrated precision balance recorded per serial number. Matched-set blade grips — all grips for one hub within ±1.5g total spread — are packaged together as pre-verified matched sets, eliminating blade grip re-sorting at propeller OEM assembly. Mass records per serial number feed directly into the eVTOL aircraft weight and balance database for center-of-gravity compliance without weighing the assembled propulsion unit.
40–60% China Propeller Machining Cost Advantage
Variable-pitch propeller hub and blade grip components from US and European specialist rotorcraft machining facilities cost 2–3× CNCPioneer's AS9100D equivalent pricing. At 2,000 aircraft/year (8,000 variable-pitch hub kits/year): CNCPioneer's complete 3-blade variable-pitch kit (hub + 3 grips + 3 pitch horns) at $1,100–$1,650 versus $2,800–$4,500 from US/European specialists — the structural cost reduction essential for commercial air taxi propulsion system BOM targets. Fixed-pitch hubs at 1,000–5,000 hubs/year: $290–$420 versus $650–$900 from western rotorcraft machining facilities.
eVTOL Propeller & Rotor Components
We Machine
CNCPioneer's eVTOL propeller and blade grip machining programs cover the complete machined component architecture of eVTOL propulsion systems — from fixed-pitch multirotor hub bodies and variable-pitch hub bodies through blade grip barrels, pitch horns, collective pitch spiders, swash plate assemblies, tiltrotor rotor head bodies, and folding propeller hinge mechanisms at prototype through AS9100D wholesale volume.

Fixed-Pitch Propeller Hubs
Fixed-pitch hubs for multirotor eVTOL lift systems — the most widely produced eVTOL propeller component. Spider hub and disc hub variants; 2–8 blade attachment bores at equal angular pitch ±0.010° from single C-axis indexed MAZAK program; center bore ±0.003mm for motor shaft engagement; blade bore perpendicularity to hub rotation plane 0.010mm per bore; retention bolt circle ±0.010mm true position; hub face flatness 0.010mm; balance boss machined for post-assembly balance access Ra 3.2μm. Materials: 7075-T6 (standard commercial programs); TC4 AMS 4928 (high-RPM cruise propeller, 100kg+ thrust class). Type III hard anodize; G1.0 balance; mass ±1g; FAIR per AS9102.

Variable-Pitch Propeller Hub Bodies
Variable-pitch hub bodies for multirotor collective pitch, tiltrotor prop-rotor, and advanced eVTOL efficiency programs — the mechanically most complex machined propeller component. Pitch bearing seat pairs per blade station: ±0.003mm bore / ±0.003mm pair concentricity from single MAZAK mill-turn setup; inter-blade angular pitch ±0.010° from C-axis indexed single program; pitch horn attachment features ±0.010° from blade station bore axis; pitch mechanism interface (spider / swash plate attachment) angular symmetry ±0.010°; 5-axis compound geometry for precone angle ±0.020°. Material: TC4 AMS 4928 or AMS 6931 STA per arm root stress analysis. Shot peen AMS 2430; FAIR per AS9102.

Blade Grip Barrels
Blade grip barrels serve as the structural intermediary between propeller blade and hub pitch axis bearing — receiving centrifugal, bending, and torsional blade loads while allowing smooth pitch rotation. Swiss CNC programs (Ø30–60mm × 80–150mm L/D ≤ 3:1): guide bushing support mandatory; upper pitch bearing seat OD ±0.003mm / lower seat OD ±0.003mm / pair coaxiality ±0.003mm from guide bushing zone; blade root bore ±0.020mm; through-bolt holes ±0.010mm true position; pitch horn reference flat ±0.010° from blade pitch datum. MAZAK mill-turn programs (Ø60–120mm × 150–350mm): both pitch bearing seats from same spindle datum ±0.003mm concentricity. Mass verified ±0.5g per grip; matched-set packaging ±1.5g total spread.

Pitch Horns & Collective Pitch Spiders
Pitch horns transmit collective pitch actuator force to blade grip rotation. Hub-attachment bore ±0.003mm; angular position on blade grip ±0.010°; actuator attachment bore (clevis or rod end) ±0.005mm / bore pair coaxiality ±0.005mm; moment arm length from pitch axis ±0.200mm — matched within ±0.100mm across all horns in one hub set for equal pitch change rate per blade; TC4 horn fatigue fillet R2.0–3.0mm ±0.100mm / shot peened AMS 2430. Collective pitch spider body (5-axis 7075-T6 disc): pitch-link attachment bores ±0.010mm per blade / angular symmetry ±0.010°; guide bore ±0.020mm H8 for smooth axial travel on hub pilot; disc face flatness 0.010mm; anti-rotation slot ±0.020mm. Actuator rod attachment ±0.010mm position.

Tiltrotor Rotor Head & Swash Plate Components
Tiltrotor prop-rotor head body (fully articulated): flapping hinge bore ±0.005mm / pin bore pair coaxiality ±0.005mm; lag damper attachment bore pair ±0.010mm / angular position from flapping axis ±0.020°; pitch axis housing: pitch bearing seat ±0.003mm — all articulation features from 5-axis machining in one hub body datum reference. Material: TC4 AMS 6931 STA mandatory — tiltrotor hub sees combined flapping, lag, and pitch loads simultaneously. Swash plate assemblies: non-rotating ring face flatness 0.010mm / bore ±0.010mm; rotating ring lower face flatness 0.010mm / pitch link attachment bores ±0.010mm per blade; spherical bearing housing ±0.005mm; contact face Ra 0.4μm; 5-axis machined guide features.

Folding Propeller Mechanisms & Contra-Rotating Hubs
Folding propeller hinge mechanisms (stowable lift propellers for lift+cruise eVTOL): fold hinge bore pair ±0.005mm / pair coaxiality ±0.005mm; bore pair perpendicularity to blade span 0.010mm; fold lock bore/groove angular position ±0.020° for positive blade position lock; fold lock over-center geometry by 5-axis milling ±0.010mm; fold spring housing ±0.050mm; fold stop face hardened for repeated contact. Material: TC4 for lightweight dynamic folding at operating RPM. Contra-rotating propeller hub pairs: outer hub OD ±0.003mm for outer shaft mating flange / blade bore array ±0.010° inter-blade pitch; inner hub bore ±0.003mm for inner shaft; outer and inner hub blade bore arrays staggered by 360°/(2×N_blades) for acoustic benefit — matched pairs with phasing reference feature ensuring correct inter-rotor blade phasing at assembly.
Industries & Applications
CNCPioneer's eVTOL propeller and blade grip machining serves the complete eVTOL propulsion supply chain — from eVTOL aircraft manufacturers and variable-pitch propeller OEMs through urban air mobility propulsion integrators, eVTOL blade manufacturer partners, electric air taxi propulsion Tier 1 suppliers, contra-rotating propulsion unit builders, and certification engineering partners requiring AS9100D documented eVTOL propeller component programs worldwide.
eVTOL Aircraft
Complete propeller hub and blade grip machined component programs — fixed-pitch multirotor lift hubs; variable-pitch hub bodies with pitch mechanism features; blade grip barrel matched sets; pitch horn sets; collective pitch spiders; and complete variable-pitch propeller machined component kits with prototype-to-certified production continuity. AS9100D production documentation and AS9102 FAIR for all propeller safety-classified components. Volume wholesale supply programs at aircraft production rates from 50 to 5,000 aircraft annually.
Variable-Pitch Propeller System
Dedicated propeller machining programs for variable-pitch propeller OEMs (Javiation-type and equivalent programs) supplying propeller assemblies to eVTOL aircraft integrators — pitch bearing seat bore programs at ±0.003mm with production SPC Cpk ≥1.67; blade grip barrel programs with AS9100D traceability per matched-set serial number; prototyping service with 48-hour DFM and 8–16 day first article delivery. Wholesale blanket order supply programs with dedicated MAZAK capacity, pre-purchased TC4 and 7075-T6 material stock, and 2-week monthly releases for propeller OEM production lines.
Urban Air Mobility Propulsion
Integrated propulsion system suppliers — motor + propeller hub as a unit — source motor shaft, propeller hub body, and blade grip matched sets from CNCPioneer under one AS9100D supply relationship. Single-source machined component supply eliminates inter-supplier angular datum stack-up (hub blade bore datum coordinated with motor shaft spline datum in one program database) and provides single-point quality accountability for the complete propulsion unit mechanical architecture. CNCPioneer maintains CNC program identity and matched-set traceability across all program phases — saving 3–6 months re-qualification when eVTOL programs transition from development to production.
Electric Air Taxi Propulsion
Propulsion Tier 1 suppliers providing motor + propeller units to eVTOL OEMs benefit from CNCPioneer's IATF 16949 automotive certification supplementing AS9100D — providing the automotive quality infrastructure (PPAP Level 3, SPC, APQP, MSA Gage R&R) that automotive-experienced Tier 1 suppliers require, combined with AS9100D for aerospace regulatory compliance. 100% blade bore angular CMM per hub, 100% pitch bearing seat air gauge per variable-pitch component, and blanket order wholesale supply at volume propeller production rates.
eVTOL Blade
Propeller blade manufacturers who produce composite or metallic blade assemblies source hub bodies and blade grip barrels from CNCPioneer to complete their propeller assembly offering — CNCPioneer supplies blade grips pre-verified as matched-mass sets, with pitch horn reference flats at correct angular datum relationship to the blade root bore interface, enabling blade manufacturers to assemble complete variable-pitch propeller units from CNCPioneer's machined metal components and their own blade structures. Coordinated program scheduling ensures hub delivery aligned to blade production cycle time.
eVTOL Certification Engineering
Engineering service companies supporting eVTOL OEMs through FAA/EASA type certification — CNCPioneer provides manufacturing substantiation data (capability studies on blade bore angular pitch, pitch bearing seat concentricity, and hub arm root fillet radius; material traceability records; shot peen process qualification data) that certification engineers use to demonstrate manufacturing process capability to airworthiness authority expectations. 99% first-submission FAIR qualification rate; Cpk ≥ 1.67 on all propeller hub critical characteristics; complete AS9102 FAIR packages with UT billet inspection records in DAH-compatible format.
eVTOL Propeller Machining
Process & Capabilities
CNCPioneer's eVTOL propeller machining process runs on 66+ MAZAK mill-turn centers with C-axis indexed single-setup blade bore programs, MAZAK VARIAXIS 5-axis platforms for compound hub geometry and pitch horn machining, 78+ Swiss CNC lathes for blade grip barrels above L/D = 3:1, and wire EDM for pitch mechanism splines and fold lock geometry — delivering blade bore angular pitch ±0.010°, pitch bearing seat pair concentricity ±0.003mm, and mass matching ±1g as production standards.
Propeller Hub Engineering DFM in 48 Hours
Six engineering analysis areas within 48 hours: (1) centrifugal stress at hub arm root from blade mass × RPM × safety factor (1.5 manned / 1.2 cargo drone) versus TC4 AMS 4928 or AMS 6931 STA allowable — with material recommendation and engineering calculation; (2) pitch bearing seat machining feasibility from tool reach / L/D for single-setup concentricity; (3) C-axis blade bore angular program verification with chip clearance check between C-axis positions; (4) pitch horn 5-axis tool path collision check against hub body geometry; (5) hub mass estimate versus design target from CAD solid; (6) shot peen specification completeness check — 35% of first submissions arrive without AMS 2430 callout on life-limited TC4 hub bodies.
Fixed-Pitch Hub Turn-Mill Sequence
Billet SII XRF + hardness → 5-axis rough all hub profile with 1.5mm stock → hub bore rough → Thermal stabilization 25 minutes (7075-T6 CTE 23.4 ppm/°C) → Hub center bore finish ±0.003mm / Ra 0.4μm / motor shaft engagement depth ±0.050mm → C-axis blade bore array ALL bores from one program: C0° bore 1 (center drill → drill → ream ±0.005mm; perpendicularity 0.010mm) → C90°/C120°/C72° bore 2 → C180°/C240°/C144° bore 3 → continue per blade count → CMM in-process probe check bores 1 and N before proceeding → bolt circle holes per blade station at same C-axis position → hub OD and fairing face 5-axis finish → deburring under 10× → FAIR per AS9102 → Type III hard anodize → post-anodize blade bore air gauge 100% → mass verification ±1g.
Variable-Pitch Hub Body Sequence
TC4 billet SII XRF + hardness + UT (manned programs) → 5-axis rough all hub arm geometry with 2mm stock; trochoidal TC4 toolpaths; 70 bar coolant → Thermal stabilization 4 hours at 20°C ±1°C (TC4 7 W/m·K thermal conductivity persists gradients longer than aluminum) → Center hub bore finish ±0.003mm → Motor flange face flatness 0.010mm / bolt circle ±0.010mm → Blade station 1 (C0°): upper pitch bearing seat ±0.003mm H6 / lower pitch bearing seat ±0.003mm same C-axis position / in-process CMM concentricity before proceeding → Blade stations 2, 3 (C120°, C240°): identical sequence → Pitch horn attachment features ±0.010° from blade station bore axis → Pitch mechanism interface (spider attachment points) ±0.010° angular symmetry → 5-axis compound precone angle finish ±0.020° → CMM FAIR → Shot peen AMS 2430 masked on pitch bearing seats.
Blade Grip Barrel Swiss CNC & Mill-Turn
Swiss CNC (Ø30–60mm × 80–150mm, L/D ≤ 3:1): TC4 bar through guide bushing (clearance 0.003mm from bar OD); guide bushing zone establishes OD concentricity within 0.001mm of spindle axis → Upper pitch bearing seat OD ±0.003mm / Ra 0.2μm → Lower pitch bearing seat OD ±0.003mm / concentricity to upper ±0.003mm from same guide bushing zone → Blade root bore (gun drill if L/D > 10:1) ±0.020mm → Cross-drilled through-bolt holes ±0.010mm true position → Pitch horn reference flat ±0.010° from pitch datum → Mass verification ±0.5g. MAZAK mill-turn (Ø60–120mm): both pitch bearing seats from same spindle datum ±0.003mm concentricity → Blade root bore precision boring → Pitch horn arm C-axis milled ±0.010° → Wire EDM slit for T-bolt barrel clamping feature → Matched-set packaging ±1.5g total spread.
5-Axis Compound Hub & Rotor Head Machining
MAZAK VARIAXIS 5-axis simultaneous machining for all eVTOL propeller compound geometry features: compound blade attachment angles (designed precone angle ±0.020° from hub rotation axis for aeromechanical stability); tiltrotor prop-rotor head with flapping hinge / lag damper / pitch axis in compound geometric relationship from one hub body datum; swash plate guide face angles; folding propeller hinge geometry and fold lock over-center profile. Angular positioning accuracy ±0.005° per axis; compound angle accuracy ±0.008° from dual-axis combination; maximum workpiece envelope 1,200mm × 1,000mm × 800mm. Pitch horn 5-axis machining: 5-axis tool path collision verification against hub body geometry at all tool orientations before machining commitment.
100% Angular CMM & Mass Verification
100% blade bore angular CMM per hub: direct 5-axis angular measurement between bore axes; all blade stations verified ±0.010°; records per hub serial number before shipment. 100% pitch bearing seat air gauge: every variable-pitch hub and every blade grip barrel; pitch seat pair concentricity by CMM roundness tester per grip; records per serial number. 100% mass verification: every hub and every blade grip on calibrated precision balance ±0.1g resolution; matched-set documentation per hub assembly (all grips within ±1.5g total spread). G0.4 dynamic balance for high-speed cruise propeller programs; G1.0 for lift rotor hubs. Shot peen AMS 2430 Almen strip per lot + coverage verification photos per life-limited component serial number in AS9102 FAIR package.
Materials for eVTOL Propeller
Hub & Blade Grip Programs
eVTOL propeller hub material selection is governed by centrifugal stress at hub arm root (primary structural driver), fatigue endurance at 10⁸–10⁹ cycles, density for mass budget, and regulatory safety factor (manned SF 1.5 / cargo drone SF 1.2). Blade grip material is governed by pitch bearing seat machinability to ±0.003mm and combined CF + bending fatigue. 7075-T6 dominates commercial fixed-pitch programs; TC4 AMS 4928 governs life-limited and 100kg+ thrust hubs.
TC4 Titanium (AMS 4928 Annealed)
950 MPa yield · 4.43 g/cm³ · fatigue endurance 600 MPa · The primary material for eVTOL variable-pitch hub bodies and 100kg+ thrust class fixed-pitch lift rotor hubs — best specific strength (220 kN·m/kg) of any commonly machined aerospace alloy. Hub arm root allowable tension at SF 1.5 (manned) = 880/1.5 = 587 MPa. CNCPioneer TC4 AMS 4928 hub machining: v_c = 50–80 m/min; through-spindle coolant 70 bar; trochoidal toolpaths at hub arm pocket transitions; dedicated fresh insert for all arm root fillet passes; 4-hour thermal stabilization before precision pitch bearing seat operations. Non-magnetic: important for motor-adjacent propeller hub applications where stray flux could affect resolver sensing.
TC4 STA (AMS 6931 Solution Treated & Aged)
1,100 MPa yield · 4.43 g/cm³ · fatigue endurance 650 MPa · Required for tiltrotor prop-rotor hub bodies (combined hover centrifugal + cruise aerodynamic loads simultaneously) and manned eVTOL blade grips where arm root stress at SF 1.5 exceeds TC4 AMS 4928 allowable (880/1.5 = 587 MPa). Hub arm root allowable at SF 1.5 (STA) = 1,000/1.5 = 667 MPa — 14% margin improvement. CNCPioneer STA hub machining: UT incoming billet per AMS 2154 Class A; cutting speed reduced 15% from annealed parameters; Rockwell hardness HRC 35–40 verified after machining to confirm STA not over-aged. Shot peen AMS 2430 mandatory for all life-limited TC4 STA hub bodies.
Aluminum 7075-T6
572 MPa yield · 2.80 g/cm³ · Fatigue endurance 160 MPa · The workhorse material for commercial eVTOL fixed-pitch multirotor hub programs — adequate hub arm fatigue life in most commercial multirotor lift rotor applications where centrifugal stress at arm root ≤ 160 MPa × appropriate fatigue safety factor. Density advantage (2.80 vs 4.43 g/cm³ for TC4) makes 7075-T6 the default aluminum specification for fixed-pitch hubs where structural calculation confirms adequacy. CNCPioneer 7075-T6 hub machining: 500+ m/min cutting speed; Ra 0.4μm blade bore and pitch bearing seat achievable directly from precision boring; 25-minute thermal stabilization before precision bore operations. Type III hard anodize standard on blade bore retention zones; post-anodize bore 100% air gauge.
Aluminum 2024-T4
470 MPa UTS · 2.78 g/cm³ · Fatigue endurance 138 MPa · For blade grip barrels with sustained high centrifugal tension loading where 7075-T6's susceptibility to stress corrosion cracking under sustained bolt preload combined with moisture exposure creates SCC risk. 2024-T4 provides superior SCC resistance versus 7075-T6 at slightly lower density — the design choice that governs blade grip material selection in coastal UAM operations and high-humidity aviation environments. CNCPioneer 2024-T4 blade grip machining: pitch bearing seat OD ±0.003mm achievable from precision turning; through-bolt hole pattern ±0.010mm true position. Type III hard anodize on pitch bearing seat OD surfaces; anodize growth allowance pre-calculated per alloy-anodize combination with post-anodize 100% air gauge verification.
17-4PH H900 Stainless Steel
1,310 MPa yield · HRC 44–47 · 7.78 g/cm³ · fatigue limit 620 MPa · For pitch horns, pitch pins, and precision coupling features requiring high strength combined with corrosion resistance and non-magnetic behavior. 17-4PH H900 is finish-machined to bearing-quality surfaces without post-machining grinding — HRC 44–47 hardness is machinable at ±0.003mm without precision grinding in most hub and blade grip interface programs. Pitch horn actuator attachment bore ±0.005mm / pair coaxiality ±0.005mm; moment arm ±0.100mm; hub-attachment bore ±0.003mm. Age-harden-after-machining sequence: machine in solution-annealed condition → H900 precipitation (315°C × 3h) → post-age passivation ASTM A967 → final CMM inspection. Non-magnetic — important for pitch position sensor proximity to blade grip.
4340 Steel (QT HRC 38–42)
1,310 MPa yield · HRC 44–47 · 7.78 g/cm³ · fatigue limit 620 MPa · For eVTOL motor shafts requiring the combination of high strength, corrosion resistance without protective coating, and non-magnetic behavior — particularly motors in coastal UAM operations, high-humidity environments, or frequent water exposure. 17-4PH H900 is finish-turned to bearing-quality surfaces without post-machining grinding — HRC 44–47 hardness is machinable at ±0.002mm without precision grinding in most journal programs. Age-harden-after-machining sequence: machine in solution-annealed condition → verify pre-age dimensions → H900 precipitation (315°C × 3 hours) → post-age passivation ASTM A967 → final CMM inspection.
Aluminum 6061-T6
572 MPa yield · 2.80 g/cm³ · Fatigue endurance 160 MPa · The workhorse material for commercial eVTOL fixed-pitch multirotor hub programs — adequate hub arm fatigue life in most commercial multirotor lift rotor applications where centrifugal stress at arm root ≤ 160 MPa × appropriate fatigue safety factor. Density advantage (2.80 vs 4.43 g/cm³ for TC4) makes 7075-T6 the default aluminum specification for fixed-pitch hubs where structural calculation confirms adequacy. CNCPioneer 7075-T6 hub machining: 500+ m/min cutting speed; Ra 0.4μm blade bore and pitch bearing seat achievable directly from precision boring; 25-minute thermal stabilization before precision bore operations. Type III hard anodize standard on blade bore retention zones; post-anodize bore 100% air gauge.
Titanium Ti-6Al-4V
880 MPa yield · 4.43 g/cm³ · Non-magnetic · Distal joint output shafts (wrist, finger, elbow) where titanium's specific strength delivers 43% mass reduction versus 17-4PH H900 at comparable strength — reducing distal link inertia, actuator sizing, and battery draw. MRI-compatible surgical robot bearing components: titanium's non-magnetic property (μᵣ ≈ 1.0005) satisfies MRI-compatibility requirements that ferromagnetic steel (μᵣ = 200–1000) fails. DLC coating on titanium bearing-interface zones compensates titanium's lower surface hardness (HRC 36) relative to bearing steel requirements at rolling contact surfaces.
PEEK Engineering Grade
ASTM E595 TML ≤0.030% · Excellent dielectric · Chemical resistance · PEEK for electrical isolation and non-magnetic structural components in motor-adjacent eVTOL structures — motor HV feedthrough insulator bodies, sensor mounting isolation bushings, rotor position encoder mounting bodies, and non-conductive structural elements in eVTOL propulsion system assemblies where metallic parts would create magnetic interference. CNCPioneer machines PEEK on the same MAZAK mill-turn platforms as metallic eVTOL components — delivering the same AS9102 FAIR documentation and mass verification (±0.5g per component) as metallic eVTOL structural parts. No post-machining heat treatment required; final CMM dimensional inspection confirms compliance before lot release.
Surface Treatments for
eVTOL Propeller Components
eVTOL CNC machining surface treatment selection addresses fatigue life enhancement on life-limited TC4 rotating components (shot peen AMS 2430), wear resistance and corrosion protection on 7075-T6 structural aluminum (Type II/III anodize), corrosion protection on stainless and 17-4PH parts (passivation ASTM A967), EMI bonding conductivity on aluminum structural fittings (Alodine MIL-DTL-5541), and recast layer management on wire EDM fatigue-critical features — all with allowances machined-in and verified post-treatment.
Passivation — ASTM A967
Shot peening per AMS 2430 is mandatory for all eVTOL life-limited TC4 rotating components — the compressive residual stress layer increases fatigue endurance limit by 20–40% at the stress concentration features (shaft shoulder fillets, bore transitions) governing component life. Almen A 0.15–0.25mm intensity range; 98–100% coverage verification per SAE AMS 2430; CNCPioneer coordinates shot peen at AS9100D qualified aerospace shot peen facilities with peening records (Almen strip results + coverage verification photos) per shaft serial number. Bearing seats and motor flange faces are masked before peening to preserve dimensional accuracy. Shot peen adds 3–4 business days to eVTOL component lead times and is included in CNCPioneer's 48-hour DFM review scope and program pricing.
Type III Hard Anodize — MIL-A-8625 (Aluminum Hub Bodies)
HV 400+ wear resistance for 7075-T6 and 2024-T4 aluminum propeller hub bodies — blade attachment bore retention zones, bolt hole countersink zones, hub arm surfaces subject to handling and installation contact. Black hard anodize on non-contact hub surfaces for UV resistance in exposed propeller nacelle environments. Pitch bearing seat surfaces: masked or post-anodize fine-bored to final dimension if anodize growth (20–50μm per side on 7075-T6 from hard anodize) would consume bearing seat tolerance. CNCPioneer's anodize allowance management incorporates predicted growth per alloy-anodize combination; post-anodize blade bore air gauge 100% and pitch bearing seat air gauge 100% on variable-pitch hub programs. Black hard anodize blade bore entry chamfers for corrosion protection at blade root T-bolt contact zone.
Shot Peen — AMS 2430 (TC4 Life-Limited Hub & Blade Grip)
Compressive surface stress induction at Almen A 0.18–0.22mm intensity for all TC4 propeller hub bodies and blade grip barrels classified as life-limited structural parts — extending TC4 fatigue life by 50–100% at the hub arm root fillet and blade grip shoulder transitions where centrifugal tensile stress is the fatigue driver. Coverage: 98% minimum all external surfaces; pitch bearing seat OD surfaces masked; pitch datum reference features masked to maintain geometric precision. CNCPioneer coordinates shot peen at AS9100D qualified aerospace shot peen subcontractor; peening records (Almen strip results + coverage verification photos) per component serial number. Shot peen adds 3–4 business days and is flagged as missing in 35% of first-submission TC4 hub DFM reviews — CNCPioneer adds specification as DFM finding.
Passivation — ASTM A967 (17-4PH & Stainless Pitch Hardware)
Mandatory post-machining passivation for all 17-4PH H900 pitch horns, pitch pins, and stainless precision pitch hardware — removes machining free iron, restores the passive chromium oxide layer, and prevents flash rusting in outdoor aviation humidity exposure and coastal UAM operating environments. Applied after all machining is complete including through-bolt holes, bore operations, and pitch horn arm features; passivation liquid penetrates all internal features uniformly. For 17-4PH H900 programs: applied after H900 precipitation hardening (315°C × 3h) as the final surface treatment step before CMM inspection. Passivation certificate per lot; post-passivation dimensional verification on all ±0.003mm pitch horn bore features confirms zero dimensional impact before lot release.
PTFE Release Treatment & Corrosion Inhibiting Compound
PTFE dispersion release treatment for pitch axis sliding surfaces in non-bearing pitch control designs (PTFE-lined plain bearings or dry-running pitch control elements): PTFE applied to blade grip outer surface in pitch sliding zone; reduces static friction (stiction) in pitch control mechanism critical for actuator precise collective pitch positioning; applied post-anodize (aluminum) or post-passivation (stainless); dimensional change ≤0.003mm. Corrosion Inhibiting Compound (CIC) per MIL-PRF-16173 applied to TC4 and aluminum propeller hub bores and mating faces during shipping and pre-installation storage — temporary corrosion protection compatible with grease or sealant applied at aircraft assembly. CIC prevents oxidation at precise machined interfaces (blade bore retention zones, pitch bearing seat ODs) during international air freight and warehouse storage before installation.
Dynamic Balance — G0.4 (High-Speed Cruise Propeller Hubs)
ISO 1940 G0.4 (residual unbalance ≤0.2 g·mm/plane) for high-speed cruise propeller hubs operating above 2,000 RPM — at 4,000 RPM, 1 g·mm imbalance generates 112 N centrifugal force, creating vibration detectable in the aircraft cabin. G1.0 (≤0.5 g·mm/plane) for lift rotor hubs at lower RPM. Balance correction on hub body balance boss: material removal from machined ring pad by CNCPioneer balancing team; balance ring geometry (OD, thickness, access clearance) reviewed in DFM to ensure balance correction access after hub assembly. Blade grip mass matching replaces individual grip balance in most programs — all grips within ±1.5g total spread eliminates first-order rotating imbalance from grip-to-grip mass variation. Dynamic balance record (plane, residual unbalance, correction applied) per hub serial number in AS9102 FAIR package.
All surface treatments on eVTOL propeller component programs — Type III hard anodize (blade bore and pitch bearing seat growth allowance machined-in; post-anodize 100% air gauge), shot peen AMS 2430 (Almen strip + coverage photos per serial number for life-limited TC4 hubs and blade grips), passivation ASTM A967 (17-4PH pitch horns and pitch pins), PTFE release treatment, and CIC shipping protection — are documented with treatment certifications and post-treatment dimensional verification in the AS9102 FAIR package. Treatment allowances are machined-in and confirmed post-treatment by air gauge, ensuring all specifications are met in the final delivered condition.
Quality Assurance for
eVTOL Propeller Machining Programs
eVTOL propeller and blade grip machining quality assurance addresses blade bore angular pitch (100% CMM per hub), pitch bearing seat concentricity (100% air gauge and roundness tester per variable-pitch component), hub arm root fillet verification (CMM optical probe per TC4 life-limited hub), dynamic balance, and AS9102 FAIR — with material traceability per serial number and Cpk ≥ 1.67 on all propeller hub special characteristics for eVTOL wholesale production programs.
Propeller Hub Engineering DFM & Contract Review
48-hour DFM covering: centrifugal stress at hub arm root from blade mass × maximum RPM × safety factor versus TC4 AMS 4928 or AMS 6931 STA allowable (material recommendation with engineering calculation); C-axis blade bore angular program feasibility with chip clearance check between C-axis positions; pitch bearing seat machining feasibility from tool reach L/D for single-setup concentricity ±0.003mm; pitch horn 5-axis tool path collision verification against hub body geometry; hub mass estimate versus design target from CAD solid; shot peen and Type III anodize specification completeness check — all six findings delivered as actionable DFM report within 48 hours.
Material Verification & Billet UT Inspection
SII XRF composition verification on every propeller material lot: TC4 AMS 4928 (Al 5.5–6.75%; V 3.5–4.5%; Fe ≤0.30%); TC4 AMS 6931 STA (same composition; condition verified by hardness HRC 35–40); 7075-T6 (Zn 5.1–6.1%; Mg 2.1–2.9%; Cu 1.2–2.0%); 2024-T4 (Cu 3.8–4.9%; Mg 1.2–1.8%); 17-4PH H900 (Cr 15.0–17.5%; Ni 3.0–5.0%; Cu 3.0–5.0%). Hardness per heat treat condition. UT per AMS 2154 Class A for TC4 STA life-limited hub body billets and TC4 blade grip barrels on manned eVTOL programs (billet section submitted; UT records archived per heat/hub serial chain). Full traceability: mill certificate heat number → CNCPioneer machining lot → hub or blade grip serial number.
In-Process Hub & Blade Grip Controls
TC4 hub body: tool wear monitoring on arm root fillet machining and pitch bearing bore operations — carbide insert assessed every 5 hub bodies; fresh inserts mandatory before all arm root fillet passes. C-axis angular positioning verification: at-machine CMM probe verification of blade bore 1 and blade bore N angular positions after programming completion — confirms no C-axis drift before all bores are committed. Pitch bearing seat pair concentricity: in-process CMM immediately after finish boring second seat; if concentricity exceeds 0.002mm, root cause investigated before batch continuation. Blade grip mass measurement: every grip weighed during production to detect material variation before investing machining time; grip >2g from design mass investigated before processing continues. 4-hour thermal stabilization documented per TC4 hub lot.
Final Inspection — 100% Angular CMM & Mass Verification
100% blade bore angular CMM per hub (all blade bores; direct 5-axis angular measurement between bore axes; records per hub serial number); 100% pitch bearing seat air gauge per variable-pitch hub and per blade grip barrel; pitch seat pair concentricity CMM roundness tester per grip. Mitutoyo CMM (±0.001mm): hub center bore; blade bore perpendicularity; bolt circle true position; hub motor interface face flatness; pitch horn angular positions (5-axis angular measurement); arm root fillet radii (TC4 fatigue-critical, optical probe ±0.010mm); swash plate face flatness. Mass: every hub on calibrated balance ±0.1g; every blade grip ±0.1g; matched-set documentation per hub assembly. Dynamic balance G1.0 or G0.4 per high-speed cruise program; balance record per hub serial number. Visual under 10×: no burrs at blade bore entries; no tool marks on pitch bearing seat bore surfaces.
Shot Peen & Matched-Set Mass Records
Housing pressure test: 100% every housing at 1.5× rated coolant pressure; 30-second hold; zero pressure decay acceptance; test results recorded per housing serial number in AS9102 FAIR. Leak failure: housing quarantined; channel geometry inspected for wall breach; MRB disposition before any re-work. Shot peen coordination: CNCPioneer coordinates at AS9100D qualified aerospace peen facility; peened motor shaft returns with Almen strip results per batch and coverage verification photos per shaft serial number; CNCPioneer verifies 98–100% coverage before accepting peening lot; post-peen journal dimension check confirms distortion within tolerance; complete peen records in FAIR package.
AS9102 FAIR & Life-Limited Part Records
FAIR per AS9102: 100% of drawing dimensions measured (including all blade bore angular positions by 5-axis CMM measurement); measurement uncertainty ≤10% of tolerance; material certification with heat/lot traceability; SII XRF composition verification; hardness verification; shot peen certificate per AMS 2430 (Almen strip + coverage photos per hub or blade grip serial number for life-limited TC4 components); dynamic balance record per hub (G1.0 or G0.4); matched-set mass documentation per blade grip set; Type III anodize certificate per lot; CMM optical probe fillet radius records (arm root, pitch horn transitions). Life-limited part records: for all TC4 propeller hub bodies and blade grip barrels classified as primary structural life-limited parts, traceability records maintained for certified component life or 10 years minimum per AS9100D Clause 8.5.2; electronic database accessible for OEM audit and airworthiness authority review.
AS9100D Quality System for
eVTOL Propeller Machining Programs
CNCPioneer's AS9100D quality management system — certified by Bureau Veritas — addresses the four quality dimensions specific to eVTOL propeller hub and blade grip components: C-axis single-setup blade bore angular pitch governance; 100% pitch bearing seat air gauge and CMM angular verification; TC4 hub body material traceability and fatigue process certification; and PPAP Level 3 / propeller wholesale supply chain qualification with SPC Cpk ≥ 1.67 on all special characteristics.
C-Axis Single-Setup Angular Pitch Governance
Blade bore inter-blade angular pitch ±0.010° is a structural guarantee — not the best result from indexing fixtures. CNCPioneer's MAZAK mill-turn C-axis single-setup programs command all blade bores in one continuous C-axis indexed program from one chucking — making angular pitch error a C-axis servo positioning accuracy outcome (±0.001–0.002°) rather than a fixture indexing-uncertainty outcome (±0.020–0.060°). Pitch bearing seat pair concentricity ±0.003mm is governed by the same principle: both seats bored from one spindle datum without rechucking. These structural accuracy guarantees extend through volume production without degradation — the ten-thousandth hub is as accurate as the first prototype.
- Blade bore angular pitch ±0.010° from C-axis servo positioning — not indexing fixtures
- Pitch bearing seat pair concentricity ±0.003mm from single spindle datum
- Angular and concentricity accuracy governed by machine — not setup uncertainty
100% Blade Bore Angular CMM & Mass Verification
Every eVTOL propeller hub receives 100% blade bore angular CMM verification (5-axis direct angular measurement between all blade bore axes; records per hub serial number before shipment). Every variable-pitch hub and blade grip receives 100% pitch bearing seat air gauge per bore and CMM roundness tester pair concentricity per blade station. Every hub and every blade grip receives 100% mass verification on calibrated precision balance (±0.1g resolution) with matched-set documentation. These 100% verifications — not sampling — eliminate the escape probability that sample-based inspection cannot eliminate when specification bandwidth is ±0.010° angular and ±1g mass.
- 100% blade bore angular CMM per hub serial number before shipment
- 100% pitch bearing seat air gauge per variable-pitch hub and blade grip
- 100% mass verification per component; matched-set documentation per hub assembly
TC4 Hub Body Fatigue Process Certification
TC4 propeller hub and blade grip fatigue certification chain: (1) UT per AMS 2154 Class A on incoming TC4 STA billet for manned flight programs; (2) SII XRF composition verification; (3) Hardness per lot confirming heat treat condition; (4) hub arm root fillet radius ±0.050mm verified by CMM optical probe at all arm stations; (5) shot peen AMS 2430 Almen A 0.18–0.22mm with 98% coverage per hub/grip serial number (pitch bearing seats and datum reference features masked); (6) dynamic balance G1.0 or G0.4 per hub; (7) AS9102 FAIR with all process certificates. Missing shot peen specification is the most common DFM finding (35% of initial TC4 hub designs) — CNCPioneer adds specification as a DFM finding and confirms shot peen record per hub in every FAIR package.
- UT per AMS 2154 Class A on incoming TC4 STA billet (manned eVTOL programs)
- Shot peen certificate per hub/grip serial number (Almen strip + coverage photos)
- Hub arm root fillet radius CMM optical probe ±0.010mm at all arm stations
eVTOL Propeller Wholesale PPAP & SPC
PPAP Level 3 for eVTOL propeller OEM supply chains: design records; process flow (C-axis single-setup sequence documentation); PFMEA (covering C-axis drift between blade bores, pitch bearing seat concentricity from single-setup, mass variation from material density variation, shot peen coverage failure modes); control plan; MSA Gage R&R on CMM angular measurement (≤10% of ±0.010° tolerance per CNCPioneer case study: 7.8% Gage R&R on blade bore pitch angle measurement); initial capability studies (Cpk ≥1.67 on blade bore angular pitch, pitch bearing seat diameter, hub center bore, and blade grip OD). Wholesale propeller programs: dedicated MAZAK VARIAXIS and mill-turn capacity; pre-purchased TC4 and 7075-T6 material stock 3–6 months forward; matched-set blade grip packaging; 2-week monthly blanket releases; safety stock 4–8 weeks.
- Cpk ≥1.67 on blade bore angular pitch, pitch bearing seat diameter, hub center bore
- MSA Gage R&R ≤10% on CMM angular measurement (demonstrated 7.8% in case study)
- Dedicated TC4 + 7075-T6 material stock; matched-set grip packaging; 2-week releases
eVTOL Propeller & Blade Grip Machining FAQ
Common questions from eVTOL aircraft manufacturers, variable-pitch propeller system OEMs, eVTOL rotor system developers, urban air mobility propulsion integrators, electric air taxi propulsion Tier 1 suppliers, and certification engineering partners about CNCPioneer's eVTOL propeller hub and blade grip machining capability, blade bore angular pitch accuracy, pitch bearing seat concentricity, hub centrifugal stress engineering, and eVTOL propeller wholesale economics.
The requirement for single-setup turn-mill machining of eVTOL propeller hub blade bores is a consequence of angular pitch error accumulation from C-axis re-indexing between setups — the dominant error mechanism that degrades inter-blade pitch accuracy in conventional multi-setup propeller hub machining. In a multi-setup approach, the hub is machined in a MAZAK mill-turn for blade bore 1, then physically repositioned on an indexing fixture rotated 120° for blade bore 2, then again for blade bore 3. Each fixture repositioning introduces angular error from three sources: (1) indexing fixture dividing head backlash and positioning uncertainty, typically ±0.010–0.025° for commercial indexing heads; (2) hub seating repeatability on fixture — non-flat hub reference surfaces seat inconsistently producing ±0.005–0.015° angular error; (3) fixture thermal drift between first and third bore across 30+ minutes of machining. Cumulative angular error: 3 × (±0.010° + ±0.005° + ±0.003°) = ±0.054° worst-case. For a 3-blade eVTOL propeller at 2,000 RPM (33.3 Hz), ±0.054° angular pitch error produces blade-to-blade thrust imbalance: ΔT/T = 2 × sin(Δθ/2) ≈ Δθ_radians = 0.054 × π/180 = 0.00094 → 0.094% thrust imbalance. Lateral vibration force: 1,600 kg × 0.00094 × 9.81 = 14.8 N at 33.3 Hz — perceptible to seated passengers (threshold ~10–15 N at this frequency). CNCPioneer's C-axis servo positioning accuracy ±0.001° per commanded position produces ±0.002° inter-blade angular error. At ±0.002°: lateral force = 1,600 × (0.002 × π/180) × 9.81 = 0.55 N — below any passenger vibration perception threshold. This quantitative comparison demonstrates why single-setup C-axis indexed turn-mill machining is a technical requirement, not a preference.
Variable-pitch propeller blade grips require pitch bearing seat pair concentricity ±0.003mm because this specification directly determines three critical operational characteristics. First, pitch axis running accuracy: if bearing seats are eccentric by δ = 0.010mm over bearing center distance L = 95mm, the pitch axis is tilted by tan(θ) = 0.010/95 = 0.000105 rad = 0.006°. This 0.006° pitch axis tilt means the blade traces a cone during pitch change rather than pure rotation. The resulting pitch angle error: Δpitch = 0.006° × sin(30°) = 0.003° for a 30° collective pitch change — accumulating with pitch horn angular position error (±0.010°) and pitch linkage variation (±0.100mm) to potentially exceed the ±0.020° total pitch angle accuracy that variable-pitch eVTOL flight control systems specify. Second, pitch bearing preload: bearing seat eccentricity imposes a bending moment on the blade grip barrel proportional to eccentricity × bearing lateral stiffness. At 0.010mm eccentricity: bending moment = 0.010mm × 50,000 N/mm = 500 N·m — substantial moment added to the centrifugal and aerodynamic loads the blade grip already carries, reducing fatigue margin. At CNCPioneer's ±0.003mm concentricity: imposed bending moment = 150 N·m — 70% lower, maintaining structural fatigue margin within design budget. Third, machining achievability: ±0.003mm concentricity between two bearing seats separated by 95mm axial distance is achievable in MAZAK mill-turn single-setup machining (both seats bored without rechucking from same spindle datum, machine positioning accuracy ±0.001mm) but is not achievable by rechucking between two lathe operations (rechucking introduces ±0.012–0.018mm eccentricity per rechuck). CNCPioneer's pitch bearing seat ±0.003mm concentricity is the single most distinctive machining capability in the eVTOL blade grip program portfolio.
CNCPioneer's 48-hour eVTOL propeller hub DFM review covers six engineering analysis areas, each producing a specific actionable finding or approval. First, centrifugal stress check at hub arm root: from blade mass, operating RPM, and hub arm root cross-sectional area — calculates CF stress × stress concentration from arm root fillet radius; compares to material allowable × safety factor (1.5 manned / 1.2 cargo drone). Finding: adequate → approved; marginal → recommend radius increase or material upgrade with engineering calculation; failing → mandatory design change before machining commitment. Second, pitch bearing seat machining feasibility: confirms both seats accessible to MAZAK boring bar tooling from single chucking without tool interference with hub arms; calculates required boring bar reach/diameter ratio. Third, blade bore angular pitch program verification: confirms C-axis can index correctly between blade bores with adequate chip clearance for the drill-ream cycle between C-axis positions; flags any hub arm geometry that might shadow the drill path at adjacent blade bore positions. Fourth, pitch horn angular achievability: calculates 5-axis tool path collision check against hub body geometry at all tool orientations. Fifth, hub mass vs target: estimates machined mass from CAD solid; compares to design target; flags >5% excess before machining. Sixth, surface treatment specification completeness. Most frequently identified issues: (1) Missing shot peen specification on TC4 hub bodies — 35% of initial designs; (2) Pitch bearing seat concentricity specified at ±0.005mm but without single-setup note — multi-setup machining cannot achieve this; (3) Hub arm root fillet radius R0.5mm (as-designed) produces Kf = 2.1 in TC4 — fatigue stress exceeds material endurance limit at 10,000-hour life; CNCPioneer recommends R2.0–3.0mm minimum at hub arm root for TC4 hub bodies.
Lead times at CNCPioneer's eVTOL propeller machining facility: 7075-T6 fixed-pitch 3-blade hub (Ø280–380mm, turn-mill, anodize, FAIR) — 8–11 business days; 7075-T6 fixed-pitch 4–6 blade hub (larger OD, 5-axis, FAIR) — 10–14 days; TC4 AMS 4928 variable-pitch 3-blade hub body (pitch bearing seats, pitch mechanism features, FAIR) — 12–16 days; TC4 AMS 6931 STA variable-pitch hub (manned class, shot peen, FAIR) — 14–18 days; matched TC4 blade grip set of 3 (Swiss CNC or mill-turn, mass-matched, FAIR) — 9–13 days; TC4 pitch horn set of 3 (angular-position-matched, FAIR) — 6–9 days; 7075-T6 collective pitch spider (5-axis, FAIR) — 7–10 days; complete variable-pitch propeller machined kit (hub + grips + horns + spider) — 16–22 days. Volume economics: prototype 3-blade fixed-pitch hub ~$680; pilot production (300–1,000 hubs/year) ~$390–$580; production (1,000–5,000/year) ~$290–$420; large volume (5,000–20,000/year) ~$195–$290. Variable-pitch complete kit: prototype ~$3,200; production (1,000–5,000 kits/year) ~$1,100–$1,650. At 2,000 aircraft/year (8,000 variable-pitch hub kits/year) at $1,100–$1,650 per kit: CNCPioneer's pricing falls within the commercial air taxi propeller kit cost target of $1,500–$2,500 per assembly — the 40–60% cost advantage versus US/European specialist rotorcraft machining facilities that price equivalent kits at $2,800–$4,500.
CNCPioneer's eVTOL propeller wholesale supply programs provide six infrastructure capabilities that standard CNC machining facilities do not offer: (1) Dedicated MAZAK VARIAXIS and mill-turn capacity: named machines block-allocated per propeller hub and blade grip programs; monthly release quantities from dedicated machines without queue competition from other programs. (2) Pre-purchased TC4 and 7075-T6 aerospace alloy stock: 3–6 months forward position; eliminates material lead time from monthly releases and protects against aerospace alloy market disruption. (3) Matched-set blade grip packaging: all grips for each hub packaged as pre-verified matched mass sets (within ±1.5g total spread); eliminates blade grip re-sorting at propeller assembly and documents matched-set compliance before shipment. (4) 100% angular pitch CMM per hub and 100% pitch bearing seat air gauge per variable-pitch component — not sampled — with records per serial number before shipment. (5) Safety stock buffer: 4–8 weeks finished goods for highest-velocity propeller component part numbers — enabling same-week emergency pull for aircraft final assembly schedules. (6) AS9100D life-limited part records: traceability from billet heat number to hub or blade grip serial number maintained for certified component life or 10 years minimum per AS9100D Clause 8.5.2, accessible for OEM audit and airworthiness authority review.
Get a Quote for eVTOL Propeller & Blade Grip Turn-Mill Machining
Upload your eVTOL propeller hub drawings, blade grip CAD models, rotor head specifications, or variable-pitch propeller system layout and receive a competitive quotation within 24 hours and a complete engineering DFM review within 48 hours — covering inter-blade angular pitch achievability from turn-mill single-setup C-axis program, pitch bearing seat concentricity chain from MAZAK mill-turn single-setup approach, hub arm root centrifugal stress adequacy check against TC4 AMS 4928 vs AMS 6931 STA material allowables and life requirement, pitch horn angular position feasibility from 5-axis reference datum, shot peen specification adequacy for TC4 life-limited classification, mass achievability against design CAD model target, AS9102 FAIR scope and timeline for your eVTOL certification program, and complete component kit pricing from prototype first articles through pilot production qualification and AS9100D-governed wholesale supply.