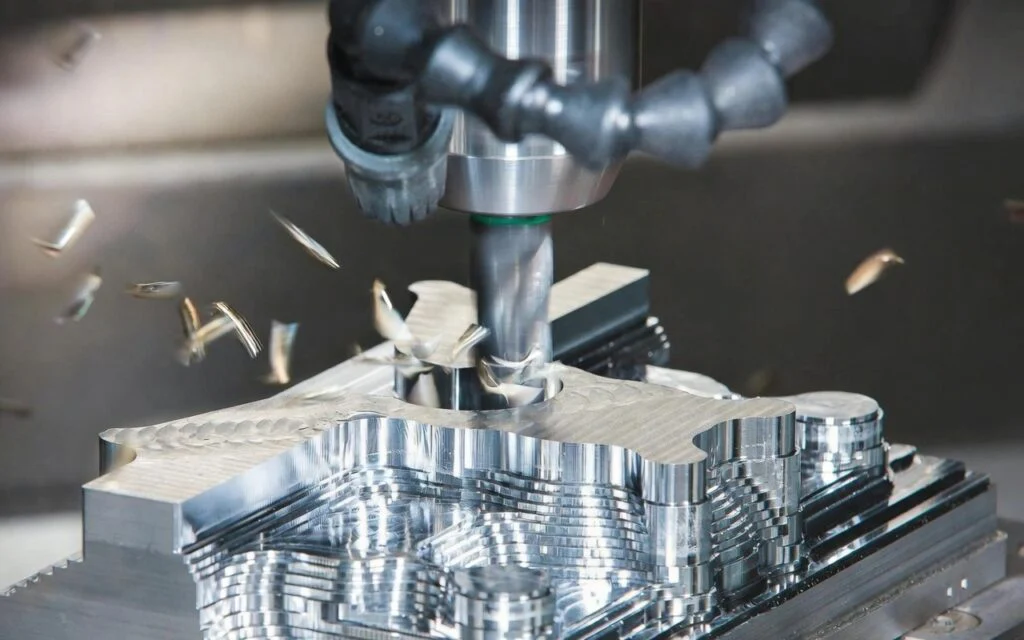
CNC machining and manual machining remove material using many of the same cutting principles. The main difference is how machine motion is controlled. CNC follows a verified program; on conventional manual equipment, the operator directly controls much of the motion and sequence.
Here, “conventional machining” means manually controlled milling and turning. The practical choice depends on the job: an urgent one-off adjustment, a development part, and a repeat batch can justify different routes.
What Changes Between CNC and Manual Machining?
A manual machinist plans the sequence, sets the work, selects tools, and controls the cut using the machine's handwheels and available power feeds. A digital readout can assist positioning without turning the machine into a CNC system. The operator's skill and attention strongly influence the result.
With CNC, the geometry and sequence are represented in a program. The operator still sets up stock, workholding, offsets, tooling, and inspection. After prove-out, the program can repeat movements and coordinate several axes more consistently than repeated manual positioning.
Neither method guarantees the drawing requirements merely by its name. Machine condition, workholding, tooling, material stability, and inspection determine whether a part is acceptable. A capable manual shop may produce a good one-off part; a poorly controlled CNC process may produce a repeatable error.
CNC vs Manual Machining: Practical Comparison
| Decision factor | CNC | Manual / conventional |
|---|---|---|
| Preparation | Programming, setup, and prove-out before repetition | Can start simple operations with less programming effort |
| Complex geometry | Coordinated paths support contours and repeated feature patterns | Complex features may require more operations or dedicated tooling |
| Repeat batches | Established programs reduce repeated positioning work | More operator time and repeated measurement may be needed |
| One-off changes | Program and setup changes may outweigh cutting time | Direct adjustment can be practical for accessible, simple features |
| Quality | Needs tool control, offset management, and inspection | Needs operator control, sound setup, and inspection |
| Capacity | Automation may reduce intervention on suitable jobs | Typically requires closer operator involvement during machining |
Compare Total Job Cost, Not Just Hourly Rate
A useful estimate separates preparation from repetition: total cost includes material, programming, setup, machining time, tooling, finishing, inspection, and handling. The cost per part changes when preparation is spread across more accepted pieces.
For CNC, a higher initial setup cost can be justified by lower repeated cutting and handling effort. For a simple one-off modification, programming may add little value. There is no universal quantity at which CNC becomes cheaper: geometry, available fixtures, operator experience, inspection needs, and whether the job will repeat all affect the crossover.
Compare quotations with the same scope. Check whether deburring, material certification, surface treatment, and inspection are included. An apparently inexpensive part can become costly if it needs extra machining or fails assembly. The CNC machining cost guide explains the main quotation inputs.
When Manual Machining Remains Useful
Manual equipment can be appropriate for a straightforward repair, an accessible shaft adjustment, a fixture modification, or an exploratory cut while dimensions are being established. It can also support work that would be awkward to schedule on a production CNC cell.
Before choosing it, define the required features and how they will be measured. A repair may involve an existing worn surface rather than ideal CAD geometry, so inspection and workholding can matter more than machine speed. Manual work should not be treated as automatically low precision or automatically cheaper.
When CNC Is the Better Starting Point
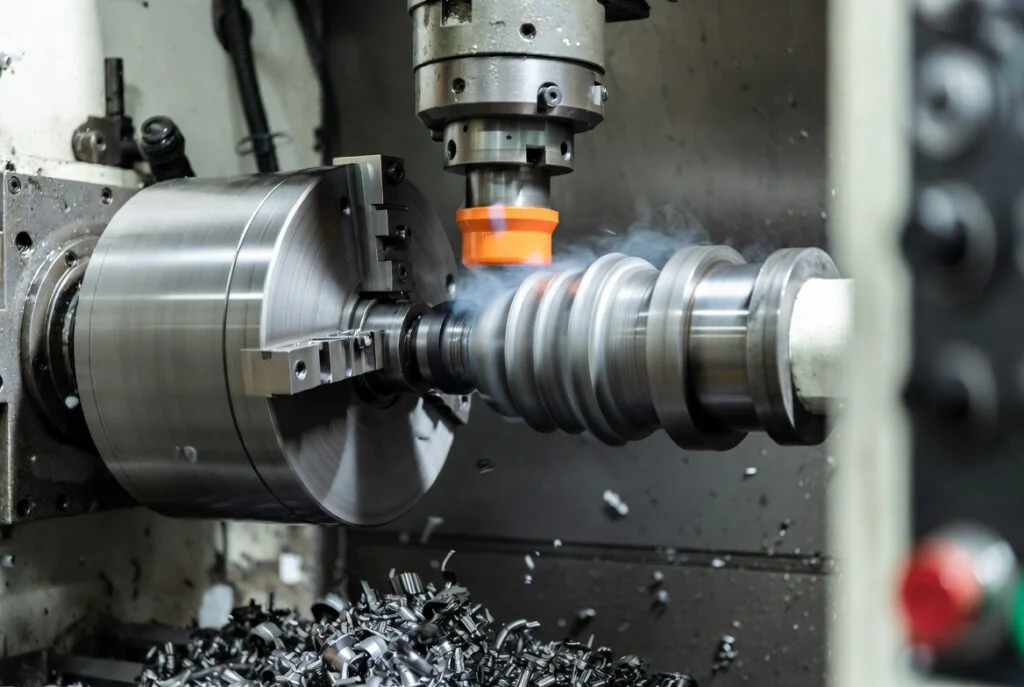
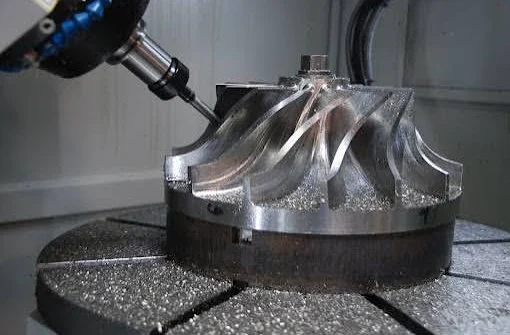
CNC is a strong candidate for repeated hole patterns, multiple identical parts, complex contours, and jobs that benefit from a stored, controlled process. It can also suit a single prototype when the geometry would be difficult to create manually.
Choose the specific process after reviewing the part. Turning suits many rotational features; milling addresses pockets, faces, and other tool-accessible geometry. Use the turning and milling comparison to refine that choice. For repeated orders, preserve the drawing revision, setup information, and inspection requirements rather than relying only on the program file.
A Short Decision Checklist
- Is the geometry stable, or will it change after every trial?
- How many parts are required now, and is repeat production likely?
- Which features control assembly and require documented inspection?
- Can the work be held and reached efficiently on the available equipment?
- What does the complete accepted batch cost, including finishing and inspection?
A hybrid route can be sensible: CNC may produce the repeated geometry while another operation handles a simple adjustment or finishing task. If outsourcing, evaluate the supplier's proposed process and quality controls rather than buying a machine category. See the supplier evaluation checklist, then send the drawing and batch requirements for review.
For repeat orders of parts with turned and milled features, review our CNC turning and milling service with the part drawing, material, quantity, and inspection requirements.
For a component example, review the drawing requirements for custom turning and milling parts.