
Brass
Pneumatic Fittings
CNCPioneer is an IATF 16949 certified China brass pneumatic fittings manufacturer delivering complete OEM and wholesale push-fit programs in C36000, DZR CW602N, and H59 brass — push-fit straight unions, elbows, tees, reducers, bulkheads, manifold blocks, and thread-to-push-fit fittings at collet groove OD ±0.010mm, 100% air pressure leak test per fitting, 100% BSP/NPT gauge per fitting, and PPAP Level 3 since 2011. From prototype 3-day first articles to 10,000,000+ unit annual wholesale supply.

What Are Brass
Pneumatic Fittings?
Brass pneumatic fittings are precision CNC turned and milled metallic connection components — manufactured from C36000 free-machining brass, DZR CW602N dezincification-resistant brass, or H59 Chinese-standard brass on 78+ Swiss CNC lathes with guide bushing and 66+ MAZAK mill-turn centers with C-axis live tooling — that connect, route, distribute, adapt, and seal compressed air and inert gas flow within pneumatic circuits by mechanically joining pneumatic tubing to pneumatic components through push-fit collet mechanisms, threaded body connections, or compression cone tube end joints.
Brass is the universal material for pneumatic fittings across the complete industrial spectrum — from desktop laboratory equipment to industrial robot tooling to automotive assembly line tooling — from the combination of properties that no alternative material simultaneously provides at comparable cost: C36000 free-machining brass at 100% machinability index enables Swiss CNC production at 5,000–20,000 small pneumatic fitting bodies per machine-hour, producing the wholesale unit economics that make brass pneumatic fittings commercially viable at the tens of millions of annual units consumed by global automation, robotics, and machine tool programs.
-
Collet groove OD ±0.010mm — the push-fit performance foundationThe collet groove OD determines the collet's radial pre-load against the inserted pneumatic tube OD. Too large → tube pull-out below ISO 15218 minimum (50N for Ø6mm tube at PN10). Too small → insertion force exceeds ergonomic limit for automated assembly. CNCPioneer's Swiss CNC guide bushing achieves ±0.010mm — the only process that simultaneously ensures ≥50N pull-out and ≤80N insertion force.
-
100% air pressure leak test per fitting — non-negotiable production standardCNCPioneer's 100% individual pressure test (1.5× rated working pressure; 15 bar for PN10 programs; 30-second hold; zero bubble tolerance; records per serial number) provides the individual fitting quality gate that lot-based sample testing misses for the 0.2–0.5% defective fitting rate typical in high-volume brass push-fit production. Standard on all sealed pneumatic fitting programs at no additional charge.
-
Single-setup MAZAK mill-turn — port angular position ±0.020° for multi-port fittingsMulti-port fittings (tee, cross, manifold, elbow) require C-axis milling for lateral port bores. MAZAK mill-turn C-axis produces port-to-port angular position ±0.020°, port perpendicularity 0.010mm — ensuring parallel tube routing in panel-mounted pneumatic circuits and conforming 90° elbow geometry for automated robot tube connections.
-
40–60% China cost advantage at IATF 16949 quality and 100% test standardEquivalent brass pneumatic fittings from European or North American specialists cost 40–60% more per fitting than CNCPioneer's IATF 16949-equivalent programs. Case study: €0.195/fitting versus previous German supplier at €0.42/fitting — €103,680 annual saving per robot model at 460,800 fittings/year, €518,400 across a 5-model line.

Why CNCPioneer for Brass
Pneumatic Fittings?
Among China brass pneumatic fittings manufacturers globally, CNCPioneer's Swiss CNC guide bushing collet groove precision, 100% air pressure leak test standard, MAZAK mill-turn C-axis multi-port accuracy, complete tube size and thread standard coverage, food-grade DZR compliance, and IATF 16949 PPAP Level 3 quality system establish our factory as the preferred OEM and wholesale pneumatic brass fitting supplier to automation equipment, robot, automotive, and food processing industries worldwide.
Push-Fit Collet Groove OD ±0.010mm — Swiss CNC Performance Foundation
The collet groove OD is the single most critical precision dimension in a push-fit fitting — directly determining the collet's radial pre-load against the inserted pneumatic tube and hence the tube retention force. Collet groove OD too large by +0.030mm → pull-out force falls from 50N to 37N for Ø6mm tube — below ISO 15218 minimum, producing tube ejection at rated pressure. Too small by −0.030mm → insertion force exceeds 80N ergonomic limit → automated assembly line reject. CNCPioneer's 78+ Swiss CNC lathes with guide bushing support the fitting body at the cutting point, producing collet groove OD ±0.010mm simultaneously with tube insertion bore ±0.020mm and BSP thread pitch diameter ±0.005mm from one bar-feed program — the only platform achieving all three simultaneously without re-chucking.
Swiss CNC Guide Bushing — Small Pneumatic Fitting Body Precision
The majority of standard push-fit pneumatic brass fittings fall within the Ø8–25mm body OD range. A Ø12mm × 30mm (L/D = 2.5:1) brass push-fit fitting body turned in a standard chuck lathe deflects 0.015–0.035mm at the push-fit port bore from the insert's radial cutting force — immediately exceeding the ±0.010mm collet groove OD specification before any other process variation is added. CNCPioneer's 78+ Swiss CNC lathes with guide bushing support the fitting body at the cutting point throughout all turning, boring, and threading operations — producing the ±0.010mm collet groove OD, ±0.020mm tube insertion bore, and ±0.005mm BSP thread pitch diameter simultaneously from one bar-feed program without re-chucking and without deflection-induced OD error.
Single-Setup MAZAK Mill-Turn for Multi-Port Fittings
Multi-port pneumatic brass fittings — tee bodies (three push-fit ports), cross bodies (four ports), manifold blocks (4–8 ports), and elbow bodies (two ports at 90° or 45°) — require C-axis milling operations for lateral port bores. Single-setup MAZAK mill-turn C-axis produces all port bores from the same spindle datum: port-to-port angular position ±0.020°; port perpendicularity to body axis 0.010mm; inter-port position ±0.020mm. For pneumatic tee and cross fittings where the branch port must be perpendicular to the inline ports within ±0.020° for parallel tube routing in panel-mounted circuits, this single-setup accuracy eliminates the angular offset that multi-machine sequential programs produce — causing branching tubes to route non-parallel and creating appearance failures and mechanical strain on automated robot installations.
100% Air Pressure Leak Test per Fitting — Non-Negotiable Standard
A 0.5mm leak path at 6 bar wastes approximately 25 litres/minute of compressed air — costing $180–360/year per leak in compressed air energy at typical factory rates. In automotive robot programs, a defective fitting can produce unexpected loss of clamping force on automated assembly fixtures — a safety incident. Cost of 100% pressure testing at CNCPioneer: $0.01–0.04/fitting. Cost of a single escaped defective fitting in an automotive robot program: $240,000–$750,000 production loss (30 minutes downtime at $8,000–$25,000/minute). CNCPioneer applies 100% individual air pressure leak test (1.5× PN rated / 30s / zero bubble / per fitting serial number) as a production standard — not a sample audit — on all sealed brass pneumatic fitting programs.
Complete Tube Size & Thread Standard Coverage from One OEM Source
OEM pneumatic circuit programs for automated manufacturing equipment, robots, and machine tools require fittings in multiple tube sizes (4mm, 6mm, 8mm, 10mm metric; ¼", 3/8" imperial) and multiple thread body standards (G1/8, G1/4, G3/8 BSP for European programs; 1/8 NPT, ¼ NPT, 3/8 NPT for North American). CNCPioneer's single-source capability covers all standard tube OD sizes (4mm through 16mm metric; 5/32" through ½" imperial), all standard thread body sizes (G1/8 through G1/2 BSP; 1/8 NPT through ½ NPT), and all standard fitting types (straight union, elbow, tee, reducer, bulkhead, manifold) from one IATF 16949 certified quality system — eliminating multi-supplier management complexity across the pneumatic fitting BOM.
DZR Food-Grade Compliance & 40–60% China Cost Advantage
Pneumatic circuits in food processing, packaging, pharmaceutical, and beverage equipment require fittings compliant with EC 1935/2004 food contact material regulations. DZR CW602N brass (As 0.02–0.06% SII XRF per lot; WRAS-compliant; EN 12164) and WRAS-compliant nickel-plated C36000 are CNCPioneer's standard food-grade pneumatic brass fitting materials — the material compliance food equipment OEMs require from pneumatic fitting supply chains. Equivalent fittings from European or North American specialists cost 40–60% more per fitting. Case study: €0.195/fitting (CNCPioneer IATF 16949 + 100% test) versus €0.42/fitting (German supplier) — €103,680 annual saving per robot model.
Brass Pneumatic Fittings —
Complete Product Portfolio
CNCPioneer's brass pneumatic fitting programs span the complete fitting type, tube size, and thread standard portfolio — push-fit straight unions, 90°/45° elbows, tees, crosses, Y-fittings, reducers, bulkheads, thread-to-push-fit adapters in all BSP/NPT/metric sizes, manifold blocks with 2–8 outlets, speed controller fittings with metering orifice, and compression tube-to-fitting programs for rigid brass tube — all from one IATF 16949 certified source with 100% pressure test per fitting.
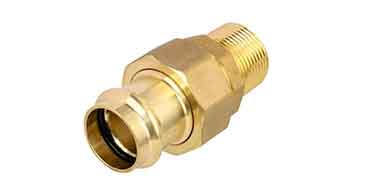
Push-Fit Straight Union & Reducer Fittings
The highest-volume pneumatic push-fit fitting type — two push-fit ports coaxial on the same body axis, joining two lengths of pneumatic tubing inline. C36000 bar; SII XRF per lot; Swiss CNC guide bushing; body OD ±0.010mm. Both push-fit ports: collet groove OD ±0.010mm per port; tube insertion bore ±0.020mm; O-ring groove depth ±0.010mm; width ±0.020mm; NBR O-ring Ø1.78mm (4–8mm tube) or Ø2.62mm (10–16mm tube) pre-assembled. Through-bore flow bore. 100% air pressure leak test: 15 bar / 30-second water immersion or soap bubble / zero leak / records per fitting serial number. Reducer unions (Ø10mm × Ø8mm; Ø8mm × Ø6mm; all tube OD combinations): asymmetric body with large-port and small-port collet grooves both ±0.010mm; stepped through-bore with smooth chamfer transition. Extended hex union bodies for panel-installation programs: C-axis milled hex ±0.100mm across-flats for wrench engagement in tight panel installations.
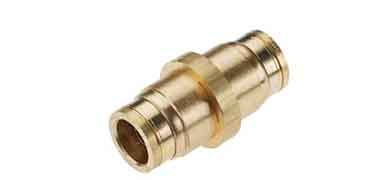
Push-Fit Elbow Fittings (90°, 45°, Swivel)
The second highest-volume pneumatic fitting type — routing pneumatic tubing through a 90° or 45° direction change without tube bending. Single-setup MAZAK mill-turn: primary push-fit port from spindle axis; secondary push-fit port from C-axis live boring at 90° or 45°; port perpendicularity 0.010mm from C-axis index accuracy. For automated robot installations where pneumatic tubes are pre-cut to exact lengths and pre-routed through robot arm cable management, port-to-port angular accuracy ±0.020° prevents tube end displacement (±sin(0.5°) × 300mm tube = ±2.6mm — exceeding typical ±1.5mm automated connection tolerance). 45° elbow from VARIAXIS 5-axis or C-axis 45° index; ±0.020° from B-axis or C-axis positioning. Swivel elbow: rotating swivel ring with smooth bore engagement; rotary O-ring seal between swivel and body; snap-ring groove retention ±0.020mm width. All types: 100% pressure test; collet groove ±0.010mm per port; bright nickel plate standard option.
Push-Fit Tee, Cross & Y-Fittings
Tee (three push-fit ports, T-configuration): two inline ports from turning axis coaxial ±0.010mm; branch port from MAZAK mill-turn C-axis at 90° perpendicularity ±0.010mm; all three collet grooves ±0.010mm OD; O-ring grooves ±0.010mm depth; 100% pressure test all three ports simultaneously. Reducing tee: inline Ø10mm collet groove ±0.010mm; branch Ø8mm collet groove ±0.010mm from C-axis live boring at reduced bore; stepped internal passage with smooth chamfer transition. Cross (4-port, 90° branch pairs): two inline ports from turning axis; two branch ports from C-axis indexed at 90° and 270°; inter-port angular positions 90° ±0.020° from C-axis absolute datum; 100% pressure test. Y-fitting (three ports at 120° for balanced 3-way distribution): MAZAK mill-turn C-axis at 120° spacing ±0.020°; shorter body than T-fitting for compact installation; applications: 3-cylinder balance grippers, tri-directional pneumatic support fixtures.
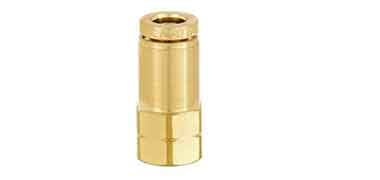
Thread-to-Push-Fit Fittings (BSP, NPT, Metric)
Connection point between pneumatic components with threaded ports and the pneumatic tubing circuit — the most structurally critical fitting type because they directly attach to pneumatic actuators. Male BSP × push-fit: G1/4 BSP parallel male thread ISO 228 Class A; single-point CNC threading; pitch diameter ±0.005mm; 100% ring gauge per fitting; hex shoulder for installation torque; shoulder face flatness 0.010mm/25mm for bonded seal or Dowty washer seating; push-fit end collet groove ±0.010mm; O-ring groove ±0.010mm depth; thread-to-push-fit body axis coaxiality ±0.010mm from single Swiss CNC setup. Female BSP × push-fit: BSP female internal thread; 100% plug gauge; hex body. NPT male × push-fit: ¼-18 NPT male; 100% L1 taper ring gauge; single-point CNC threading for stainless; CNC die head for brass NPT. Metric M5×0.8 × Ø4mm push-fit: for SMC, Festo M5-port cylinders; Swiss CNC single-point threading ±0.005mm; 100% ring gauge; fitting body OD Ø9mm × 18mm. L-shaped (90° elbow) thread-to-push-fit: MAZAK mill-turn C-axis; thread-to-push-fit axis perpendicularity ±0.020°; replaces two separate components in single body.
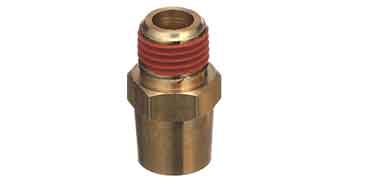
Pneumatic Manifold Block Fittings (2–8 Ports)
Single precision-machined brass bodies distributing one compressed air inlet to 2, 4, 6, or 8 push-fit tube outlet ports — for pneumatic circuits serving multiple parallel actuators from one supply point. 4-port manifold (G1/4 BSP inlet × 4× Ø8mm push-fit outlets): MAZAK mill-turn central inlet port → four outlet push-fit ports C-axis indexed at 0°, 90°, 180°, 270°; inter-outlet angular position ±0.020° from C-axis absolute datum — ensuring equal tube length and routing geometry for equal flow distribution to parallel cylinders; each push-fit outlet collet groove ±0.010mm; O-ring groove ±0.010mm; NBR O-ring pre-assembled; central distribution bore Ø8mm flowing to each outlet bore; end ports plugged with brass hex plug; 100% pressure test all outlets simultaneously. 2-port block format with flat mounting face for panel mounting, tapped mounting holes C-axis drilled ±0.050mm. 8-port manifold for automotive assembly fixture programs (6–8 pneumatic clamps from one manifold): C-axis indexed at 45° spacing ±0.020°; G3/8 BSP inlet for adequate flow at full 8-cylinder simultaneous actuation.
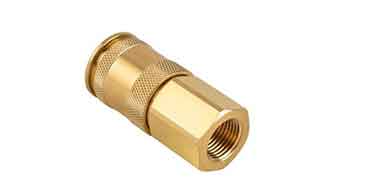
Specialty Fittings (Bulkhead, Speed Controller, Compression, Flare)
Bulkhead fitting: push-fit port on each face of the panel; body OD machined for panel bore clearance ±0.100mm; hex lock nut with panel contact face ±0.050mm; body length accommodating panel thickness with thread projection; both push-fit ports collet groove ±0.010mm; 100% pressure test. Speed controller with metering orifice: Ø0.5mm–Ø4.0mm ±0.010mm metering orifice from Swiss CNC precision boring — providing ±1% flow control accuracy for cylinder actuation speed control (versus ±4% from ±0.050mm orifice); same push-fit collet geometry as standard fitting. Compression-type to brass tubing (DIN 2353 24° cone): for rigid brass tube pneumatic circuits (CNC machine tool lubrication air circuits, compressor outlet mains); brass olive pre-assembled; DIN 2353 thread per tube OD; 100% ring gauge. Flare-type to brass tubing (SAE 45° cone): for North American HVAC and refrigeration pneumatic circuits; 45° half-angle female flare seat ±0.5°; UNF nut per SAE J512; 100% ring gauge.
Industries & Applications
CNCPioneer's brass pneumatic fitting programs serve every industry consuming precision push-fit and thread-body pneumatic fittings at IATF 16949 quality and 100% pressure test standard — from industrial automation and robot assembly equipment through automotive factory pneumatic systems, food processing and packaging equipment, machine tools, construction equipment, commercial vehicles, medical device laboratories, and global wholesale pneumatic fitting distributors requiring 10,000,000+ annual units.

Semiconductor
C36000 and nickel-plated brass push-fit and thread-body pneumatic fittings for semiconductor equipment OEM assembly programs — wafer handling robot arm pneumatic circuits, CVD/ALD process chamber pneumatic actuator supply lines, lithography automated stage pneumatic feeds, and dry vacuum pump pneumatic manifolds. IATF 16949 PPAP Level 3; SPC Cpk ≥1.67 collet groove OD and thread form; 100% pressure test per fitting; 100% post-plate collet groove go-gauge per fitting. Complete BSP / NPT / metric thread body matrix available; blanket order programs with monthly kanban; free First Article samples for new program qualification; annual supply from 50,000 to 2,000,000+ fittings.
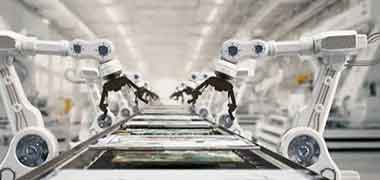
Robots
Complete OEM brass pneumatic fitting programs for industrial welding robot arm pneumatic circuits (FANUC, ABB, KUKA, Yaskawa), collaborative robot end-effector tooling air supply, pick-and-place automation gripper circuits, and automated assembly machine air distribution manifolds. IATF 16949 PPAP Level 3; SPC Cpk ≥1.67 collet groove OD; 100% pressure test per fitting; 100% BSP/NPT gauge per fitting; 100% post-plate collet groove go-gauge; weekly kanban delivery to robot OEM assembly lines. Validated case study: 460,800 fittings/year for Japanese welding robot OEM at €0.195/fitting versus previous German supplier at €0.42/fitting — €103,680 annual saving with superior 100% post-plate pressure test quality versus 5% sample-tested equivalent.
Aerospace
C36000 and DZR brass push-fit and thread-body pneumatic fittings for aerospace manufacturing floor pneumatic tooling — rivet gun air supply manifolds, pneumatic drill and countersink tool feed circuits, wing jig and fuselage fixture pneumatic clamp actuator supply lines, and MRO hangar compressed air distribution drops. Natural brass and zinc-nickel plated options for corrosion resistance in outdoor MRO environments; 100% pressure test per fitting; 100% BSP/NPT thread gauge per fitting. AS9100D supply chain documentation support on request; full lot traceability records; material certifications to AMS or ASTM on request; annual supply programs from 20,000 to 500,000+ fittings with custom OEM-PN part marking for MRO traceability.
Medical
DZR CW602N brass and 316L stainless push-fit and thread-body pneumatic fittings for medical device manufacturing equipment pneumatic circuits, hospital piped medical gas distribution manifolds (O₂, N₂, CO₂, Ar, vacuum), dental equipment compressor feed circuits, and ISO Class 5/6 cleanroom laboratory automation systems. 316L stainless option: ASTM A967 passivation; VSM μ_r ≤1.005 non-magnetic certification for MRI-adjacent gas panel installations; HEPA-compatible surface finish. Full material traceability; biocompatibility documentation on request; RoHS and REACH compliance certificates supplied. NPT, BSP, and metric thread bodies for global medical OEM programs; 100% pressure test per fitting; annual supply from 10,000 to 1,000,000+ units.
Automotive
IATF 16949-certified C36000 and DZR brass pneumatic fittings for automotive body shop welding fixture pneumatic clamp circuits, transfer press die pneumatic actuator supply lines, paint shop spray booth pneumatic tooling, sunroof and glass assembly machine air circuits, and engine assembly line torque tool air supply manifolds. PPAP Level 3 with dimensional balloon report; SPC Cpk ≥1.67 on collet groove OD, thread form, and body OD; 100% post-plate pressure test per fitting; zinc-nickel or nickel plating per OEM specification. Weekly kanban delivery to assembly lines; bar-coded OEM-PN traceability packaging; 4-week rolling call-off blanket orders; annual supply from 100,000 to 5,000,000+ fittings.
Food Processing
DZR CW602N (As 0.02–0.06%; SII XRF mandatory per lot; WRAS-approved; EC 1935/2004 food contact compliant) and nickel-plated C36000 brass pneumatic fittings for food packaging machinery, beverage can and bottle filling lines, bakery and confectionery automated packaging equipment, dairy and brewing process plant pneumatic circuits, and pharmaceutical cleanroom assembly machine air supply. Bright nickel or satin Ni+PTFE composite plating for hygienic washdown-compatible surface finish; 100% pressure test per fitting; full food contact material compliance documentation (EC 1935/2004, FDA 21 CFR §175–177, LFGB on request). 100% SII XRF arsenic verification per lot with certificate; WRAS approval certificate supplied; annual supply from 10,000 to 10,000,000+ units.
Brass Pneumatic Fittings —
Technical Capabilities
CNCPioneer's brass pneumatic fitting technical capability combines Swiss CNC guide bushing collet groove precision (±0.010mm), MAZAK mill-turn C-axis multi-port accuracy (±0.020°), 100% individual air pressure leak test, 100% BSP/NPT thread gauge, 100% post-plate collet groove go-gauge, and complete IATF 16949 PPAP Level 3 documentation — delivering brass pneumatic fitting programs from 3-day prototype through 10,000,000+ unit annual OEM and wholesale supply.
Swiss CNC + MAZAK Mill-Turn Two-Platform Architecture
78+ Swiss CNC lathes with guide bushing for standard push-fit straight union, reducer, and thread-body fitting bodies (Ø6–25mm; collet groove OD ±0.010mm; tube insertion bore ±0.020mm; BSP thread pitch diameter ±0.005mm; 5,000–20,000 C36000 fittings/machine/hour bar-feed automated). 66+ MAZAK mill-turn centers with full C-axis and driven tooling for multi-port pneumatic manifold fitting bodies, elbow bodies (port perpendicularity ±0.010mm from C-axis), tee and cross bodies (port angular position ±0.020°), and thread-to-push-fit elbow bodies — all features from single-setup one spindle datum. O-ring groove depth ±0.010mm and width ±0.020mm from single-setup MAZAK mill-turn boring — the precision governing O-ring compression ratio (target 15–25%) for leak-free seal across all operating pressures.
SII XRF per C36000/DZR/H59 Lot — Grade-Specific Compliance
SII XRF composition confirmation on every brass bar lot before machining: C36000 (Cu 60–63%; Pb 2.5–3.7% confirmed per lot); DZR CW602N (As 0.02–0.06% MANDATORY per lot — the dezincification inhibitor content governing WRAS compliance and EC 1935/2004 food contact material approval); H59 CuZn40 (Cu 57–60% per lot). 316L stainless push-fit fittings: SII XRF C ≤0.030%; Mo 2–3%; Cr 16–18% per lot. EN 10204 3.1 or material test report archived per lot; lot traceability from bar certificate to production lot to delivery documentation and PPAP Level 3 PSW. 3-month C36000 and DZR bar safety stock SII XRF pre-verified; NBR/EPDM/FKM O-ring and stainless steel collet inventory pre-stocked by fitting size for OEM program continuity.
Collet Groove OD ±0.010mm + 100% Go-Gauge per Fitting
Collet groove OD calculations: target groove OD = collet natural diameter − (2 × required collet pre-load deflection). For Ø6mm tube: tube insertion bore 6.20mm ±0.020mm; collet groove OD 7.70mm ±0.010mm; O-ring Ø1.78mm cross-section; O-ring groove depth 0.36mm ±0.010mm; all from Swiss CNC guide bushing single program. Post-production: 100% collet groove OD go-gauge per fitting (go-gauge diameter set to tolerance maximum — fitting passes if groove OD does not close the go-gauge). Nickel-plated programs: pre-plate target adjusted +0.016mm/side (8μm nickel × 2 sides) so post-plate collet groove OD lands at nominal ±0.010mm — confirmed by 100% post-plate collet groove go-gauge. Tube pull-out force calculation provided in 48-hour DFM for each tube OD and operating pressure in the customer's pneumatic circuit specification.
BSP / NPT / Metric — 100% Gauge per Fitting, All Thread Standards
BSP G-type ISO 228 Class A (G1/8, G1/4, G3/8, G1/2): single-point CNC threading; pitch diameter ±0.005mm; 100% ring gauge (external thread) and 100% plug gauge (internal thread) per fitting before and after nickel plate; port face flatness 0.010mm/25mm for bonded Dowty seal programs; O-ring groove depth ±0.010mm for face O-ring seal programs. NPT ASME B1.20.1 (1/16 NPT, ¼-18, 3/8-18, ½-14): 100% L1 taper ring gauge per fitting; single-point CNC threading for stainless steel programs (galling prevention); CNC die head for brass NPT at production rate. Metric M3/M5/M6/M7: Swiss CNC single-point threading ±0.005mm for miniature pneumatic instrument and small-bore cylinder programs; 100% ring gauge. Post-plate: 100% BSP plug gauge confirming thread pitch diameter within ISO 228 Class A limits after nickel plating growth.
Integrated Surface Treatment — Four Programs with IATF Quality Control
Bright nickel ASTM B689 (8–12μm standard): XRF thickness ±1μm per plating lot; adhesion ASTM B571 per lot; ASTM B117 96h salt spray; 100% post-plate collet groove go-gauge; 100% post-plate BSP thread gauge; EC 1935/2004 food contact compliance. Natural brass + PTFE pre-applied thread sealant: for industrial machine tool, factory automation, and robot programs in clean indoor environments — eliminating installer PTFE tape application step at automated assembly line. Satin Ni+PTFE composite (10–15μm; FDA 21 CFR 175.300; food contact; non-stick; HV 200+): for food-grade pneumatic fittings requiring both chemical resistance and nickel corrosion protection. Zinc-nickel ASTM B841 (8–15μm; 720h ASTM B117 salt spray): for machine tool coolant splash environments, outdoor equipment, and agricultural machinery pneumatic circuits — 7× better salt spray than standard bright nickel.
100% Pressure Test + PPAP Level 3 / IATF 16949
100% air pressure leak test: automated pressure test rig; 1.5× PN rated (15 bar for PN10; 24 bar for PN16); 30-second pressurize/hold/vent; water immersion or soap bubble; zero leak acceptance; records per fitting serial number archived minimum 10 years for IATF 16949 programs. Post-plate 100% collet groove go-gauge (confirming nickel growth did not close groove below minimum diameter). Post-plate 100% BSP plug gauge (confirming thread pitch diameter within ISO 228 Class A limits after plating). PPAP Level 3 for IATF 16949 automotive factory and robot pneumatic fitting programs: 30-piece pilot; initial Cpk ≥1.33 collet groove OD and thread pitch diameter (target ≥1.67 production); MSA Gage R&R ≤10% collet groove go-gauge and thread gauges; Control Plan; PSW. 99%+ first-article qualification rate.
Brass Pneumatic Fitting
Materials & Grades
Brass pneumatic fitting material selection is governed by the service environment (standard industrial air, food contact, potable water, chemical exposure, or cleanroom), regulatory compliance requirements (EC 1935/2004, WRAS, FDA 21 CFR), machinability economics for high-volume programs, and surface finish requirements for nickel plate compliance. C36000 dominates non-regulated programs; DZR CW602N governs food and WRAS-regulated programs; H59 optimises cost for Chinese domestic market supply; 316L stainless addresses pharmaceutical and semiconductor cleanroom programs.
C36000 Free-Machining Brass (CW614N)
Cu 60–63%; Zn 35–37%; Pb 2.5–3.7% (SII XRF per incoming lot) · 100% machinability reference standard · PCD turning at v_c = 400–600 m/min; Swiss CNC at 5,000–20,000 fittings/machine/hour · The standard material for the majority of brass pneumatic fittings globally — the gold-standard machinability enables the wholesale unit economics that make pneumatic brass fittings commercially viable at tens of millions of annual units. Natural gold-yellow colour provides instant visual identification in mixed-material pneumatic circuits. Brass's protective cuprous oxide passive film provides years of reliable service in indoor compressed air environments without painting or coating required. AMS and EN 12164 equivalent certification available for regulated programs. Applications: all standard industrial automation, machine tool, automotive factory, and robot pneumatic programs not requiring food contact material compliance.
C26000 Lead-Free Brass (CW508L)
Cu 68–72%; Pb ≤0.07% (SII XRF per lot — RoHS Pb ≤0.01% verification on export programs) · Machinability 40–50% (lower than C36000 from reduced lead content; v_c = 200–350 m/min; chip-break insert geometry mandatory to prevent long chips) · +30–40% cost premium over C36000 from lower machinability at equivalent geometry. For European market programs where EU Regulation 2020/784 (restricting lead in plumbing products) applies to pneumatic fitting specifications — increasingly adopted by European food processing equipment OEMs applying plumbing material compliance frameworks to all fluid circuit fittings including air. REACH SVHC compliance documentation per lot. Applications: European food processing machine pneumatic circuits requiring maximum material compliance margin; pharmaceutical equipment programs where lead content must be below detection limits for regulatory audit purposes.
DZR CW602N Dezincification-Resistant Brass
Cu 62–65%; Pb 1.6–2.5%; As 0.02–0.06% dezincification inhibitor (SII XRF MANDATORY per incoming lot — the As content governing WRAS compliance) · Machinability 55–65% (lower than C36000 from modified alloy composition; production rate adjustment for pneumatic fitting programs) · 15–20% cost premium over C36000. DZR CW602N meets UK Water Regulations Advisory Scheme (WRAS) and EU EN 12164 potable water material specification — applied by food equipment OEMs as the same material compliance framework for all fluid circuit fittings including pneumatic air circuits. EC 1935/2004 food contact material compliance for incidental food product contact from actuator exhaust air or CIP/SIP cleaning reaching pneumatic fitting external surfaces. WRAS certificate per batch available for regulated programs. Applications: food packaging machine pneumatic grippers; beverage filling line pneumatic actuator fittings; pharmaceutical cleanroom pneumatic circuits; food processing equipment pneumatic systems.
Nickel-Plated C36000 for Food-Grade Programs
C36000 base + bright nickel 8–12μm (ASTM B689) or satin Ni+PTFE composite (10–15μm; FDA 21 CFR 175.300) · For food equipment pneumatic programs where C36000 machinability economics are required but bare brass surface is unacceptable for food contact appearance or compliance. Bright nickel on C36000 with EC 1935/2004 food contact material declaration covers incidental contact applications. Satin Ni+PTFE composite: non-stick surface; easier CIP cleaning; chemical resistance to food-grade cleaning agents (citric acid, sodium hydroxide, hydrogen peroxide); FDA 21 CFR 175.300 for direct food contact surfaces. Post-plate: 100% collet groove go-gauge confirming nickel growth compensation achieved target groove OD ±0.010mm; 100% BSP/NPT thread gauge confirming thread pitch diameter within specification after plate. Critical: pre-plate target adjusted +0.016mm/side to compensate 8μm nickel growth — preventing the tolerance shift that CNCPioneer's DFM identified in the automotive robot case study Finding 1.
H59 CuZn40 Chinese-Standard Brass
Cu 57–60%; Zn 37–41%; Pb 0.5–1.5% (SII XRF per incoming lot confirming Cu 57–60%) · Machinability 60–70% (lower than C36000 from reduced lead content; v_c = 200–400 m/min) · 8–12% cost reduction versus C36000 from lower material cost and domestic supply chain. For cost-optimised pneumatic fitting programs for Chinese domestic market automation equipment, Chinese OEM machine tool pneumatic circuits, and domestic industrial programs where the cost premium of C36000 versus H59 is not justified by regulatory requirements or export specifications. GB/T 5231 material certificate per lot; SII XRF Cu 57–60% verification. Not recommended for export to European or North American markets where EN 12164 CW614N (C36000 equivalent) is the standard specification. Applications: Chinese domestic market pneumatic fittings; non-regulated industrial pneumatic circuits; domestic machine tool air circuit fittings.
316L Stainless Push-Fit Pneumatic Fittings
C ≤0.030%; Mo 2–3%; Cr 16–18% (SII XRF per lot) · Work-hardening prevention ≥0.10 mm/rev enforced; 70 bar through-spindle coolant throughout all operations · For pharmaceutical, semiconductor, and chemical environment pneumatic circuits where brass corrosion contamination is unacceptable and stainless steel push-fit pneumatic fittings are specified. Same push-fit collet groove and O-ring geometry as brass programs — same ±0.010mm collet groove OD and 100% pressure test standard. ASTM A967 passivation standard post-machining. ASME BPE EP SF2 Ra ≤0.38μm available for pharmaceutical pneumatic circuit programs where hygienic surface quality is specified on pneumatic fittings. VSM μ_r ≤1.005 per lot for MRI-adjacent laboratory and medical equipment programs. HEPA-compatible materials. ISO 13485-compatible quality records for medical device pneumatic circuit programs. Higher unit cost than brass — reserved for programs where brass corrosion or contamination risk is unacceptable.
Bright Nickel Plate ASTM B689
Bright nickel 8–12μm on C36000 brass pneumatic fittings — the standard finish for food equipment, pharmaceutical, and premium industrial automation pneumatic programs. XRF thickness ±1μm per plating lot; adhesion ASTM B571 per lot; ASTM B117 96h salt spray. CRITICAL post-plate inspection sequence: (1) 100% collet groove OD go-gauge confirming nickel growth within pre-load specification (nickel grows on groove floor: 8μm per side = 0.016mm diameter reduction — pre-plate target must be machined +0.016mm oversize to compensate); (2) 100% BSP plug/ring gauge confirming thread pitch diameter within ISO 228 Class A limits after nickel growth. Both post-plate inspections are non-negotiable and are included as standard in all CNCPioneer nickel-plated pneumatic fitting programs — the checks identified as missing in the automotive robot case study DFM finding (Finding 3: post-plate pressure test standard established; pre-plate test cancelled as redundant for detecting hydrogen embrittlement cracking from plating).
Satin Ni+PTFE Composite Coating
Composite electroless Ni-P + PTFE coating (Niflor or equivalent) 10–15μm; non-stick PTFE-modified surface; HV 200+ wear resistance; chemical resistance to food-grade cleaning agents (citric acid, sodium hydroxide, hydrogen peroxide concentrations used in CIP/SIP cycles). FDA 21 CFR 175.300 compliant for food contact applications — the surface finish combining both the nickel's corrosion protection and PTFE's chemical resistance and non-stick properties. Low friction thread installation from PTFE surface lubricity — reducing installation torque requirement and eliminating PTFE tape application step at automated assembly line. Applications: food processing machine pneumatic circuits with CIP/SIP cleaning exposure; beverage plant pneumatic fittings where acidic cleaning solutions contact fitting external surfaces; pharmaceutical cleanroom pneumatic circuits requiring maximum surface chemical resistance. Post-coat: 100% collet groove go-gauge confirming composite coat growth within push-fit pre-load specification.
Zinc-Nickel Electroplate ASTM B841
8–15μm zinc-nickel (12–15% Ni alloy) per ASTM B841 for brass pneumatic fittings in machine tool coolant splash environments, outdoor equipment, and agricultural machinery pneumatic circuits where standard bright nickel has inadequate salt spray resistance. Zinc-nickel provides 720+ hours ASTM B117 salt spray resistance versus bright nickel's 96 hours — 7.5× improvement from the sacrificial zinc-nickel electrochemical protection mechanism. For machine tool CNC coolant splash programs: zinc-nickel withstands continuous coolant (5–10% water-soluble cutting fluid) exposure without the white corrosion products that bright nickel develops within weeks in coolant-splash environments. For outdoor agricultural equipment: zinc-nickel withstands salt road splash, moisture, and UV from agricultural service environments. Post-plate: 100% collet groove go-gauge; 100% BSP thread gauge. Trivalent chromate topcoat passivation RoHS-compliant standard. Applications: CNC machine tool ATC and spindle air barrier circuit fittings; outdoor equipment pneumatic control circuits; construction equipment hydraulic manifold pneumatic signal port fittings.
Surface Treatments for
Brass Pneumatic Fittings
Brass pneumatic fitting surface treatment selection addresses decorative corrosion protection (bright nickel ASTM B689 — standard), food-grade chemical resistance (satin Ni+PTFE composite — FDA 21 CFR 175.300), machine tool and outdoor corrosion protection (zinc-nickel ASTM B841 — 720h ASTM B117 salt spray), and PTFE pre-applied thread sealant for assembly line installation speed. All surface treatments coordinated through IATF 16949-assessed Pearl River Delta plating partners at 1–2 day transit.
Bright Nickel Plate ASTM B689 — Standard on Food Equipment & Premium Programs
Bright nickel 8–12μm on C36000 brass pneumatic fittings for food equipment, pharmaceutical, and premium industrial automation programs requiring the bright nickel surface that hides brass oxidation in humid environments and provides EC 1935/2004 food contact material compliance for incidental food product contact. XRF thickness ±1μm per plating lot; ASTM B571 adhesion per lot; ASTM B117 96h salt spray.
Non-negotiable post-plate inspection sequence at CNCPioneer: (1) 100% collet groove OD go-gauge — nickel grows 8μm per side on groove floor (0.016mm diameter reduction); pre-plate target machined +0.016mm oversize; post-plate go-gauge confirms groove OD lands at nominal ±0.010mm and collet pre-load remains within pull-out force specification. (2) 100% BSP/NPT thread gauge — nickel growth on thread flanks confirmed within ISO 228 Class A pitch diameter limits. (3) 100% air pressure leak test post-plate (not pre-plate) — detects hydrogen embrittlement cracking from nickel sulfamate plating bath, the failure mode identified in the automotive robot case study DFM Finding 3 that pre-plate testing cannot catch. All three post-plate inspections are standard at no additional charge on all CNCPioneer nickel-plated pneumatic fitting programs.
Natural Brass + PTFE Pre-Applied & Satin Ni+PTFE Composite
Natural brass (no plating) + PTFE pre-applied thread sealant: the most economical finish for industrial machine tool, factory automation, and robot pneumatic programs in clean indoor environments where brass oxidation is cosmetically acceptable and food contact compliance is not required. PTFE tape pre-applied to the male BSP or NPT thread zone before delivery — eliminating the PTFE tape application step at the OEM automated assembly line (saving 5–15 seconds per fitting installation at automated assembly stations processing 200–500 fittings per hour). PTFE film thickness and coverage verified by operator check per lot. 100% pressure test standard; 100% thread gauge standard on all programs.
Satin Ni+PTFE composite coating (Niflor or equivalent; 10–15μm; HV 200+; FDA 21 CFR 175.300): for food-grade pneumatic fittings requiring both chemical resistance of PTFE and the corrosion protection of nickel. Non-stick surface reduces build-up of food processing debris on fitting external surfaces; low friction thread installation from PTFE surface lubricity. Chemical resistance to CIP/SIP cleaning agents (citric acid, NaOH, H₂O₂ at standard food-grade concentrations). Post-coat 100% collet groove go-gauge; 100% thread gauge; 100% pressure test.
Zinc-Nickel ASTM B841 — Machine Tool Coolant & Outdoor Programs
8–15μm zinc-nickel (12–15% Ni alloy) per ASTM B841 for brass pneumatic fittings in machine tool coolant splash environments, outdoor equipment, and agricultural machinery pneumatic circuits where standard bright nickel has inadequate salt spray resistance. 720+ hours ASTM B117 salt spray resistance versus bright nickel's 96 hours — 7.5× improvement from the zinc-nickel's sacrificial electrochemical protection mechanism (zinc preferentially corrodes, protecting the base brass from corrosion even when the coating is scratched or chipped).
For CNC machine tool ATC and spindle air barrier circuit fittings: zinc-nickel withstands continuous 5–10% water-soluble cutting fluid coolant splash without the white corrosion products that bright nickel develops within weeks in coolant-splash environments. Trivalent chromate topcoat passivation RoHS-compliant standard. Post-plate: 100% collet groove go-gauge confirming zinc-nickel growth (8–15μm total = 16–30μm diameter reduction on groove OD) within pre-load specification — larger growth than bright nickel, requiring larger pre-plate compensation; 100% BSP/NPT thread gauge; 100% pressure test. XRF zinc-nickel thickness ±2μm per plating lot.
Surface finish selection by program: standard industrial automation / robot pneumatic → natural brass + PTFE pre-applied (most economical; assembly-line ready); food equipment / pharmaceutical / premium industrial → bright nickel ASTM B689 (+$0.04–0.12/fitting; EC 1935/2004 food contact compliance); food-grade CIP/SIP chemical exposure → satin Ni+PTFE composite (+$0.08–0.20/fitting; FDA 21 CFR 175.300); machine tool coolant splash / outdoor → zinc-nickel ASTM B841 (+$0.06–0.15/fitting; 720h B117). All nickel-plated programs include 100% post-plate collet groove go-gauge, 100% post-plate BSP/NPT thread gauge, and 100% post-plate air pressure leak test as standard — the complete post-plate inspection sequence at no additional charge.
Quality Assurance for
Brass Pneumatic Fittings
Brass pneumatic fitting quality assurance is built around four non-negotiable controls: 100% collet groove OD go-gauge per fitting (governing tube pull-out force); 100% BSP/NPT/metric thread gauge per fitting (governing thread sealing integrity); 100% air pressure leak test per fitting serial number (governing assembled circuit leak-free operation); and SII XRF per incoming lot (governing food-grade DZR As content and C36000 composition compliance). All four standard — not sampled — on all CNCPioneer pneumatic brass fitting programs.
Engineering DFM — 24-Hour Quote, 48-Hour DFM
Material selection (C36000 vs DZR vs H59 from regulatory and service requirements with per-fitting cost impact and food contact material compliance analysis) · tube OD push-fit collet groove OD target calculation per tube tolerance and nickel plate growth compensation · O-ring material from media compatibility (NBR standard / EPDM food-grade / FKM chemical) · thread standard and size (BSP G-type vs NPT vs metric) · metering orifice diameter from cylinder speed and supply pressure for speed controller fittings · port angular position achievability from MAZAK mill-turn C-axis for multi-port manifold programs · elbow port perpendicularity specification for 90°/45° elbow programs · 100% pressure test scope · PPAP Level 3 scope for IATF 16949 programs · free sample availability for new program qualification.
Material Verification — SII XRF per Lot
SII XRF per incoming lot before machining: C36000 (Cu 60–63%; Pb 2.5–3.7% confirmed); DZR CW602N (As 0.02–0.06% MANDATORY — the dezincification inhibitor content governing WRAS and EC 1935/2004 compliance; any lot below 0.02% As rejected — As below minimum means dezincification protection is absent); H59 (Cu 57–60%); 316L stainless (C ≤0.030%; Mo 2–3%; Cr 16–18%). EN 10204 3.1 or material test report per lot archived; lot traceability from bar certificate to production lot to delivery documentation and PPAP PSW. DZR As XRF certificate included in delivery documentation per lot for food-grade programs as standard.
In-Process Collet Groove, O-Ring Groove & Thread Controls
Collet groove OD: 100% go-gauge per fitting on all push-fit programs (go-gauge diameter set to tolerance maximum); spot CMM measurement on first piece and every 200 pieces for ±0.010mm precision programs. O-ring groove dimensions: CMM spot check every 10% of production; 100% first piece of each production session after insert change. Thread gauging: 100% BSP plug/ring and NPT L1 taper gauge per fitting before surface treatment dispatch. Post-plate: 100% collet groove OD go-gauge after bright nickel plate confirming nickel growth did not close groove below minimum diameter (collet pre-load would be excessive → insertion force failure); 100% BSP plug gauge after nickel plate confirming thread pitch diameter within ISO 228 Class A limits. 100% air pressure leak test: post-plate on all nickel-plated programs per DFM finding 3 (hydrogen embrittlement cracking from plating bath detectable only by post-plate test).
100% Air Pressure Leak Test per Fitting Serial Number
Automated pressure test rig: 1.5× PN rated working pressure (15 bar for PN10; 24 bar for PN16); 30-second pressurize/hold/vent; water immersion or soap bubble test; zero bubble-leak tolerance (zero leak acceptance — any bubble = fail); records per fitting serial number in quality system. All sealed pneumatic brass fitting programs — prototype through volume — receive 100% individual pressure test as a production standard, not a sample audit. Test applied post-plate on nickel-plated programs (hydrogen embrittlement cracking from plating bath would escape detection in a pre-plate test). Pressure test records per serial number archived 10 years minimum for IATF 16949 programs. Cost of 100% testing: $0.01–0.04/fitting — 1.2–3.8% of expected production loss from a single escaped defective fitting reaching an automotive robot pneumatic circuit.
Final Inspection & Surface Treatment Verification
CMM: body OD; thread port face flatness (for bonded seal programs); port angular position (elbow and tee programs); body length; flow bore; metering orifice diameter (if applicable). Profilometry: body Ra per lot for premium programs. Nickel plate: XRF thickness ±1μm per plating lot; ASTM B571 adhesion per lot. DZR As XRF certificate per lot for food-grade programs. Zinc-nickel XRF thickness ±2μm per plating lot; trivalent chromate passivation certificate per lot. Satin Ni+PTFE composite adhesion and PTFE content per lot. Collet and O-ring pre-assembly inspection: O-ring cross-section diameter per lot; collet spring wire diameter ±0.010mm per lot confirming correct tube OD size. Assortment kit counting: calibrated scale per kit weight verification; part number label per pocket verified.
PPAP Level 3 Documentation & SPC Monitoring
PPAP Level 3 for IATF 16949 automotive factory and robot pneumatic fitting programs: 30-piece pilot per fitting type; initial Cpk ≥1.33 collet groove OD and thread pitch diameter (PPAP acceptance; target ≥1.67 in production from SPC monitoring); MSA Gage R&R ≤10% on collet groove go-gauge and thread gauges; PFMEA (collet groove out-of-spec; nickel plate growth collet groove violation; O-ring missing; thread out-of-spec; pressure test leak path); Control Plan; PSW. SPC real-time monitoring all critical pneumatic fitting dimensions; monthly Cpk reporting per IATF 16949 customer-specific requirements. Pressure test records archived 10 years; material lot certificates archived 10 years. Free sample (5 pieces per fitting type) for qualified wholesale account qualification of new fitting programs before volume commitment.
100% Collet Groove OD Go-Gauge per Fitting
Every production fitting — prototype or volume — receives 100% collet groove OD go-gauge verification. Go-gauge diameter set to tolerance maximum; fitting passes if groove OD does not close the go-gauge. Confirms minimum collet pre-load for ≥50N tube pull-out force per ISO 15218.
- 100% per fitting — not sampled — all push-fit programs
- Pre-plate and post-plate go-gauge for nickel-plated programs
- Go-gauge records per fitting archived for IATF 16949 programs
100% BSP/NPT/Metric Thread Gauge per Fitting
100% BSP ring gauge (external male thread) or plug gauge (internal female thread) per ISO 228 Class A limits; 100% NPT L1 taper ring gauge per ASME B1.20.1; 100% metric ring gauge. Pre-plate and post-plate gauging for all plated programs — confirming plate growth within thread tolerance.
- 100% BSP/NPT/Metric gauge per fitting — all programs
- Post-plate thread gauge after nickel/zinc-nickel plate
- Gauge calibration traceable to NIST/NPL standards
100% Air Pressure Leak Test — Post-Plate, Per Serial Number
100% individual pressure test: 1.5× PN rated (15 bar PN10 / 24 bar PN16) / 30-second / water immersion or soap bubble / zero bubble / per serial number. Applied post-plate on plated programs. Records per fitting serial number archived 10 years. Standard on all sealed programs, no additional charge.
- 100% per fitting serial number — not batch sampled
- Post-plate test (detects hydrogen embrittlement cracking)
- Records per serial number archived 10 years IATF 16949
SII XRF Material Compliance + PPAP Level 3
SII XRF per lot: C36000 Cu 60–63%; DZR CW602N As 0.02–0.06% MANDATORY per lot (below 0.02% → lot rejected); H59 Cu 57–60%. PPAP Level 3 for IATF 16949: 30-piece pilot; Cpk ≥1.33 minimum (≥1.67 target); MSA R&R ≤10%; Control Plan; PSW.
- DZR As 0.02–0.06% XRF MANDATORY per lot — lot rejection policy
- PPAP Level 3: Cpk ≥1.33 acceptance; ≥1.67 target in production
- SPC monthly Cpk reporting per IATF 16949 customer requirements
Brass Pneumatic Fittings FAQ
Common questions from industrial automation and robot assembly equipment manufacturers, automotive factory pneumatic Tier 1 suppliers, compressed air system distributors, food processing and packaging equipment OEMs, machine tool pneumatic circuit manufacturers, and wholesale pneumatic fitting distributors about CNCPioneer's push-fit mechanism, collet groove precision, BSP vs NPT thread selection, 100% pressure test economics, and OEM volume program pricing.
The push-fit (push-in) connection mechanism in brass pneumatic fittings operates through a stainless steel or polypropylene collet spring that grips the pneumatic tube's outer diameter when the tube is inserted into the fitting body. The collet — a thin-walled cylindrical spring with multiple axial slots creating flexible fingers — is pre-assembled in an annular groove (the collet groove) machined into the fitting body's bore. When a pneumatic tube is pushed into the fitting, the tube's leading edge contacts the angled tips of the collet fingers and flexes them outward; as the tube advances past the collet tips, the collet fingers spring back inward to their natural pre-load position, with the collet tips now contacting the tube OD surface just behind the tube's leading end — locking the tube by a friction grip plus the mechanical interlock of the angled collet tip against the tube's cylindrical surface. To release the tube, the operator presses the collet release ring inward against the collet fingers, flexing them outward and away from the tube surface — allowing tube withdrawal. The collet groove OD (the diameter of the groove floor in the fitting body bore where the collet sits in its rest, un-deflected state) is the single most critical precision dimension in the push-fit fitting because it directly determines the collet's radial pre-load against the inserted tube: collet pre-load = (collet_natural_diameter − collet_groove_OD) × collet_spring_constant. For a standard stainless wire collet sized for Ø6mm tube: natural diameter (relaxed) = 7.90mm; installed in groove OD 7.70mm → radial pre-load = (7.90 − 7.70)/2 = 0.10mm radial deflection per collet finger. When the collet groove OD varies: groove OD too large by +0.030mm → pre-load drops from 0.10mm to 0.085mm → pull-out force falls from 50N to 37N for Ø6mm tube — below ISO 15218 minimum 50N, producing tube ejection from the fitting at rated pneumatic system pressure during actuator operation. Groove OD too small by −0.030mm → pre-load increases to 0.115mm → insertion force exceeds 80N ergonomic limit → tube cannot be manually inserted to the lock position in the assembly line process time allocated for tube connection. CNCPioneer's ±0.010mm collet groove OD specification — achieved from Swiss CNC guide bushing turning at the support point without deflection — produces pull-out force in the range 50–100N for Ø6mm tube at PN10, simultaneously satisfying the ISO 15218 minimum retention and the ergonomic maximum insertion force. This dimensional accuracy is the fundamental quality parameter that makes CNCPioneer's brass pneumatic fittings safe for rated-pressure pneumatic circuit use.
BSP (British Standard Pipe) and NPT (National Pipe Thread) are the two dominant thread standards for pneumatic fitting-to-component connections globally, and the choice between them is determined entirely by the thread standard of the pneumatic components the fittings will connect to — not by any engineering preference for the thread form itself. BSP (ISO 228 G-type parallel thread) is standard on pneumatic components from: European manufacturers (Festo, Bosch Rexroth, Parker-Legris, SMC European range); Asian manufacturers supplying to European and Asian markets (SMC Japan, CKD, Koganei, Airtac, Mindman); and Commonwealth market equipment. The BSP G-type parallel thread (ISO 228) is the most common pneumatic body port at G1/8, G1/4, G3/8, and G1/2 sizes. BSP G-type threads are NOT self-sealing — they require a bonded Dowty seal under the fitting hex shoulder, or PTFE tape plus thread-sealing compound, or an O-ring in the fitting port face groove for pressure-tight connection. NPT (ASME B1.20.1 tapered thread) is standard on pneumatic components from: North American manufacturers (Parker Hannifin US range, Numatics, ARO, SMC US models with NPT ports). NPT threads are self-sealing (the tapered thread form produces metal-to-metal contact between mating thread flanks when tightened to engagement depth) plus PTFE tape fills the helical interface. The practical consequence for fitting selection: if your pneumatic circuit connects to Festo, Parker Legris, SMC European series, or Airtac → specify BSP G-type body ports; if connecting to Parker Hannifin US series, Numatics, or other North American components → specify NPT body ports; if connecting to both → specify custom BSP × NPT adapter fittings. The most commonly confused thread sizes: G1/4 BSP and ¼-18 NPT are completely non-interchangeable despite similar nominal size designation — they differ in thread form (55° Whitworth vs. 60° NPT flank), taper (parallel BSP vs. 1/16 in/in NPT taper), and TPI (19 BSP vs. 18 NPT). CNCPioneer's 48-hour DFM for every brass pneumatic fitting inquiry confirms the pneumatic component port thread standard from the customer's component datasheets or physical samples before committing to fitting thread geometry — preventing costly BSP/NPT substitution errors on the customer's assembly line.
The standard quality practice for catalog pneumatic fitting suppliers — whether European specialists or Asian catalog fitting distributors — is lot-based pressure testing: typically 5–10 fittings sampled from a production lot of 1,000–5,000, with the remaining 990–4,995 fittings shipped without individual pressure verification. This practice is statistically rational for catalog fittings supplied to general industrial markets where the fitting defect rate is low (0.05–0.2% for mature product lines) and the consequence of a single fitting failure is an air leak causing circuit malfunction — a minor efficiency loss. CNCPioneer's 100% individual pressure test is appropriate and commercially justified for OEM custom brass pneumatic fitting programs for the following cost-benefit analysis. Cost of 100% pressure testing at CNCPioneer (automated pressure test rig; 30-second cycle; capital amortised over production volume): $0.01–0.04/fitting — negligible relative to the fitting unit cost of $0.15–0.55. Cost of a single escaped defective fitting in an automotive robot pneumatic circuit: a Tier 1 automotive supplier's assembly robot stops production when a pneumatic cylinder fails to actuate (defective fitting → air loss → insufficient actuator pressure → cylinder does not complete stroke → robot E-stop). Automotive assembly line downtime cost: typically $8,000–$25,000/minute. If the defective fitting produces 30 minutes of production downtime: $240,000–$750,000 production loss from one defective pneumatic fitting. At CNCPioneer's production defect rate of 0.2% at worst case, shipping without 100% test to 460,800 fittings/year produces 922 defective fittings per year in service — with the Poisson probability of at least one defective fitting reaching a critical robot pneumatic circuit producing one major production line incident per year. The expected annual production loss from non-tested pneumatic fittings: $240,000–$750,000 versus the annual cost of 100% testing at CNCPioneer: 460,800 × $0.02 = $9,216. The 100% testing cost is 1.2–3.8% of the expected production loss from escaped defects — making 100% individual pressure testing the economically dominant choice for automotive, robot, and safety-critical pneumatic circuit OEM programs.
Lead times at CNCPioneer for brass pneumatic fitting prototype programs: C36000 push-fit straight union Ø8mm (collet groove ±0.010mm; O-ring; nickel; 100% pressure test; 50-piece) — 3–4 business days; C36000 G1/4 BSP male × Ø8mm push-fit (100% BSP gauge; 100% pressure test; nickel; 50-piece) — 3–4 days; C36000 push-fit 90° elbow Ø8mm (C-axis ±0.020° perpendicularity; 100% pressure test; nickel; 25-piece) — 4–5 days; C36000 push-fit tee Ø8mm (C-axis 90° branch; 100% pressure test; 25-piece) — 4–5 days; C36000 4-port manifold (G1/4 BSP × 4× Ø8mm; C-axis; 100% pressure test; nickel; 10-piece) — 5–7 days; DZR CW602N food-grade union set (As XRF; nickel; 100% pressure test; FAIR; 25-piece per type) — 4–6 days. Volume economics: C36000 push-fit straight union Ø8mm at 25,000–100,000/year $0.37–0.55; at 2M–10M/year $0.11–0.17; at 10M+/year $0.075–0.11. C36000 G1/4 BSP × Ø8mm at 25,000–100,000/year $0.51–0.75; at 10M+/year $0.10–0.15. Four-tier market comparison for C36000 bright nickel G1/4 BSP male × Ø8mm push-fit fitting (100% BSP gauge; 100% pressure test post-plate; collet groove 100% go-gauge; IATF 16949 PPAP Level 3) at 460,800/year: European pneumatic fitting specialist (Legris, Parker, Norgren OEM equivalent program): €0.38–0.55/fitting; Taiwanese precision machining (ISO 9001-certified): $0.25–0.38/fitting; CNCPioneer China (IATF 16949; C36000 SII XRF per lot; Swiss CNC ±0.010mm collet groove; 100% BSP gauge; 100% post-plate pressure test; 100% post-plate collet groove go-gauge; PPAP Level 3): $0.15–0.23/fitting (case study achieved €0.195 ≈ $0.21/fitting at 460,800/year); lowest-cost Asian general machining (no collet groove gauging; 5% sample pressure test; no PPAP; nickel ±3μm): $0.09–0.14/fitting. The CNCPioneer versus lowest-cost Asian premium: $0.06–0.09/fitting (43–64% above lowest-cost) provides: ±0.010mm collet groove OD accuracy with 100% go-gauge; 100% post-plate pressure test; 100% post-plate collet groove go-gauge preventing nickel-growth-induced insertion force failure; IATF 16949 PPAP Level 3. The case study validated saving: €0.42 European versus €0.195 CNCPioneer = €0.225/fitting × 460,800/year = €103,680 annual saving per robot model. Across a 5-model robot line: €518,400 annual fitting cost reduction — with superior quality (100% tested at 15 bar; 100% collet groove gauged; PPAP Level 3) versus the European supply program's 5% sample-tested equivalent.
Get a Quote for Brass Pneumatic Fittings
Upload your brass pneumatic fitting drawings, 3D CAD models, tube OD specifications (metric 4–16mm or imperial 5/32"–½"), thread body standard (BSP G-type ISO 228 / NPT ASME B1.20.1 / metric), fitting type requirements, quantity per type, annual volume, surface finish requirement (bright nickel / natural brass + PTFE / DZR food-grade / satin Ni+PTFE / zinc-nickel), or complete pneumatic fitting BOM and receive a competitive quotation within 24 hours and complete engineering DFM within 48 hours — covering material selection from your service environment and regulatory requirements (C36000 vs DZR CW602N vs H59 with per-fitting cost impact and food contact material compliance analysis); tube OD push-fit collet groove OD target calculation per tube tolerance and nickel plate growth compensation; O-ring material selection (NBR standard / EPDM food-grade / FKM chemical); thread standard confirmation and gauge specification; port angular position achievability from MAZAK mill-turn C-axis for multi-port manifold programs; 100% pressure test scope (standard all sealed programs); 100% post-plate collet groove go-gauge scope for nickel-plated programs; PPAP Level 3 scope for IATF 16949 automotive factory and robot pneumatic programs; assortment kit packaging; free sample availability; and complete per-fitting pricing from prototype first articles through IATF 16949 governed production and wholesale supply.