
Precision Aluminum CNC
Turning Parts
CNCPioneer is an AS9100D and IATF 16949 certified aluminum CNC turning parts specialist — 78+ Swiss CNC lathes with guide bushing support and 66+ MAZAK mill-turn centers delivering shafts, bushings, sleeves, spacers, hex standoffs, and complex aluminum bodies across Ø0.5mm to Ø1,000mm at ±0.002mm diameter, ±0.001mm roundness, and Ra 0.05μm surface finish since 2011.

What Is Aluminum
CNC Turning?
Aluminum CNC turning is the computer-controlled precision machining process — executed on Swiss CNC lathes with guide bushing support, MAZAK mill-turn centers with C-axis and live tooling, MAZAK VARIAXIS 5-axis simultaneous platforms, and precision cylindrical grinding systems — that produces aluminum parts whose primary geometry is defined by rotation about a central axis: shafts, bushings, sleeves, spacers, collars, hubs, pins, nozzles, adapters, valve bodies, and thousands of other rotational-symmetry components.
Aluminum's machinability index of 300–500% relative to steel means CNC turning of aluminum produces parts at 3–5× the cutting speed of equivalent steel programs, reducing cycle time and per-part cost by 60–75%. Simultaneously, aluminum's density of 2.70–2.80 g/cm³ — one-third of steel's — means turned aluminum parts weigh one-third as much for the same structural cross-section, driving selection across every weight-sensitive application.
-
Swiss CNC guide bushing — the precision foundation for small & slender parts For Ø0.5–32mm parts at L/D up to 20:1, guide bushing positioning eliminates deflection regardless of bar length — achieving ±0.005mm OD on Ø2mm pins that would deflect 0.050mm+ under cutting force on any standard chuck lathe.
-
PCD tooling — aluminum surface finish precision foundation PCD hardness (HV 8,000+) maintains a razor-sharp cutting edge that shears aluminum chips without micro-tearing, producing Ra 0.4μm standard, Ra 0.2μm precision, and Ra 0.1μm diamond-cut finishes directly from turning — eliminating BUE defects that carbide tooling creates on precision aluminum surfaces.
-
100% SII XRF incoming material verification Every aluminum alloy lot verified by SII XRF composition analysis before machining — confirming alloy identity against forged material certificates and eliminating the alloy substitution risk that precision supply chains cannot afford in AS9100D and IATF 16949 programs.
-
40–60% China aluminum turning cost advantage 40–60% below US and European precision turning facilities at equivalent AS9100D/IATF 16949 quality and documentation — engineering DFM review, alloy selection analysis, tolerance achievability assessment, and FAIR included in program pricing without surcharges.

Why CNCPioneer for
Aluminum CNC Turning Parts?
Among aluminum CNC turning parts suppliers globally, CNCPioneer's Swiss CNC guide bushing precision, PCD tooling surface quality, CBN precision grinding, 100% XRF material verification, MAZAK mill-turn completeness, and China cost advantage establish our factory as the preferred aluminum turning partner across aerospace, EV, semiconductor, medical, and industrial programs.
Swiss CNC Guide Bushing — Slender & Small Part Precision
CNCPioneer's 78+ Swiss CNC lathes with guide bushing support provide the dimensional accuracy foundation for aluminum CNC turning parts where standard chuck turning cannot achieve the required specification. The guide bushing positions the cutting tool within 0.5–2.0mm of the workpiece support point — achieving ±0.005mm OD on aluminum shafts at 20:1 L/D and ±0.003mm OD on Ø2mm aluminum pins that would deflect 0.024mm+ under cutting force on any standard chuck lathe.
PCD Tooling — Ra 0.4μm as Production Standard
Polycrystalline diamond (PCD) tooling in aluminum eliminates built-up edge entirely — PCD's HV 8,000+ hardness and 560 W/m·K thermal conductivity produce a razor-sharp cutting edge that shears aluminum cleanly without micro-tearing. CNCPioneer achieves Ra 0.4μm standard, Ra 0.2μm precision, and Ra 0.1μm diamond-cut directly from PCD turning — not as special processes requiring premium pricing, but as production standard capability.
CBN Precision Cylindrical Grinding — ±0.002mm & Ra 0.05μm
When aluminum CNC turning parts require dimensional accuracy beyond ±0.005mm achievable from Swiss CNC turning — bearing journals, precision bore fits, high-precision shaft ODs for interference-fit assembly — CNCPioneer's CBN cylindrical grinding programs extend precision to ±0.002mm OD, ±0.001mm roundness, and Ra 0.05μm surface finish from between-centers CBN grinding, applied to the minority of features requiring ground surface quality.
100% SII XRF Material Verification
CNCPioneer maintains safety stock in 6061-T6, 7075-T6, 2024-T4, 6063-T5, 5052-H32, 7050-T7451, and 2219-T87 with SII XRF composition verification on every incoming lot — confirming alloy identity before machining commitment. In a market where aluminum alloy substitution is a documented quality risk, 100% XRF verification provides the material traceability that AS9100D and IATF 16949 programs require and that general Chinese turning shops without laboratory verification infrastructure cannot provide.
MAZAK Mill-Turn — Complex Aluminum Parts, Single Setup
Complex aluminum CNC turning parts — shafts with keyways, hubs with bolt circles, spacers with cross-drilled holes, adapters with milled flats and threaded ports — require mill-turn centers combining turning and milling in one setup. CNCPioneer's 66+ MAZAK mill-turn centers with live tooling and full C-axis produce complex aluminum turning parts where all features share one datum reference frame — eliminating the ±0.050–0.200mm multi-setup datum errors that produce geometric tolerance violations.
40–60% China Aluminum Turning Cost Advantage
Precision aluminum CNC turning parts from US and European precision turning facilities cost 40–60% more than CNCPioneer's AS9100D/IATF 16949-equivalent programs — the manufacturing cost differential that determines whether precision aluminum turned component programs are commercially viable in competitive end-product markets. Engineering DFM, alloy selection analysis, PPAP documentation, and FAIR are all included in program pricing.
Aluminum CNC Turning Parts
We Manufacture
CNCPioneer's aluminum CNC turning programs cover the complete rotational component architecture — from Ø0.5mm micro-turned pin bodies through Ø1,000mm large-format flanges, including round shafts and bushings, complex multi-diameter bodies, square and hex forms, high aspect ratio slender shafts, and large structural disk bodies at every tolerance class.

Round Parts — Shafts, Bushings, Sleeves & Spacers
The largest volume category — shafts, pins, bushings, spacers, collars, and sleeves appearing in virtually every mechanical assembly. Motor rotor shafts with bearing journal ±0.002mm k5 fit and Ra 0.2μm; linear motion shafts with thread OD ±0.005mm and journal Ra 0.2μm; sliding contact bushings with ID ±0.005mm H7 and Ra 0.4μm; precision spacers with face parallelism 0.005mm; hydraulic sleeves with bore ID ±0.005mm and Ra 0.2μm. Range: Ø2mm through Ø200mm. Materials: 6061-T6 standard; 7075-T6 high-strength; 2024-T4 fatigue-critical. Surface treatment: Type II or III anodize, electroless Ni-P, Alodine.

Complex Parts — Multi-Diameter, Undercut & Eccentric
Multi-diameter stepped shafts with 3–15 distinct diameter zones, internal bores with O-ring grooves, eccentric OD from programmable eccentric chuck programs, valve bodies with NPT/BSP threaded ports, and compound taper profiles. Datum diameter ±0.002mm; functional diameters ±0.003–0.005mm per fit class; shoulder perpendicularity 0.005mm; eccentric position accuracy ±0.010mm. Integrated C-axis milled features: keyways ±0.020mm width, cross-holes ±0.020mm true position, milled flats ±0.010mm, threaded ports with 100% GO/NO-GO verification — all from single MAZAK mill-turn setup eliminating datum errors between operations.

Hex & Square Parts — Standoffs, Couplings & Adapter Bodies
Hex standoff turning programs (M3–M12, 6061-T6) producing the electronics and instrumentation fastener standard: internal thread ISO metric M3–M12 ±0.005mm pitch diameter, 100% GO/NO-GO; body length ±0.050mm standard, ±0.020mm precision; end face parallelism 0.010mm for flat stacking. Hex coupling bodies with precision internal bore ±0.010mm and O-ring groove ±0.020mm. Square bar turning programs for structural adapter bodies with central precision bore. Volume programs at 1.2M+ standoffs per year. All from MAZAK mill-turn with C-axis indexing — turning and milling from one setup without angular re-alignment.

Small & Micro Parts — Ø0.5mm to Ø25mm, Swiss CNC
The category that separates Swiss CNC guide bushing capability from standard chuck turning — parts where L/D ratio makes standard turning impractical at specified tolerance. A Ø5mm × 50mm aluminum pin (L/D = 10:1) under 20N cutting force deflects 0.024mm at midpoint — 10× a ±0.002mm tolerance. Swiss CNC guide bushing eliminates this deflection entirely. Minimum diameter Ø0.5mm; maximum L/D 20:1; OD tolerance ±0.005mm standard, ±0.003mm precision; Ra 0.2μm from PCD; 100% laser micrometer measurement. Applications: electronics connector pin bodies, optical fiber ferrule bodies, CMM probe shafts, medical stylus tips, MEMS mechanical miniature components.

High Aspect Ratio — 20:1 L/D Slender Shafts
Slender shafts, long pins, probe bodies, and cylindrical guide elements at L/D exceeding 10:1 — the capability boundary for precision aluminum turning. For a Ø10mm × 200mm shaft (L/D = 20:1), Swiss CNC guide bushing positions the cutting tool 1mm from support — the effective L/D at the cutting point is always 0.1:1, independent of total shaft length. CNCPioneer achieves ±0.005mm OD on Ø10mm × 200mm aluminum shafts — impossible on standard chuck turning without steady rest marks and associated dimensional variation. Applications: linear guide rail bodies, long medical needle forms, optical alignment rods, sensor probe shafts, CMM stylus bodies.

Large Format — Ø100mm to Ø1,000mm
Medium and large aluminum CNC turning parts — flanges, housings, disk bodies, ring spacers, and large valve bodies — from MAZAK mill-turn centers with large chuck capacity. At Ø500mm, aluminum's CTE of 23.6 ppm/°C means a 5°C temperature difference shifts diameter by 0.059mm — requiring temperature-controlled machining for ±0.020mm accuracy. CNCPioneer applies temperature-controlled machining environment (±1°C), CMM measurement at 20°C ±0.5°C inspection room, and interrupted-cut facing strategy. Face flatness 0.020–0.050mm; bore concentricity to OD ±0.005mm; bolt circle ±0.020mm. Maximum capacity Ø1,000mm.
Industries & Applications
CNCPioneer's aluminum CNC turning parts programs serve every industry consuming precision aluminum turned components at documented dimensional accuracy — from aerospace and defense structural component suppliers requiring AS9100D FAIR through consumer electronics OEMs requiring millions of micro-turned pin bodies annually.
Aerospace
7075-T6 and 2024-T4 precision shaft bodies, structural fittings, lug bodies, and rotational components from AS9100D-certified programs. FAIR per AS9102 on all new part numbers; AMS mill certificate traceability; shot peen AMS 2430 for life-limited primary structural programs. Cpk ≥1.67 on critical dimensions. 2024-T4 preferred for fatigue-critical programs (K_IC = 33 MPa·√m versus 7075-T6's 24 MPa·√m).
Automotive
IATF 16949:2016 certified aluminum turning parts for automotive OEM supply — powertrain shaft bodies, suspension components, EV motor housing precision features, EV battery enclosure structural bodies, and EV charging connector bodies. PPAP Level 3 supply; SPC production monitoring with Cpk ≥1.67; weekly kanban delivery programs. 6061-T6 structural standard; 7075-T6 for high-stress powertrain; 6063-T5 for thermal management bodies.

Semiconductor
6061-T6 and 6063-T5 precision aluminum turning parts for semiconductor process equipment — DI water compatible electroless Ni-P aluminum fittings; precision bore housings; thermal management bodies; non-magnetic aluminum housing programs for Hall-effect sensor adjacent applications. High-phosphorus (10–12% P) electroless Ni-P for 1,000+ hour ASTM B117 corrosion resistance in DI water cooling circuits.
Medical Devices
Precision 6061-T6 and 7075-T6 aluminum turned components for medical instrumentation, surgical tool bodies, and diagnostic equipment. ISO 13485 compatible quality documentation on request; Ra 0.2μm or better surface finish on instrument body programs; biocompatible Type II anodize surface treatment. Optical fiber ferrule bodies (Ø2–5mm, ±0.002mm bore); CMM probe bodies; stylus and measurement reference standards.
Oil and Gas
6061-T6 and 7075-T6 aluminum valve bodies, cylinder bodies, and port adapter fittings with NPT/BSP threaded ports, precision bore for dynamic seal engagement (Ra 0.2μm), O-ring grooves ±0.020mm, and 100% pressure decay leak test on sealed components. Combined hex OD + NPT bore from single MAZAK mill-turn setup — no rechucking for fitting body programs.
Industrial Automation & Robotics
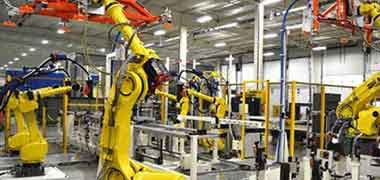
High-volume aluminum CNC turning parts for robot body components, actuator housings, gripper structural bodies, conveyor and motion system components — from simple hex standoffs at millions of units per year through complex actuator housing bodies at thousands of units per year. All under IATF 16949 production quality with weekly kanban delivery, SPC Cpk ≥1.67, and dedicated MAZAK cell allocation for blanket order programs.
Aluminum CNC Turning Parts
Process & Capabilities
CNCPioneer's aluminum CNC turning programs run on 78+ Swiss CNC lathes with guide bushing support, 66+ MAZAK mill-turn centers with live tooling and C-axis, MAZAK VARIAXIS 5-axis simultaneous platforms, and precision cylindrical grinding systems — the integrated turning, milling, and grinding capability delivering complete aluminum CNC turning parts under one AS9100D and IATF 16949 quality system.
24-Hour Quote · 48-Hour DFM Engineering Review
Alloy selection analysis from structural, thermal, corrosion, and cost requirements · Tolerance achievability assessment at specified diameter and L/D (Swiss CNC vs MAZAK vs CBN grinding recommendation) · L/D deflection analysis and guide bushing requirement determination · Surface finish process selection from Ra specification · Thread specification verification (ISO metric, UNF, NPT, BSP) · Surface treatment specification from operating environment · Coating allowance pre-built into machined target dimensions · FAIR scope definition · Complete pricing from prototype through production.
Swiss CNC Guide Bushing Turning — Ø0.5–32mm at 20:1 L/D
78+ Swiss CNC lathes delivering the deflection-free precision foundation for small and slender aluminum turning programs. Standard production: ±0.005mm OD at any L/D to 20:1; ±0.003mm from precision passes with CBN tooling; Ra 0.2μm from PCD at optimal parameters; Ra 0.1μm from CBN finish turning. Bar-fed continuous operations for high-volume micro-turning programs. Minimum diameter Ø0.5mm. Maximum diameter through guide bushing Ø32mm. In-process laser micrometer OD measurement with automatic offset correction for tool-wear diameter drift.
MAZAK Mill-Turn — Complex Aluminum Bodies, Ø10–600mm
66+ MAZAK mill-turn centers with live tooling and C-axis continuous interpolation for complex aluminum CNC turning parts combining turning, milling, and threading in one setup. Standard: ±0.010mm from turning; ±0.005mm precision turning with temperature compensation; bore concentricity to OD ±0.003mm from single-setup. Integrated features: keyways ±0.020mm, cross-holes ±0.020mm true position, bolt circles ±0.020mm, O-ring grooves ±0.020mm, NPT/BSP threads from live tooling. MAZAK VARIAXIS 5-axis for compound bore geometry in non-orthogonal orientation.
CBN Precision Cylindrical Grinding — ±0.002mm & Ra 0.05μm
Between-centers CBN cylindrical grinding extending precision beyond Swiss CNC turning capability for bearing journals, gauge-body surfaces, precision shaft ODs for interference-fit assembly, and optical-quality aluminum body surfaces. Standard precision grinding: ±0.002mm OD; ±0.001mm roundness; Ra 0.1μm. Precision grinding programs: ±0.001mm with in-process air gauge feedback. Progressive fine-grinding to Ra 0.05μm from 600-grit → 1,000-grit → spark-out 15 revolutions. Profilometer Ra verification at 5 positions per part before release.
Complete Aluminum Alloy Portfolio — SII XRF Verified
6061-T6 (276 MPa yield, general-purpose standard) · 7075-T6 (503 MPa, highest-strength standard) · 2024-T4 (324 MPa, fatigue-critical K_IC superior) · 6063-T5 (200 W/m·K, thermal management priority) · 5052-H32 (marine corrosion) · 7050-T7451 (thick-section aerospace) · 2219-T87 (cryogenic, aerospace weldable) · 2011-T3 (free-machining, −10% cost) · 1100-H14 (electrical conductor) · 6082-T6 (European 6061 equivalent). All SII XRF composition-verified and hardness-tested per temper per lot. EN 10204 3.1 or AMS mill certificate archived per lot.
AS9100D · IATF 16949 · ISO 10012 Documentation
Certificate of Conformance · 100% laser micrometer OD diameter records per lot · 100% air gauge bore records per lot · CMM dimensional report (concentricity, perpendicularity, true positions, flatness, thread positions) · Profilometer Ra records at specified locations · Thread GO/NO-GO gauge records (100% per lot) · SII XRF material composition certificates · Hardness verification per temper · Surface treatment certification with thickness and post-treatment dimensional verification · AS9102 FAIR for AS9100D programs · PPAP Level 3 for IATF 16949 automotive programs · Records retained 20 years.
Aluminum Alloys for
CNC Turning Parts
Aluminum alloy selection for CNC turning parts follows four criteria in priority order: yield strength adequacy at minimum cross-section, thermal conductivity requirement, corrosion and SCC resistance, and manufacturing cost. 6061-T6 covers approximately 60% of programs; 7075-T6 for high-stress structural; 2024-T4 for fatigue-critical; 6063-T5 for thermal management.
6061-T6 / T651
276 MPa yield · 2.70 g/cm³ · Excellent machinability · 167 W/m·K · Very good corrosion resistance. Universal structural turning: housings, fittings, shafts, brackets. Most common alloy — 60% of aluminum turning programs.
7075-T6 / T651 / T7351
503 MPa yield · 2.80 g/cm³ · Good machinability · 130 W/m·K. Highest-strength standard alloy. Aerospace structural shafts, fittings. +25–35% machining cost versus 6061-T6. T7351 for improved SCC resistance.
2024-T4 / T351
324 MPa yield · 2.78 g/cm³ · K_IC = 33 MPa·√m (versus 7075-T6's 24 MPa·√m). Preferred for fatigue-critical and damage-tolerant structural turning. Aerospace primary structure.
6063-T5
145 MPa yield · 2.70 g/cm³ · 200 W/m·K — highest thermal conductivity aluminum. Heat sink bodies, cooling plates, thermal management housings. Semiconductor equipment, EV motor stator sleeves.
5052-H32 / 5083-H321
193 MPa yield · 2.68 g/cm³ · Excellent corrosion resistance. Marine structural turning, chemical equipment, weldable structures. 5083-H321 for LNG equipment and cryogenic applications.
2011-T3 · 1100-H14 · 2219-T87
2011-T3: −10% machining cost (free-machining) for high-volume connector and fitting bodies. 1100-H14: 222 W/m·K, electrical conductor turning. 2219-T87: aerospace weldable, cryogenic liquid H₂ applications.
Surface Finish for
Aluminum CNC Turning Parts
CNCPioneer's aluminum CNC turning and grinding programs achieve the full surface finish range — from Ra 3.2μm rough structural through Ra 0.05μm optical mirror ground — with PCD tooling as the production standard for Ra 0.4μm and better, and CBN precision cylindrical grinding for sub-Ra 0.1μm bearing-quality and optical-quality surfaces.
Ra 0.4μm — Precision PCD Standard
CNCPioneer's production standard for precision aluminum CNC turning — from PCD tooling at v_c = 600–900 m/min, f = 0.015–0.030 mm/rev. Eliminates built-up edge (BUE) from the surface entirely. Applications: sliding seal surfaces, optical body exteriors, seating faces for soft-metal seals, most precision instrument body surfaces.
Ra 0.1μm — CBN Ground or PCD Diamond-Cut
From CBN cylindrical grinding at optimized parameters, or diamond turning (SPDT) at v_c = 1,000–1,200 m/min, f = 0.008 mm/rev. Applications: laser mirror mount body surfaces, precision gauge block faces, bearing spindle journals, dynamic wiper seal rod surfaces where seal life specification requires Ra ≤0.1μm.
Ra ≤0.05μm — Optical Mirror Ground
From CBN precision grinding + lapping, or single-point diamond turning (SPDT). Requires Ra 0.2μm pre-grind surface, 600-grit → 1,000-grit → spark-out 15 revolutions; profilometer verification at 5 positions per part; grinding fluid at 20°C ±0.2°C; vibration-isolated precision grinding machine. Applications: optical reference mirrors, EUV optics mounts, precision gauge master surfaces.
All surface treatments on aluminum CNC turning parts programs — Type II anodize, Type III hard anodize, electroless Ni-P, Alodine, hard chrome, and DLC coating — are documented with treatment certifications and post-treatment dimensional verification. Anodize dimensional growth (5–25μm per side) is compensated in pre-anodize machined targets and confirmed post-treatment by air gauge. Treatment selection guidance and dimensional allowance calculation are included in CNCPioneer's 48-hour DFM review at no additional cost.
Quality Assurance for
Aluminum CNC Turning Parts
CNCPioneer's aluminum CNC turning parts quality system applies laser micrometer OD verification on every precision program lot, air gauge bore verification on all precision bore programs, SII XRF 100% incoming material composition verification, and SPC Cpk ≥1.67 production monitoring — the quality infrastructure that AS9100D and IATF 16949 programs require and that general Chinese turning shops without laboratory verification infrastructure cannot provide.
48-Hour DFM & Engineering Review
Alloy selection analysis from structural, thermal, corrosion, and cost requirements. Tolerance achievability assessment at specified diameter and L/D — Swiss CNC guide bushing versus MAZAK mill-turn versus CBN precision grinding recommendation. L/D deflection analysis confirming guide bushing requirement for slender shafts. Surface finish process selection from Ra specification. Thread specification verification. Surface treatment coating allowance calculation. FAIR scope definition. All drawing ambiguities resolved before machining.
SII XRF Material Verification
SII XRF composition verification on every aluminum alloy lot before machining commitment — 6061-T6 (Mg 0.80–1.20%; Si 0.40–0.80%; Cu ≤0.40%); 7075-T6 (Zn 5.1–6.1%; Mg 2.1–2.9%; Cu 1.2–2.0%); 2024-T4 (Cu 3.8–4.9%; Mg 1.2–1.8%); 6063-T5; 5052-H32 verified per lot. Hardness verification per temper condition: 6061-T6 HRB 60–70; 7075-T6 HRB 85–92. EN 10204 3.1 or AMS mill certificate archived per lot with full traceability from certificate to production lot to part.
In-Process Control — 100% OD Laser Micrometer
100% OD laser micrometer at Swiss CNC output for all precision aluminum turning programs — every part OD measured; out-of-tolerance parts identified and quarantined before proceeding. Adaptive offset correction for tool-wear diameter drift maintaining ±0.005mm compliance without operator intervention. Bore diameter: in-process CMM or air gauge after finish boring, before part-off. Thread GO/NO-GO 100% per production lot. Surface finish profilometry per lot at specified sample frequency. Temperature verification at 20°C ±1°C before precision bore and OD measurement.
Final Inspection — CMM & Laser Micrometer
CMM: all drawing dimensions including OD diameters, bore diameters, bore concentricity to OD, face perpendicularity, true position of holes and patterns, thread position, flatness, and 5-axis angular features. Laser micrometer 100% OD on all precision aluminum turning programs (±0.010mm and tighter). Profilometry: Ra at specified locations per drawing. Roundness tester for ±0.003mm roundness specifications on precision bearing journal programs. Visual: burr-free all edges; anodize uniformity; cosmetic finish per specification.
Surface Treatment Verification
Type II anodize thickness: 5–10μm; post-anodize bore and OD dimension verified by air gauge against pre-anodize target incorporating the +5μm/side growth. Type III hard anodize thickness: 25–75μm; post-anodize bore reaming or OD grinding to final dimension where precision fit requires. Electroless Ni-P: 5–8μm per side; thickness confirmed by XRF measurement; post-plate bore reaming where bore tolerance requires post-plate correction. Hard chrome: post-chrome OD grind to ±0.005mm final diameter; profilometer Ra 0.1μm verification.
Documentation Package
Certificate of Conformance · 100% laser micrometer OD diameter records per lot · Air gauge bore records per lot · CMM dimensional report (concentricity, perpendicularity, true positions, thread positions, flatness) · Profilometer Ra records at specified locations · Thread GO/NO-GO records (100% per lot) · SII XRF material composition certification with lot traceability · Hardness verification per temper · Surface treatment certifications with thickness and post-treatment dimensional verification · AS9102 FAIR for AS9100D programs · PPAP Level 3 for IATF 16949 automotive programs · Records retained 20 years.
AS9100D & IATF 16949 Quality System
for Aluminum CNC Turning Parts
CNCPioneer's aluminum CNC turning quality system addresses the four quality dimensions specific to precision aluminum turned components: thermal management discipline for aluminum's 23.6 ppm/°C CTE, PCD tooling BUE suppression for Ra 0.4μm and better, Swiss CNC guide bushing governance for slender-part dimensional accuracy, and 100% material XRF verification for alloy traceability.
Thermal Discipline — Aluminum CTE Management
Aluminum's CTE of 23.6 ppm/°C means a 5°C temperature difference shifts a Ø50mm bore by 5.9μm — half of a ±0.010mm tolerance. CNCPioneer applies through-spindle coolant at 20°C ±0.5°C during precision turning, CMM measurement room at 20°C ±0.5°C, and workpiece temperature verification at 20°C ±1°C before precision bore measurement — the thermal discipline that produces dimensional data consistent with specification rather than tolerances that pass at machining temperature and fail at ambient measurement.
- Coolant at 20°C ±0.5°C during precision turning
- CMM room at 20°C ±0.5°C for measurement
- Workpiece temperature verified before ±0.005mm measurement
PCD Tooling BUE Suppression
Carbide turning of aluminum at standard speeds produces built-up edge (BUE) — aluminum welds to the carbide rake face at 200–400°C, deposits on the machined surface, and prevents Ra 0.4μm achievement. PCD's HV 8,000+ hardness maintains a 0.5–2.0μm edge radius versus carbide's 5–20μm, shearing aluminum cleanly without adhesion. CNCPioneer's PCD-equipped MAZAK and Swiss CNC programs achieve Ra 0.4μm as production standard — not a special process — with tool life of 100,000–1,000,000 parts between resharpens on aluminum.
- PCD standard on all Ra ≤0.8μm programs
- Ra 0.4μm production standard — not special process
- 100K–1M part tool life before resharpen
Swiss CNC Guide Bushing Deflection Governance
For Ø5mm × 50mm aluminum at L/D = 10:1, cutting force of 20N produces 0.024mm midpoint deflection — 10× a ±0.002mm tolerance. Swiss CNC guide bushing eliminates deflection by supporting the workpiece at the cutting point, making the effective L/D at the cutting point 0.1:1 regardless of total shaft length. CNCPioneer's ±0.005mm OD at 20:1 L/D is a structural guarantee from guide bushing positioning accuracy — not best-effort outcome from skilled operator managing deflection.
- ±0.005mm OD at 20:1 L/D structural guarantee
- Minimum diameter Ø0.5mm through guide bushing
- In-process laser mic with automatic offset correction
PPAP Level 3 & Volume Production
PPAP Level 3 for IATF 16949 automotive aluminum turning programs: 30-piece dimensional data; Cpk ≥1.33 on all critical dimensions (≥1.67 on IATF special characteristics); MSA Gage R&R ≤10% on CMM and laser micrometer; PFMEA covering tool wear drift, thermal expansion measurement error, and alloy substitution failure modes; Control Plan; Process Flow Diagram; PSW. Weekly or biweekly kanban delivery on established blanket orders; 2-week lead time on weekly kanban releases from 6061-T6 and 7075-T6 safety stock. 5,000,000+ annual unit capacity.
- PPAP Level 3 for IATF 16949 automotive programs
- Cpk ≥1.67 on critical OD, bore, and concentricity
- MSA Gage R&R ≤10% on laser mic and CMM
Aluminum CNC Turning Parts FAQ
Common questions from aerospace and defense component suppliers, automotive and EV Tier 1 manufacturers, semiconductor equipment builders, medical device manufacturers, and precision engineering distributors about CNCPioneer's aluminum CNC turning parts capability, tolerance achievability, alloy selection, surface finish, and volume program economics.
Tolerance capability depends on three simultaneous factors: diameter, L/D ratio, and manufacturing process. Swiss CNC guide bushing turning (Ø0.5–32mm, L/D ≤ 20:1): ±0.005mm standard production; ±0.003mm with precision passes; lower tolerance requires CBN grinding. MAZAK mill-turn turning (Ø10–600mm, L/D ≤ 8:1): ±0.010mm standard; ±0.005mm precision with temperature compensation; below ±0.005mm requires CBN precision grinding. CBN precision cylindrical grinding between centers: ±0.002mm standard; ±0.001mm with in-process air gauge feedback; ±0.0005mm from ultra-precision programs with full thermal control. Large-format turning (Ø500–1,000mm): ±0.050mm standard; ±0.020mm with temperature-compensated facing. Critical to understand: aluminum's CTE of 23.6 ppm/°C means a 5°C temperature difference shifts a Ø50mm bore by 5.9μm — for ±0.005mm tolerance programs at Ø50mm, temperature control within ±2°C during machining and ±0.5°C during measurement is required. CNCPioneer applies through-spindle coolant at 20°C ±0.5°C and CMM room at 20°C ±0.5°C for all precision aluminum turning programs at ±0.005mm and tighter.
Carbide turning of aluminum at standard speeds (v_c = 100–200 m/min) produces built-up edge (BUE) — aluminum welds to the carbide rake face at 200–400°C from aluminum's chemical affinity for cobalt binder. BUE deposits on the machined surface producing Ra 0.8–2.0μm from tearing and tool marks. Carbide at high speed (v_c = 400+ m/min) eliminates BUE thermally — Ra 0.4–0.8μm achievable but sensitive to insert wear. PCD eliminates BUE entirely: PCD's HV 8,000+ hardness produces an edge radius of 0.5–2.0μm versus carbide's 5–20μm; PCD's 560 W/m·K thermal conductivity conducts chip heat away from the cutting zone rather than accumulating at the edge. PCD surface finish on 6061-T6: Ra 0.4μm standard (f = 0.030 mm/rev, v_c = 600 m/min); Ra 0.2μm precision (f = 0.015 mm/rev, v_c = 800 m/min); Ra 0.1μm diamond-cut (f = 0.008 mm/rev, v_c = 1,000–1,200 m/min). PCD tool life in aluminum: 100,000–1,000,000 parts between resharpens — the long tool life making PCD economically dominant despite higher tool cost. CBN cylindrical grinding complements PCD turning for sub-Ra 0.1μm: Ra 0.1μm standard grinding; Ra 0.05μm precision; Ra 0.02–0.05μm with progressive lapping.
Aluminum alloy selection for CNC turning parts follows four criteria in priority order. First, yield strength adequacy: if peak stress at minimum cross-section × safety factor exceeds 6061-T6's 276 MPa yield, upgrade to 7075-T6 (503 MPa) — accepting 25–35% higher machining cost; for fatigue-critical parts, specify 2024-T4 (324 MPa, K_IC = 33 MPa·√m versus 7075-T6's 24 MPa·√m) despite lower yield than 7075-T6. Second, thermal conductivity: if the part dissipates heat, specify 6063-T5 (200 W/m·K) over 6061-T6 (167 W/m·K) accepting lower strength. Third, corrosion and SCC resistance: 7075-T7351 over 7075-T6 for sustained-tension in humid environments; 5052-H32 or 5083-H321 for marine applications. Fourth, manufacturing cost: 2011-T3 free-machining alloy reduces machining cost 15–20% below 6061-T6 at moderate strength (310 MPa UTS) for high-volume connector and fastener programs. In practice: approximately 60% of aluminum turning inquiries correctly specify 6061-T6 (DFM confirms); 20% over-specify 7075-T6 where 6061-T6 is adequate (cost reduction identified); 10% under-specify 6061-T6 where 7075-T6 is required (strength concern flagged); 10% have no alloy specified (DFM provides recommendation from part function analysis).
Prototype lead times: simple precision shaft or spacer (±0.005mm, PCD finish, anodize, FAIR) — 3–5 business days; complex multi-feature turning body (multi-bore, milled features, threads, anodize, FAIR) — 5–8 business days; CBN precision ground shaft (±0.002mm, Ra 0.1μm, FAIR) — 5–7 business days; micro-turned aluminum pins (Ø2mm, Swiss CNC, 25-piece) — 3–4 business days. Volume economics (simple shaft Ø10×50mm, 6061-T6): 2,000–10,000/year $1.75–$2.60; 200,000+/year $0.54–$0.80. Precision bushing (Ø30 OD × Ø20 bore): 2,000–10,000/year $3.10–$4.60; 200,000+/year $0.96–$1.42. Three-market comparison at 10,000/year: US precision turning (AS9100D equivalent): simple shaft $5.50–$8.50; precision bushing $10–$16. European equivalent: simple shaft $6–$10; precision bushing $12–$18. CNCPioneer China (equivalent quality): simple shaft $1.75–$2.60; precision bushing $3.10–$4.60. Cost ratio CNCPioneer/US: 0.30–0.35× — representing 63–70% cost reduction at equivalent quality. The cost advantage reflects manufacturing economics (China engineering labor, overhead, supply chain proximity) and machine fleet scaling economics — not quality compromise. CNCPioneer's AS9100D/IATF 16949 certifications, SII XRF material verification, Cpk ≥1.67 SPC monitoring, CMM verification, and AS9102 FAIR documentation represent quality infrastructure equivalent to mid-tier US and European precision turning facilities.
Type II Clear Anodize (MIL-A-8625 Type II): 5–10μm thickness, 50% growth into surface; precision bores and ODs masked during anodize; post-anodize dimension verified by air gauge; adds approximately +5μm per side to external dimensions. Type III Hard Anodize (MIL-A-8625 Type III): 25–75μm, HV 400+ on 6061-T6; +12–25μm per side; bore masking and post-anodize verification mandatory. Electroless Ni-P (MIL-C-26074): high-phosphorus 10–12% P for 1,000+ hours ASTM B117 and DI water compatibility; 5–8μm per side; post-plate bore reaming where precision fit requires. Hard Chrome (AMS 2460): post-chrome OD grind to ±0.005mm; Ra 0.1μm post-grind; RoHS exemption for precision engineering. Chromate Conversion (Alodine MIL-DTL-5541): Class 1A for EMC conductivity (contact resistance ≤5 mΩ/cm²); Class 3 trivalent for European market; <0.1μm dimensional change — no bore masking required. DLC Coating: 1–3μm PVD, HV 2,000+; ±0.001μm per side — negligible; requires Ra 0.1μm CBN-ground base surface. All treatment allowances are machined-in at the CNC turning stage and confirmed post-treatment — ensuring dimensional specifications are met in the final delivered condition. Treatment selection guidance and allowance calculation are included in CNCPioneer's 48-hour DFM at no additional cost.
Get a Quote for Aluminum CNC Turning Parts
Upload your aluminum CNC turning part drawings, 3D CAD files, or complete BOM and receive a competitive quotation within 24 hours and a complete engineering DFM within 48 hours — covering alloy selection analysis, tolerance achievability assessment, L/D deflection analysis, surface finish process selection, thread specification verification, surface treatment specification, FAIR scope, and complete pricing from prototype first articles through production supply under AS9100D or IATF 16949 quality programs.