
Grade-Specific Machining Parameters
Confirm material grade, delivery condition, finishing requirements and supporting records.
CNCPioneer is an IATF 16949 and AS9100D certified manufacturer of custom stainless steel CNC turning parts for valve bodies, valve cores, shafts, hygienic fittings, sensor housings and industrial hardware.
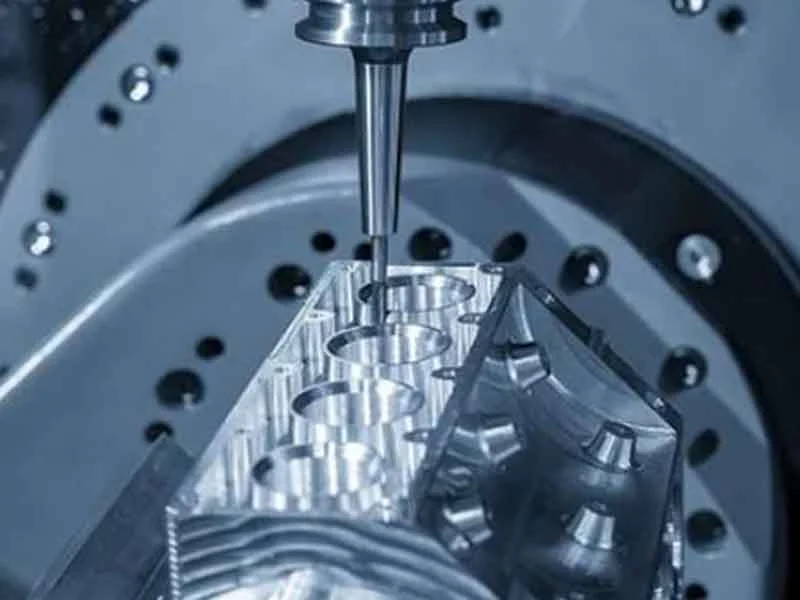
Custom stainless steel CNC turning parts are rotational components machined from corrosion-resistant and high-strength grades for valves, fluid fittings, shafts, hygienic equipment, sensors and industrial hardware.

Coordinate geometry, material, finishing and inspection around the part's intended function.
Confirm material grade, delivery condition, finishing requirements and supporting records.
Plan support and setup around critical diameters, datums and mating interfaces.
Specify journals, bores, threads and cross-features using functional datums. Review stock condition, cutting access and chip removal before agreeing the operation sequence.
Identify whether passivation, electropolishing or another finish is required. State controlled surfaces, masking and the final dimensional acceptance condition with the drawing.
Stainless parts requiring black, non-reflective finish (military optical hardware, tactical instruments, architectural hardware, precision mechanisms) need blackening that preserves corrosion resistance and dimensional accuracy.
List material certificates, dimensional reports and any customer-specific approval records. Agree document content and inspection coverage for the actual stainless steel components.
Explore representative configurations and share your drawing for a product-specific review.
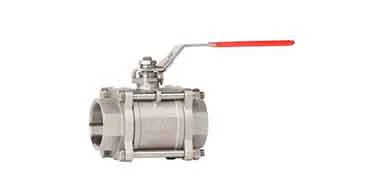
Ball valve core (420 hardened or 316L): OD ±0.003mm h6 from CBN precision grinding; sphericity ±0.003mm at 12 measurement positions; port bore Ra ≤0.4μm; stem flat angular position ±0.010°; chrome or Ni-P surface for hardened 420; passivation + electropolish for 316L.
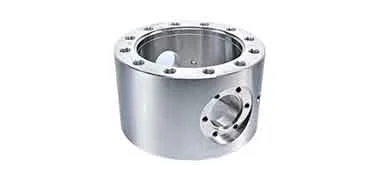
Ball valve body (Ø15–100mm, PN16–PN40): body bore ±0.010mm Ra 0.8μm; BSP/NPT/metric ports ±0.005mm; stem bore ±0.005mm perpendicular to ball bore 0.010mm; O-ring groove ±0.020mm width / ±0.010mm depth; gland nut thread ±0.005mm.
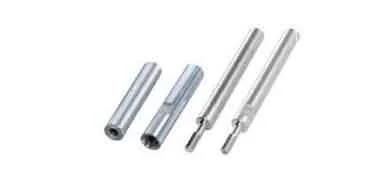
Precision Shafts machined to your drawing. Confirm material, functional dimensions and finish before production.
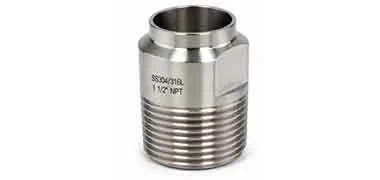
Hygienic Fittings machined to your drawing. Confirm material, functional dimensions and finish before production.
Exhaust sensor boss (316Ti or 304): M18×1.5 external thread ±0.005mm; bore ID ±0.020mm; face perpendicularity 0.010mm; ASTM A967 passivation.
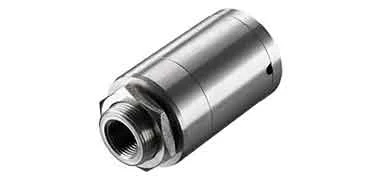
Sensor Housings machined to your drawing. Confirm material, functional dimensions and finish before production.
Stainless steel turned components for automotive, aerospace, medical, oil and gas, robotics and semiconductor equipment. Match the material, sealing features, mating fits and inspection requirements to each application.
Stainless steel sensor housings, valve components and precision shafts for vehicle assemblies. Review threads, locating diameters, corrosion protection and mating fits against the approved drawing.
Explore automotive machining
Turned shafts, sleeves, threaded fittings and actuator hardware for aircraft equipment. Define material condition, concentric features, surface finish and the inspection records required for your program.
Explore aerospace machining
Instrument shafts, connector bodies and equipment housings machined to medical device drawings. Specify material grade, burr limits, cleanable surfaces and the assembly interfaces that control fit.
Explore medical machining
Valve bodies, valve cores, threaded fittings and instrumentation housings for energy equipment. Review process media, sealing features, pressure-related drawing requirements and material traceability before production.
Explore oil & gas machining
Joint shafts, precision sleeves, locating pins and sensor housings for robot assemblies. Control bearing fits, concentricity and mounting datums, with finishing allowances defined for the mating components.
Explore robotics machining
Vacuum fittings, gas valve bodies and sensor housings for semiconductor equipment. Define stainless grade, sealing surfaces, surface treatment, cleanliness and packaging requirements for the equipment specification.
Explore semiconductor machiningMaterials
Confirm the exact grade, delivery condition and finish compatibility with your drawing.
C ≤0.030% · Cr 16–18% · Ni 10–14% · Mo 2–3% · UTS 485–690 MPa · μ_r ≤1.005.
Cr 18–20% · Ni 8–10.5% · C ≤0.080% · UTS 515–690 MPa · Non-magnetic.
S 0.15–0.35% (free-machining) · Machinability 70–80% (best stainless) · v_c = 180–250 m/min.
Cr 15–17.5% · Ni 3–5% · Cu 3–5% · HRC 44–47 H900 · UTS 1,170–1,310 MPa · Magnetic.
Confirm the exact material grade, condition, heat-treatment requirements and certificates against the approved drawing.
Finish selection
Select the finish around the specified material, functional surfaces and service conditions. Confirm process details and acceptance requirements with your drawing.
CNCPioneer's standard treatment on all 304, 316L, 316Ti, and 303 stainless CNC turning parts — not an optional add-on.
Phosphoric-sulfuric acid EP simultaneously planarizes (50–70% Ra reduction) and creates a chromium-enriched passive oxide superior to passivated-only surfaces.
Black oxide (Fe₃O₄, 1–3μm, flat matte black, <1μm dimensional change) for military hardware, optical instruments, architectural components.
Machining resources for drawing review, prototypes and repeat-production programs.
Inspection & documentation
Review material identity, machining datums, functional dimensions and production records for your component.
Final tolerances, inspection coverage and acceptance criteria are confirmed against your drawing, material and geometry.
Confirm the certificates, inspection reports and production records needed for your order when sharing your drawing.
The product range includes Valve Cores, Valve Bodies, Precision Shafts. Custom geometry is reviewed against the approved drawing.
Material options include 316L Stainless (UNS S31603), 304 Stainless (UNS S30400), 303 Stainless (UNS S30300). The exact grade and condition should be confirmed for your application.
Define critical dimensions, datums and mating features, together with datums, tolerances and required surface condition.
Finishing options include astm a967 passivation, electropolishing, blacken stainless. Applicability is reviewed against the specified material and geometry.
Pricing and delivery are confirmed after reviewing the drawing, material availability, quantity, machining route, finishing and inspection scope.
CUSTOM CNC PARTS
Share your drawing or 3D model, material, critical dimensions, finish and order quantity. We’ll review the machining route, inspection scope and delivery requirements.
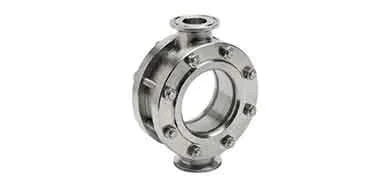 Stainless Steel Flange
 Stainless Steel Precision Turning Shafts
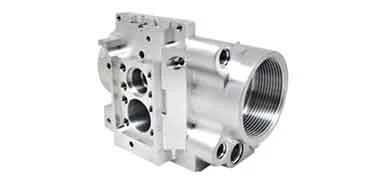 Stainless Steel 5-Axis CNC Parts
 Stainless Steel Semiconductor Parts