
Single-Setup Bore Coaxiality
Every bearing housing supporting a shaft at two or more points requires those housing bores to be coaxial.
Custom Bearing Housing made to your drawing. Review bore size, outside diameter and mating fits, material, finishing and inspection requirements before production.
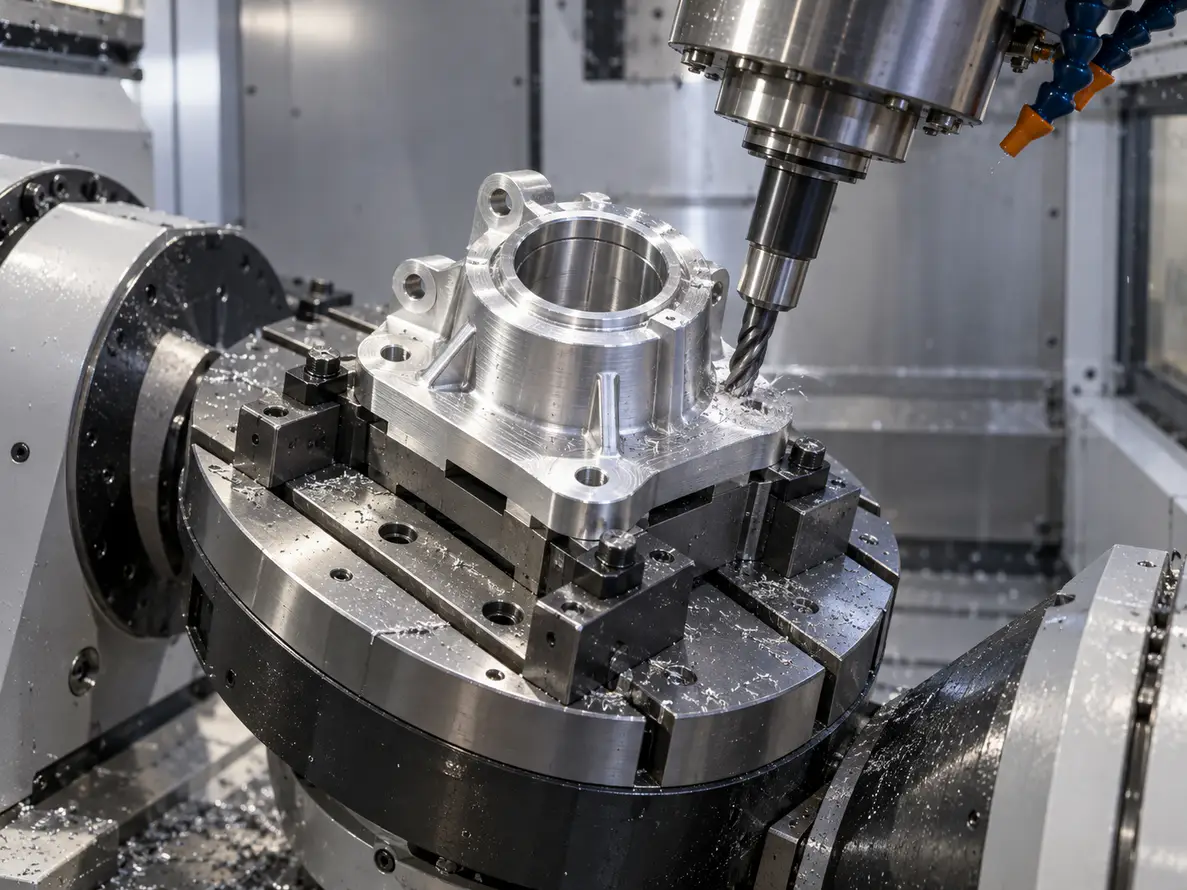
Custom bearing housings are reviewed around bore size, outside diameter and mating fits. The machining route, material, finishing and inspection plan follow the approved drawing and intended application.
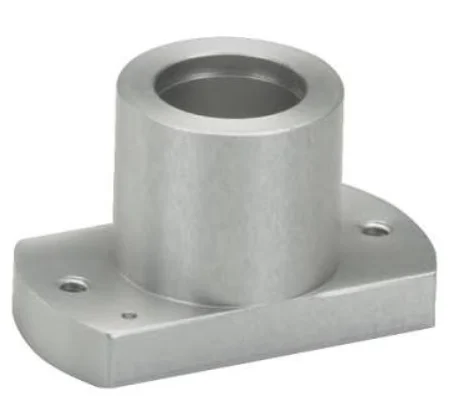
Coordinate geometry, material, finishing and inspection around the part's intended function.
Every bearing housing supporting a shaft at two or more points requires those housing bores to be coaxial.
eVTOL motor bearing housings in aluminum (CTE 23.6 ppm/°C) operating at 100°C expand the housing bore by nearly 0.1mm.
Self-lubricating PTFE-lined bushings require PCD tooling and temperature-stabilized machining for bore accuracy ±0.003mm; bronze bushings require optimized rake geometry to prevent built-up edge; PEEK bushings require fluoropolymer-adjacent machining discipline.
An eVTOL bearing housing block 50g heavier than optimum multiplies across 40–80 critical bearing interfaces to produce 2–4 kg of avoidable structural mass.
Review bore size, outside diameter and mating fits and functional requirements before defining the process.
CNCPioneer delivers eVTOL bearing housing machining at 40–60% below US and European aerospace precision shops at equivalent AS9100D tolerance and documentation.
Explore representative configurations and share your drawing for a product-specific review.

Flapping hinge bearing housing blocks (articulated rotor head) with bore ±0.003mm H7 for spherical plain bearing engagement; lug bore pair coaxiality ±0.005mm; perpendicularity of bearing bore axis to hinge pin axis 0.010mm.

Outboard motor bearing housings for overhung propeller loads with angular contact pair (DB arrangement) bores ±0.002mm and pair coaxiality ±0.005mm.

Collective pitch control spider center guide bearing housings ±0.005mm.
Landing gear pivot bearing housings in TC4 AMS 6931 STA for emergency sink-rate design loads (2.4–4.0 m/s) with FEA-verified minimum wall at impact design load × 2.0 safety factor.

Linear actuator bearing housing bodies with actuator body outer diameter interface ±0.020mm clearance fit.
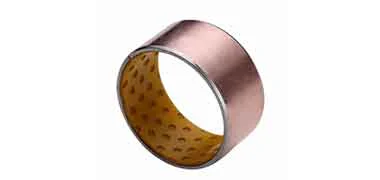
PTFE-lined self-lubricating bushings with PCD-machined bores ±0.005mm and thermal expansion allowance for CTE 100–125 ppm/°C.
Match the component to its operating environment, assembly interfaces and documentation requirements.

Custom bearing housings for aircraft actuators and accessory drive assemblies. We machine bearing bores, shoulders and mounting faces to your drawing, with material traceability and agreed dimensional inspection.
Explore aerospace machining
Bearing housings for electric motors, gearboxes and automotive drive modules. We coordinate bore concentricity, mounting-hole position and sealing interfaces, with prototype and batch production matched to your specifications.
Explore automotive machining
Bearing housings for pumps, compressors and rotating equipment. Material selection, bearing fits, seal grooves and lubrication passages are reviewed against operating temperature, corrosion exposure and maintenance needs.
Explore oil & gas machining
Bearing housings for rail vehicle auxiliary drives and gearbox assemblies. We machine bearing seats and mounting datums, with material, finish and inspection requirements reviewed for vibration and outdoor service.
Explore railroad machining
Precision bearing housings for diagnostic equipment, laboratory automation and compact drive assemblies. We review bore fit, shaft alignment, burr control and surface finish to suit your device design and cleaning requirements.
Explore medical machining
Bearing housings for wafer-handling robots, precision stages and inspection equipment. We machine bearing seats and mounting interfaces to support repeatable motion, with specified burr control, cleaning and packaging.
Explore semiconductor machiningMaterials
Confirm the exact grade, delivery condition and finish compatibility with your drawing.
Non-magnetic; CTE 8.6 ppm/°C; 950 MPa yield.
Titanium options for weight-sensitive and corrosion-resistant components. Confirm the approved grade, material condition and surface requirements.
Aluminum options for lightweight machined components. Confirm the alloy, temper, finishing allowance and critical assembly dimensions.
Aluminum options for lightweight machined components. Confirm the alloy, temper, finishing allowance and critical assembly dimensions.
Aluminum options for lightweight machined components. Confirm the alloy, temper, finishing allowance and critical assembly dimensions.
Magnetic precipitation-hardening stainless steel. Specify the H900 condition, required surface treatment and dimensional inspection against the approved drawing.
Stainless steel options for corrosion-resistant components. Confirm the grade, delivery condition, surface finish and cleaning requirements.
Confirm the exact material grade, condition, heat-treatment requirements and certificates against the approved drawing.
Finish selection
Select the finish around the specified material, functional surfaces and service conditions. Confirm process details and acceptance requirements with your drawing.
Standard corrosion protection for 7075-T6 and 6061-T6 aluminum eVTOL bearing housing bodies — 5–10μm clear anodize preventing moisture corrosion while maintaining electrical insulation.
Review shot peen against the material, functional surfaces and intended service conditions.
Review electroless nickel against the material, functional surfaces and intended service conditions.
All 316L and 17-4PH stainless eVTOL bearing housing components — passivation restores passive oxide layer at all machined surfaces; documented per ASTM A967 method for manned aviation program material records.
Diamond-like carbon (1–3μm, μ 0.05–0.15, HV 2,000+) for PEEK and metal bushing bore running surfaces in high-cycle eVTOL pitch control applications.
Chromate conversion coating for aluminum bearing housings and bushing mounting bodies requiring electrical conductivity alongside corrosion protection.
Machining resources for drawing review, prototypes and repeat-production programs.
Inspection & documentation
Review material identity, machining datums, functional dimensions and production records for your component.
Final tolerances, inspection coverage and acceptance criteria are confirmed against your drawing, material and geometry.
Confirm the certificates, inspection reports and production records needed for your order when sharing your drawing.
The product range includes Rotor System Bearing Housings, Motor and Drivetrain Bearing Housings, Flight Control System Bearing Housings. Custom geometry is reviewed against the approved drawing.
Material options include TC4 Titanium AMS 4928, TC4 Titanium AMS 6931 STA, 7075-T6 Aluminum AMS-QQ-A-225. The exact grade and condition should be confirmed for your application.
Define bore size, outside diameter and mating fits, together with datums, tolerances and required surface condition.
Finishing options include type ii/iii anodize, shot peen, electroless nickel. Applicability is reviewed against the specified material and geometry.
Pricing and delivery are confirmed after reviewing the drawing, material availability, quantity, machining route, finishing and inspection scope.
CUSTOM CNC PARTS
Share your drawing or 3D model, material, critical dimensions, finish and order quantity. We’ll review the machining route, inspection scope and delivery requirements.
 CNC Turning Bearing Housings
 Sensor Housing 5-Axis Machining Part
 Bearing Bushing
 EV Housing CNC Machining