
Server Component
CNC Manufacturing
CNCPioneer is an IATF 16949 and AS9100D certified server component CNC manufacturing specialist and OEM server component machining factory delivering high-reliability server platform mechanical hardware through complete server parts CNC fabrication programs — 78+ Swiss CNC lathes and 66+ MAZAK mill-turn centers for structural chassis elements, thermal management components, storage mechanical parts, power infrastructure bodies, connector interface hardware, and rack structural components for hyperscale operators, AI accelerator platform developers, enterprise server OEMs, and custom server hardware CNC machining programs worldwide since 2011.
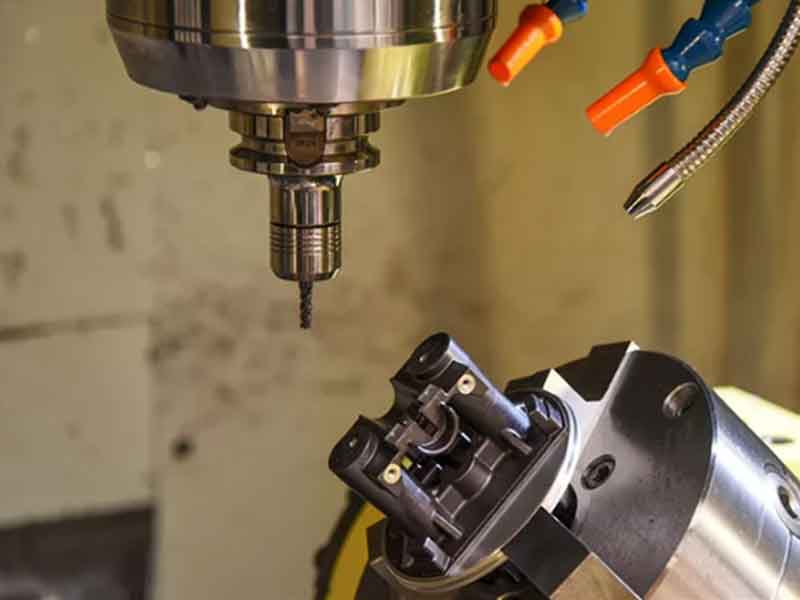
What Is Server Component
CNC Manufacturing?
Server component CNC manufacturing is the precision engineering and production discipline encompassing the complete set of manufacturing operations — CNC turning, milling, drilling, boring, threading, and finishing — applied to aluminum, copper, stainless steel, and specialty alloy stock to produce the mechanical components that constitute enterprise server hardware, data center infrastructure equipment, and high-performance computing platforms across the full lifecycle from design concept through commercial volume deployment.
Server component CNC manufacturing differs from general precision CNC manufacturing in three defining characteristics: documentation depth (RoHS 2011/65/EU material compliance, full lot traceability, PPAP or FAIR quality documentation); assembly interface precision (connector cutout position ±0.050mm, guide rail width ±0.080mm consistent across production quantities); and design collaboration (custom server hardware CNC machining DFM partnership that prevents costly design iterations, identifies manufacturing feasibility issues before tooling investment, and optimizes server hardware designs for the manufacturing processes that achieve required tolerances at competitive production economics).
-
Complete server hardware BOM coverage in single OEM relationship Chassis structural hardware, thermal management components, storage mechanical parts, power system enclosures, connector interface elements, and rack integration structural hardware — CNCPioneer's server component CNC manufacturing eliminates the 4–8 supplier qualification programs that multi-source conventional server parts CNC fabrication requires, replacing them with a single supplier qualification covering the complete server mechanical BOM.
-
IATF 16949 production quality for server parts CNC fabrication OEM server component machining programs supplying server assembly lines require IATF 16949 — PPAP Level 3 documentation confirming manufacturing process capability, Cpk ≥1.67 on critical dimensions, 100% CCD automatic sorting eliminating dimensional escapes, and MSA Gage R&R confirming measurement system adequacy. CNCPioneer's IATF 16949 certification provides this complete automotive-grade quality framework for server parts CNC fabrication programs where server OEM assembly line zero-defect requirements match automotive production quality standards.
-
5–7 day prototype plus prototype-to-volume continuity Server hardware development programs operate on 12–18 month concept-to-commercial-launch timelines. CNCPioneer delivers first article aluminum server component CNC manufacturing prototypes in 5–7 business days, then maintains the same machining programs, tooling, and process parameters from prototype through volume production — ensuring production server components are dimensionally identical to the prototype components used in server hardware qualification testing.
-
40–60% China OEM server component machining cost advantage CNCPioneer's China-based server component CNC manufacturing factory delivers 40–60% cost reduction versus equivalent OEM server component machining from US, European, and Japanese precision machining facilities — DFM review, PPAP documentation, RoHS/REACH compliance, and conflict mineral reporting included in China server component CNC manufacturing pricing without surcharges.

Why CNCPioneer — OEM Server
Component Machining Partner
CNCPioneer's server component CNC manufacturing capability combines MAZAK mill-turn multi-axis machining for complex server housing bodies and thermal management assemblies with Swiss CNC lathe fabrication for miniature server hardware connector bodies and precision shaft elements — providing OEM server component machining customers with single-source server parts CNC fabrication across the complete server hardware mechanical portfolio.
Complete Server Hardware BOM in Single OEM Relationship
CNCPioneer's server component CNC manufacturing covers chassis structural hardware, thermal management, storage mechanical parts, power system enclosures, connector interface elements, and rack integration structural hardware — eliminating the 4–8 supplier qualification programs that multi-source conventional server parts CNC fabrication requires, replacing them with a single supplier qualification covering the complete server mechanical BOM.
Engineering DFM Partnership for Custom Server Hardware
Custom server hardware CNC machining programs succeed when manufacturing feasibility is evaluated during design — not after tooling investment. CNCPioneer's 24-hour DFM review identifies dimensional tolerance feasibility, material machinability, surface treatment compatibility, and assembly interface compliance before prototype commitment — preventing the design iterations that compress server hardware program timelines and inflate development budgets.
IATF 16949 Production Quality for Server OEM Assembly Lines
OEM server component machining supplying server assembly lines requires PPAP Level 3 documentation, Cpk ≥1.67 on critical dimensions, 100% CCD sorting eliminating dimensional escapes, and MSA Gage R&R confirming measurement system adequacy — the complete automotive-grade production quality framework that server OEM zero-defect assembly requirements demand from qualified server parts CNC fabrication suppliers.
5–7 Day Prototype, Prototype-to-Volume Continuity
First article aluminum server component CNC manufacturing prototypes in 5–7 business days, supporting bi-weekly design iteration cycles that compressed server hardware development timelines require. CNCPioneer then maintains the same machining programs, tooling, and process parameters from prototype through volume — ensuring production server components are dimensionally identical to the prototype components used in server hardware qualification testing.
MAZAK Mill-Turn + Swiss CNC Dual Process Platform
66+ MAZAK mill-turn centers (Ø10mm–Ø500mm; ±0.003mm positional accuracy; 5-axis simultaneous for compound-geometry server hardware) for complex server chassis bodies, thermal management assemblies, and storage structural components — combined with 78+ Swiss CNC lathes (Ø0.5–Ø32mm; ±0.002mm; L/D up to 20:1) for miniature server connector bodies, retention pivot pins, and precision shaft elements.
40–60% China Server Component CNC Manufacturing Cost
CNCPioneer's China-based OEM server component machining delivers 40–60% cost reduction versus equivalent server component CNC manufacturing from US, European, and Japanese facilities — DFM review, PPAP documentation, RoHS/REACH compliance, and conflict mineral reporting per Dodd-Frank Section 1502 included in China server component CNC manufacturing program pricing. Single prototype pieces accepted with no minimum order requirement.
Server Parts CNC Fabrication
— Complete Program Scope
CNCPioneer's server parts CNC fabrication covers every component category in the server hardware mechanical bill of materials — providing OEM server component machining customers with comprehensive fabrication coverage from a single qualified supplier relationship with IATF 16949 PPAP Level 3 or AS9100D FAIR documentation.

Structural Server Component CNC Manufacturing
Server chassis and enclosure bodies (chassis profile ±0.200mm for EIA-310-D compliance; connector cutout ±0.050mm; motherboard standoff ±0.050mm; mating flange flatness 0.005mm; Alodine Class 3 on EMC surfaces), server midplane structural bodies (connector array flatness 0.005mm; blade guide rail pitch ±0.030mm), and PCIe expansion bay and GPU carrier structures (riser mounting flatness 0.005mm; OAM module guide pin bore ±0.020mm; GPU auxiliary power cable routing ±0.200mm; mechanical retention bracket ±0.050mm). Material: aluminum 6061-T6 primary; 7075-T6 for weight-critical GPU carrier hardware.

Thermal Management Server Component CNC Manufacturing
Air-cooled heat sink arrays (fin pitch ±0.050mm; fin height ±0.050mm; base flatness 0.003mm; heat pipe groove ±0.020mm; Intel LGA4677/AMD SP5 mounting hole ±0.050mm; aluminum 6063-T5 for maximum thermal conductivity), liquid cooling server component fabrication (GPU cold plate contact flatness 0.003mm; channel width ±0.050mm; O-ring groove ±0.020mm; 100% pressure decay leak testing; copper C11000 ETP for high-flux programs), and thermal interface hardware (vapor chamber cavity perimeter ±0.050mm; heat pipe evaporator groove array ±0.020mm; thermal spreader-to-socket frame 0.003mm flatness).

Storage System Server Component CNC Manufacturing
Hot-swap NVMe/SAS/SATA drive carriers (guide rail ±0.080mm; SFF-8639/SFF-8611 blind-mate clearance ±0.050mm; 6-32 UNC boss ±0.050mm per JEDEC MO-297; anti-vibration grommet pocket ±0.030mm; latch click-in ±0.050mm; aluminum Type II anodized or 304 stainless for high-cycle programs), storage bay and backplane structural fabrication (standoff array ±0.050mm; drive bay rail flatness 0.010mm), and enterprise JBOD enclosure internal components (60-bay rail array ±0.100mm; SAS expander mounting ±0.100mm; hot-swap fan tray guide ±0.150mm).

Power System Server Component CNC Manufacturing
PSU mechanical housing fabrication (guide rail ±0.100mm; bus bar contact ±0.050mm; PMBus connector ±0.050mm; PSU retention latch ±0.050mm; Alodine Class 3 on bus bar contact zones), power distribution and bus bar hardware in copper C11000 ETP (bus bar contact flatness 0.005mm; cross-section ±0.100mm; Ra 0.4μm contact surface; electroless nickel oxidation protection), and VRM thermal hardware (heat sink boss height ±0.020mm; retention spring clip ±0.030mm; phase assembly contact surface 0.005mm flatness for uniform thermal pad coverage).

Fan, Airflow & Connector Interface CNC Manufacturing
Fan module housing and retention hardware (guide rail ±0.080mm; blind-mate connector engagement ±0.050mm; retention click-in ±0.050mm; vibration isolation boss ±0.030mm), airflow baffle and plenum structural fabrication (seating surface flatness 0.020mm; snap-fit retention ±0.100mm; cable routing aperture ±0.200mm), PCIe and high-speed interconnect hardware (slot connector height ±0.030mm for PCIe Gen5/Gen6 signal integrity; card guide width ±0.050mm; CXL/Ethernet cable backshell bore ±0.020mm; InfiniBand HDR/NDR strain relief ±0.050mm), and BMC/IPMI management interface structural hardware (dedicated management port RJ45 cutout ±0.030mm).

Rack Integration & Data Center Infrastructure CNC
19-inch rack cabinet structural hardware per EIA-310-D (vertical rail U-position hole pattern ±0.100mm; corner post profile ±0.300mm; cable management arm mounting ±0.100mm; side panel retention ±0.150mm), OCP Open Rack V3 structural components (rail profile ±0.300mm; 48V horizontal busbar mounting ±0.100mm; thermal management structural element ±0.200mm), cable management hardware (routing finger boss ±0.050mm; horizontal panel bracket ±0.100mm), and intelligent PDU mechanical bodies (IEC 60320 C13/C19 outlet ±0.100mm; copper C11000 ETP distribution block; current transformer mounting bore ±0.020mm).
Industries & Applications
CNCPioneer's server component CNC manufacturing and OEM server component machining serves hyperscale cloud infrastructure operators, AI and ML server platform developers, enterprise server OEMs, storage system manufacturers, telecommunications infrastructure builders, edge computing hardware developers, HPC infrastructure providers, and defense server system integrators worldwide.
Hyperscale Cloud Infrastructure
Server component CNC manufacturing for Amazon Web Services, Microsoft Azure, Google Cloud, Meta, and Chinese hyperscale operator custom server hardware programs — OCP server node mechanical components, Open Rack V3 structural hardware, custom GPU server mechanical elements, AI training server structural components, and data center infrastructure hardware at deployment volumes requiring complete RoHS documentation and blanket order monthly delivery scheduling.
AI & Machine Learning Server Platforms
Custom server hardware CNC machining for AI training and inference infrastructure — NVIDIA HGX-compatible mechanical hardware, AMD OAM server structural components, custom AI accelerator chassis mechanical elements, NVLink bridge alignment precision brackets, and AI training cluster rack integration structural components for hyperscale AI infrastructure buildout programs requiring both mechanical precision and complete RoHS documentation.
Enterprise Server OEMs
OEM server component machining for Dell Technologies, HPE, Lenovo, Supermicro, and Inspur enterprise server product programs — complete server mechanical hardware portfolio production supply covering chassis structural elements, storage drive carriers, fan module housings, PSU mechanical hardware, PCIe bracket assemblies, and thermal management components with IATF 16949 PPAP Level 3 quality documentation for enterprise server OEM supply chain qualification.
Storage Systems & Telecommunications
Server parts CNC fabrication for Pure Storage, NetApp, Dell EMC, IBM, and Chinese storage OEM all-flash array and hybrid storage programs — NVMe/SSD drive carrier fabrication, JBOD enclosure structural components, and storage array backplane mounting hardware. Also: CNC machining for server components in 5G network hardware — 5G baseband unit chassis mechanical elements, CU/DU server structural hardware, and Open RAN server components meeting NEBS Level 3 environmental specifications.
Edge Computing & HPC Infrastructure
Custom server hardware CNC machining for ruggedized edge server programs — IP67-sealed chassis elements, vibration-rated structural hardware, DIN rail server mounting hardware, wide-temperature-range server components, and industrial edge computing mechanical elements for transportation, energy, and manufacturing edge deployments. Also: server component CNC manufacturing for HPC cluster infrastructure — InfiniBand switch chassis components, HPC compute node structural hardware, and custom HPC rack structural elements.
Defense & Government Computing
AS9100D certified OEM server component machining for defense server programs — ruggedized tactical server chassis components, armored vehicle computing hardware, shipborne server mechanical elements, portable field computing structural hardware, and classified network infrastructure server components with MIL-STD-810 qualification and FAIR documentation per AS9102. MIL-A-8625 Type III hard anodize and MIL-DTL-5541 Alodine Class 3 surface treatments for defense server hardware procurement qualification.
OEM Server Component Machining
Program Architecture
CNCPioneer's OEM server component machining programs represent long-term supply partnerships where CNCPioneer functions as the qualified precision manufacturing arm of the server OEM's mechanical component supply chain — delivering consistent production quality across server platform lifetimes measured in years rather than individual production orders.
Engineering Partnership Establishment
Complete server hardware mechanical architecture review identifying all CNC machining for server components within the server hardware mechanical BOM · Server OEM automated assembly process parameters reviewed against achievable server component CNC manufacturing dimensional accuracy — confirming guide rail widths, connector clearance geometries, and snap-fit retention features are compatible with robotic assembly tolerance windows · Quality documentation requirements mapped to CNCPioneer's IATF 16949 quality system capabilities before OEM program commitment · 24-hour DFM review for every custom server hardware CNC machining inquiry with complete cost analysis at prototype through volume tiers.
Development Prototype Server Component CNC Manufacturing
First article aluminum server component prototypes in 5–7 business days · Complex multi-material server component sets in 10–14 business days · MAZAK mill-turn (Ø10–Ø500mm; ±0.003mm; 5-axis simultaneous) for complex server chassis bodies and thermal assemblies · Swiss CNC lathes (Ø0.5–Ø32mm; ±0.002mm; L/D up to 20:1) for miniature server connector bodies and precision server hardware shaft elements · Complete CMM dimensional documentation with first article report · Same-day DFM feedback on design modifications tested in rapid successive prototype cycles supporting bi-weekly server hardware iteration.
Production Qualification — PPAP Level 3
Process capability study: Cpk ≥1.67 on all IATF 16949 special characteristics; Cpk ≥1.33 on product characteristics · MSA Gage R&R confirming gauge variation ≤10% of tolerance on all gauging systems · PFMEA identifying all server component CNC manufacturing failure modes with detection controls · Control plan specifying measurement types, frequencies, and reaction plans for all critical server component dimensions · Complete PPAP package: dimensional results, material certifications, RoHS declaration, Part Submission Warrant signed by CNCPioneer quality manager · FAIR per AS9102 for defense server programs.
Volume OEM Server Component Machining Supply
Monthly blanket order delivery scheduling aligned with server OEM production calendar · Dedicated production capacity ensuring monthly releases never delayed by competing programs · Adaptive SPC toolpath correction: real-time control charts on critical server component dimensions with automatic CNC offset correction before dimensions approach specification limits · 100% CCD automatic sorting on critical server component dimensions in high-volume programs · Complete lot-level documentation with every OEM server component machining shipment · Annual volume capacity: 500,000–5,000,000 aluminum server parts (MAZAK); 5,000,000–15,000,000 miniature server hardware (Swiss CNC).
Server Parts CNC Fabrication Materials
Al 6061-T6 (167 W/m·K; dominant at ~70% of programs) · Al 6063-T5 (200 W/m·K; heat sink arrays) · Al 7075-T6 (503 MPa yield; GPU carriers, weight-critical) · Al 5052-H32 (marine/outdoor) · Copper C11000 ETP (391 W/m·K; cold plates, bus bars) · Stainless 304 / 316L / 17-4PH H900 (1,310 MPa yield) · Cold-rolled steel (rack structural hardware) · Magnesium AZ91D (1.81 g/cm³; blade server) · Ti-6Al-4V (aerospace server) · PEEK (ESD-sensitive inserts) — all SII XRF verified with full RoHS compliance documentation.
Quality Documentation
IATF 16949 PPAP Level 3 for OEM server component machining programs · AS9102 FAIR for defense server programs · 100% CMM dimensional reports · Thread gauge verification records · 100% pressure decay leak test records for liquid cooling server components · Surface treatment certifications · RoHS Declaration of Conformity per IEC 62321 · REACH SVHC declaration · Conflict mineral reporting per Dodd-Frank Section 1502 · Certificate of Conformance · Records retained 10 years minimum (15 years for automotive-grade programs).
Material Programs for
Server Parts CNC Fabrication
Material selection for server parts CNC fabrication balances six dimensions: thermal conductivity for heat management components; specific strength for mass-critical structural components; machinability at required tolerances; corrosion resistance for outdoor and harsh environment server deployments; RoHS regulatory compliance; and surface treatment compatibility. Aluminum 6061-T6 covers approximately 70% of CNCPioneer's server component CNC manufacturing volume for its optimal balance across all six criteria.
6061-T6
167 W/m·K · 276 MPa yield · Excellent machinability · Anodizable · RoHS compliant · Dominant server parts CNC fabrication material (~70% of programs). Server chassis structural bodies, drive trays, fan housings, rack structural hardware, PCIe bracket components, and general server hardware. Optimal balance of structural strength, machinability for complex server part geometry, anodize and Alodine surface treatment compatibility, and cost efficiency for server OEM production programs.
6063-T5
200 W/m·K · 214 MPa yield · Maximum aluminum thermal conductivity · Extrusion alloy · RoHS compliant · Server heat sink fin arrays where 6063-T5's higher thermal conductivity versus 6061-T6 produces measurably lower fin array thermal resistance at identical geometry. Extruded server chassis profile sections with integrated thermal management surfaces in server hardware designs combining structural and thermal functions.
7075-T6 & 5052-H32
7075-T6: 503 MPa yield · 2.80 g/cm³ · RoHS compliant · GPU carrier hardware, aerospace server structural fittings, and weight-critical custom server hardware CNC machining programs where maximum yield strength enables minimum chassis section at required structural load. 5052-H32: excellent saltwater corrosion resistance · Marine edge server hardware and outdoor server enclosure structural elements exceeding 6061-T6 service life in coastal environments.
304 Stainless
Good corrosion resistance · 7.93 g/cm³ · RoHS compliant · PCIe brackets, server drive carrier components, slide rail hardware, and server rack components requiring corrosion resistance in data center humidity environments and durability for repeated server field service contact across 5–10 year data center deployment lifetimes. Cost-effective stainless for indoor data center server hardware programs.
316L Stainless
Superior corrosion resistance · Non-magnetic · FDA compatible · RoHS compliant · Outdoor edge server hardware in coastal and industrial environments, medical server components adjacent to patient areas requiring non-magnetic construction, and corrosive coolant cold plate programs where 316L provides chemical resistance that aluminum and copper cannot achieve in chloride-containing or oxidizing server cooling environments.
Cold-Rolled Steel & 17-4PH H900
Cold-rolled steel: high stiffness · low cost · zinc plating for RoHS compliance · standard server rack cabinet structural hardware at hyperscale deployment volumes. 17-4PH H900: 1,310 MPa yield · excellent corrosion resistance · RoHS compliant · high-strength server mechanism hardware, precision server structural fittings, and defense server structural elements where maximum yield strength and corrosion resistance are simultaneously required at minimum section thickness.
C11000 ETP
391 W/m·K · 8.94 g/cm³ · Maximum thermal and electrical conductivity · RoHS compliant · Server bus bars, heat pipe evaporator bases, and GPU direct-contact cold plates where copper's 2.3× thermal conductivity advantage over aluminum governs server component thermal performance. Server PDU distribution blocks and chassis-to-PSU power bus bar contacts (flatness 0.005mm; Ra 0.4μm) for minimum resistance at server power distribution interface.
Magnesium AZ91D
1.81 g/cm³ (35% below aluminum) · Good machinability · RoHS compliant · Blade server chassis and portable server hardware where magnesium's lowest density of all structural metals enables maximum blade server density within blade chassis weight constraints. Ultra-lightweight custom server hardware CNC machining programs for portable military computing and airborne server platforms where chassis mass is a primary performance constraint.
Ti-6Al-4V
880 MPa yield · 4.43 g/cm³ · Non-magnetic · Excellent corrosion resistance · RoHS compliant · Aerospace server structural fittings, ruggedized defense server hardware, and server components in proximity to magnetically sensitive navigation sensors. AS9100D FAIR documentation for aerospace server Ti-6Al-4V programs. Highest specific strength of any server hardware material enabling minimum mass at required structural loads in weight-critical airborne and portable computing platforms.
PEEK Engineering Grade
Chemical resistant · Electrical insulator · RoHS compliant · ESD-sensitive server hardware inserts and isolated server hardware elements where direct metal-to-metal contact between server structural hardware and ESD-susceptible server electronic components creates electrostatic discharge risk. Server chassis electrical isolation barriers per IEC 62368-1 safety isolation requirements. Chemical-resistant server component inserts in cooling fluid-exposed server assembly environments.
C3604 Brass
Excellent machinability · 115 W/m·K · RoHS compliant · Server connector body inserts, precision server hardware small parts, and miniature server mechanical components requiring maximum Swiss CNC lathe machinability for high-volume production at minimum cycle time. Server hardware threaded insert adapter components, server chassis pillar elements, and precision server small parts produced at volumes of millions of units annually on Swiss CNC lathe platform.
Custom Alloy Programs
White-box ODM server design-build programs and hyperscale custom server hardware programs frequently specify non-standard material combinations — Invar 36 (CTE 1.3 ppm/°C) for dimensionally stable optical server chassis inserts, beryllium copper C17200 for high-cycle spring contact server retention hardware, or aluminum-copper composite cold plates combining aluminum manifold mass efficiency with copper contact zone thermal performance. CNCPioneer's server component CNC manufacturing supports custom alloy material programs with DFM review, material procurement, and RoHS compliance documentation.
Surface Treatments for
Server Component CNC Manufacturing
Surface treatment selection for server component CNC manufacturing balances RoHS 2011/65/EU compliance, EMC bonding continuity (Alodine Class 3 on chassis assembly joints), wear resistance at high-cycle server field service surfaces (Type III hard anodize), corrosion protection for data center and outdoor edge server deployment environments, and appearance quality for branded server hardware exterior surfaces in OEM product programs.
Type II Clear Anodize
Standard corrosion protection for aluminum server component CNC manufacturing programs in indoor data center environments. 5–15μm coating for server chassis structural hardware, storage drive trays, and rack structural components. Electrically insulating — all EMC mating surfaces are masked before anodizing and treated separately with Alodine Class 3 to maintain RF shielding continuity at server chassis assembly joints. RoHS compliant.
Type III Hard Anodize — MIL-A-8625
Wear-resistant anodize (HV 400+) for high-cycle server hardware — hot-swap drive tray guide rails (thousands of insertions), fan module housings (annual replacement cycles), PCIe card guide rails (repeated card installation), and server chassis elements subject to repeated field service access across 5–10 year data center deployment lifetimes. Standard for defense server hardware and ruggedized edge server enclosures requiring both wear resistance and maximum corrosion protection. RoHS compliant.
Alodine Class 3 & Class 1A — MIL-DTL-5541
Alodine Class 3: electrically conductive trivalent chromate (Cr³⁺) for aluminum server component CNC manufacturing EMC bonding surfaces — contact resistance ≤5 mΩ/cm² at server chassis assembly joints, connector bracket bonding tabs, and PCIe bracket contact surfaces for FCC Part 15 Class A compliance. Alodine Class 1A: maximum corrosion protection for outdoor edge server hardware, solar inverter server components, and marine environment server structural hardware. Both RoHS-compliant Cr³⁺ formulations.
Passivation — ASTM A967 & Electroless Nickel
Passivation: mandatory for all stainless steel server component CNC manufacturing — PCIe brackets, drive carriers, slide rails, and outdoor edge server hardware. Removes machining free iron for maximum corrosion resistance in data center humidity environments. Electroless nickel MIL-C-26074: corrosion protection for copper server bus bars, heat pipe evaporator surfaces, and liquid cold plate internal channels — uniform plating across complex bus bar and channel geometry maintaining dimensional compliance post-plating. Both RoHS compliant.
Vacuum Bake-Out
Zinc plating: cost-effective corrosion protection for steel server rack structural hardware, cable management frames, and server PDU mounting elements in standard indoor data center environments at hyperscale deployment volumes where per-unit material cost governs total deployment economics. Black oxide: low-reflectance surface for server structural components in machine vision-guided server assembly operations where bright metallic surfaces create camera illumination interference affecting automated assembly accuracy. Both RoHS compliant.
Powder Coat & Black Anodize
Powder coat: durable branded color appearance for custom server hardware CNC machining exterior surfaces requiring specific RAL colors for server OEM brand identity in commercial server product programs — applied over Alodine primer on aluminum server components for combined corrosion protection and branded cosmetic finish. Black anodize: low-reflectance surface for server structural components in machine vision-guided server assembly and optical inspection environments where bright metallic surfaces create camera illumination interference affecting automated assembly accuracy. Both RoHS compliant.
All server component CNC manufacturing surface treatments — Type II and Type III anodize MIL-A-8625, Alodine Class 3 and Class 1A MIL-DTL-5541, passivation ASTM A967, electroless nickel MIL-C-26074, zinc plating, powder coat, and black anodize — comply with RoHS 2011/65/EU restricted substance requirements. Surface treatment certifications and bath chemistry compliance records are included in the documentation package for every server parts CNC fabrication program. Surface treatment selection — including Alodine masking zone definition for combined EMC and corrosion protection programs — is included in CNCPioneer's 24-hour server component CNC manufacturing DFM review service.
Quality Assurance for Server Component
CNC Manufacturing
CNCPioneer's IATF 16949 and AS9100D certified server component CNC manufacturing quality system provides the statistical quality infrastructure that server OEM automated assembly processes require — PPAP documentation eliminating incoming inspection burden, adaptive SPC maintaining Cpk ≥1.67 throughout production runs, and complete RoHS compliance documentation supporting global server hardware market access.
Engineering Contract Review
Complete engineering review of CNC machining for server components drawing requirements, applicable EIA-310-D, OCP hardware, JEDEC storage connector, PCI-SIG, IEC 60320, RoHS 2011/65/EU material compliance, and customer server OEM specifications before server component CNC manufacturing order acceptance. Server assembly interface tolerance analysis confirming dimensional specifications compatible with server OEM automated assembly process requirements during 24-hour DFM review.
Material Incoming Inspection & RoHS Verification
SII XRF composition verification on every server component CNC manufacturing material lot confirming alloy grade and all RoHS 2011/65/EU restricted substance thresholds. Hardness testing for heat-treated server hardware alloys including 7075-T6 and 17-4PH H900. RoHS restricted substance declaration review on all material and surface treatment chemistry certifications. Full lot traceability from mill certificate through finished server component manufacturing shipment.
PPAP Level 3 & FAIR Qualification
Complete PPAP Level 3 for IATF 16949 OEM server component machining programs: process capability study (Cpk ≥1.67 on SC dimensions), MSA Gage R&R (gauge variation ≤10% of tolerance), PFMEA, control plan, dimensional results, material certifications, RoHS declaration, and PSW signed by CNCPioneer quality manager. Customer approval required before volume production release. FAIR per AS9102 for AS9100D defense server component programs.
Adaptive SPC & Production Quality Control
Real-time SPC control charts on critical CNC machining for server components dimensions — connector cutout positions, guide rail widths, chassis flange flatness — with ±3σ control limits and automatic CNC offset correction when patterns indicate dimensional drift from tool wear or thermal expansion, maintaining Cpk ≥1.67 throughout complete production lots of 10,000–100,000 server components. Dedicated tooling programs per OEM server component machining part number. 100% CCD automatic sorting for high-volume programs.
Final CMM Inspection
Mitutoyo CMM (±0.001mm) full dimensional report. Surface roughness measurement on thermal interface surfaces and EMC mating surfaces. Thread gauge verification for all server component CNC manufacturing threaded features. Visual inspection for burrs on guide rail edges, connector clearance surfaces, and chassis mating flanges. 100% pressure decay leak test records for liquid cooling server components. First-off and last-off CMM verification bracketing each production lot with dimensional evidence.
Documentation Package
Certificate of Conformance, CMM dimensional report, material certifications with full lot traceability, RoHS Declaration of Conformity per IEC 62321, REACH SVHC declaration, conflict mineral reporting per Dodd-Frank Section 1502, surface treatment certifications, PPAP Level 3 or FAIR per AS9102, and complete server component CNC manufacturing program documentation with every shipment. Records retained 10 years minimum; 15 years for automotive-grade programs.
IATF 16949 Quality System for
OEM Server Component Machining
CNCPioneer's IATF 16949 certified OEM server component machining factory applies the automotive-grade statistical quality framework that eliminates server OEM incoming inspection burden — PPAP documentation confirming process capability, adaptive SPC maintaining dimensional compliance across complete production lots, and complete RoHS/REACH documentation supporting global server hardware market access and supply chain ESG reporting requirements.
IATF 16949 PPAP Level 3 Qualification
Complete PPAP Level 3 package for OEM server component machining supply chain qualification: design records confirming production intent; process flow diagram covering complete server parts CNC fabrication sequence; PFMEA identifying all failure modes; control plan specifying measurement types, frequencies, and reaction plans for all critical server component dimensions; MSA Gage R&R (gauge variation ≤10% of tolerance); initial capability study (Cpk ≥1.33 on product characteristics; Cpk ≥1.67 on IATF special characteristics); dimensional results; and PSW signed by CNCPioneer quality manager. Customer approval before production release.
- PPAP Level 3 for OEM server programs
- Cpk ≥1.67 on special characteristics
- MSA Gage R&R ≤10% of tolerance
Adaptive SPC for High-Volume Dimensional Consistency
Real-time SPC control charts on critical server component dimensions with automatic CNC toolpath offset correction before dimensions approach specification limits — maintaining Cpk ≥1.67 throughout complete production lots of 10,000–100,000 server components without operator intervention. Dedicated tooling inventory per OEM server component machining part number. Production process travelers with exact CNC program numbers, tool specifications, and cutting parameters preventing shift-to-shift process variation. First-off and last-off CMM verification bracketing each production lot.
- Adaptive SPC with auto toolpath correction
- Dedicated tooling per OEM program
- First-off and last-off CMM verification
RoHS, REACH & Material Traceability
SII XRF composition verification on every server component CNC manufacturing material lot confirming alloy grade and all RoHS restricted substance thresholds. Signed RoHS Declaration of Conformity per IEC 62321, REACH SVHC substance declaration (no SVHC above 0.1% w/w), and conflict mineral documentation per Dodd-Frank Section 1502 — included as standard documentation with every server parts CNC fabrication shipment supporting server OEM supply chain ESG reporting requirements and global server hardware regulatory market access.
- XRF RoHS verification every lot
- RoHS / REACH / conflict mineral docs
- Full lot traceability mill cert to ship
AS9100D for Defense Server Programs
AS9100D certified OEM server component machining for defense computing programs — ruggedized tactical server chassis components, armored vehicle computing hardware, shipborne server mechanical elements, and portable field computing structural hardware with FAIR documentation per AS9102, risk management, configuration control, MIL-A-8625 Type III hard anodize, and MIL-DTL-5541 Alodine Class 3 surface treatment compliance for defense server hardware procurement program qualification by government contracting authorities.
- AS9102 FAIR for defense server programs
- MIL-specification surface treatments
- Risk management & configuration control
Server Component CNC Manufacturing FAQ
Common questions from hyperscale cloud operators, AI server OEMs, enterprise server manufacturers, storage system producers, and defense server system integrators about CNCPioneer's server component CNC manufacturing capabilities, OEM server component machining program architecture, custom server hardware CNC machining, and server parts CNC fabrication volume programs.
OEM server component machining is distinguished from standard precision machining by three systematic differences. First, manufacturing program permanence: OEM server component machining establishes permanent manufacturing programs — fixed CNC programs, dedicated tooling, qualified process parameters, and production control plans — that remain in place across years of production supply, ensuring production server components are dimensionally identical to the qualification components tested during server hardware program launch. Second, statistical quality infrastructure: OEM server component machining operates under IATF 16949 PPAP qualification with documented process capability (Cpk ≥1.67), production SPC monitoring, 100% CCD sorting for critical server hardware dimensions, and complete lot documentation — a quality infrastructure investment that standard precision machining order-by-order programs do not justify. Third, supply relationship scope: OEM server component machining encompasses engineering partnership during server hardware development, prototype fabrication, PPAP qualification, and volume production in a single continuous relationship — providing server OEM customers with server component supply chain partners rather than transactional job shops.
Four server hardware design features consistently create CNC machining for server components manufacturing challenges that CNCPioneer's DFM review addresses before prototype investment. First, pocket depth-to-width ratio in server chassis structural bodies — pockets deeper than 4× their minimum width require extended flute end mills that deflect under cutting forces, producing dimensional variation in pocket side walls and floor flatness; DFM review identifies deep-narrow pockets and recommends geometry modification or split-machining approach. Second, blind-mate connector clearance geometry at near-zero clearance — server connector blind-mate geometries sometimes specify clearance below statistical manufacturing capability, creating connector binding during server assembly automation; DFM review recommends tolerance relaxations maintaining functional engagement without binding while improving server assembly automation reliability. Third, thin-wall aluminum server chassis sections below 2.0mm — walls below 2.0mm distort under machining cutting forces and thermal stresses, creating flatness and dimension variation that exceeds specification; DFM review recommends minimum 2.0mm wall thickness or alternative cross-section geometry. Fourth, threaded features in thin boss sections — M3 and M4 tapped holes in boss sections below 3mm wall thickness risk thread stripping under server assembly torque; DFM review recommends helicoil insert installation or boss geometry modification providing adequate thread engagement length.
CNCPioneer maintains OEM server component machining dimensional consistency across high-volume production through four integrated control mechanisms. First, adaptive SPC toolpath correction: real-time SPC control charts monitor critical server component dimensions throughout production — when patterns indicate dimensional drift from tool wear or thermal expansion, the CNC program automatically applies calculated tool offset corrections before dimensions approach specification limits, maintaining Cpk ≥1.67 across complete production lots of 10,000–100,000 server components without operator intervention. Second, dedicated tooling programs: OEM server component machining programs maintain dedicated tooling inventory assigned exclusively to each server hardware component program — eliminating the tooling variable contribution to dimensional variation. Third, production process traveler control: each server component lot moves through all CNC machining for server components operations under a dedicated process traveler specifying exact CNC program numbers, tool specifications, cutting parameters, and inspection requirements. Fourth, first-off and last-off dimensional verification: every production run begins with first-off CMM verification confirming setup compliance, and ends with last-off CMM verification confirming dimensional stability — bracketing the production lot with dimensional evidence that all components produced met specification requirements.
CNCPioneer's custom server hardware CNC machining for AI server infrastructure covers five primary program categories. First, OCP and proprietary GPU carrier hardware: custom structural carrier frames, OAM module guide hardware, and NVLink bridge alignment precision brackets for NVIDIA H100/H200/B100 and AMD MI300X GPU accelerators in OCP OAM or custom PCIe card form factors. Second, liquid cooling integration hardware: custom GPU direct-attach cold plate mechanical components (0.003mm contact flatness; 100% pressure decay leak tested), HGX baseboard cold plate manifold structural elements, and rack-level liquid cooling distribution hardware for 300–1,000W per GPU heat loads that air cooling cannot manage. Third, AI inference edge server hardware: compact server chassis mechanical elements and passive cooling integration structural hardware for AI inference edge platforms deployed without data center infrastructure support. Fourth, custom AI rack integration hardware: AI training cluster rack structural hardware — rack-to-rack interconnect structural elements, network fabric cabling management structural components, and custom power distribution bus bar hardware for dense AI training cluster rack configurations. Fifth, AI server mechanical qualification hardware: custom server hardware CNC machining for mechanical qualification and environmental testing fixtures — server component vibration test fixtures, thermal cycling test hardware, and mechanical reliability qualification apparatus for AI server platform certification programs.
CNCPioneer's server parts CNC fabrication lead times: prototype aluminum server components 5–7 business days; complex multi-component server hardware prototype sets 10–14 business days; PPAP Level 3 qualification for OEM server component machining programs 6–8 weeks from prototype approval. Production volume lead times: standard aluminum server hardware 3–5 weeks; complex server component programs with integrated fastener services and surface treatment 4–6 weeks; OEM server component machining blanket order monthly releases 2–3 weeks per release for established programs with dedicated production capacity. Annual volume capacity: simple aluminum server structural components 500,000–5,000,000 units annually on MAZAK mill-turn platform; miniature Swiss CNC server component hardware 5,000,000–15,000,000 units annually. Inventory stocking programs for high-volume OEM server component machining accounts maintain 4–8 weeks safety stock at CNCPioneer's Shenzhen facility enabling same-day shipment against monthly release orders — eliminating supply chain disruption risk from logistics delays or unexpected server OEM production demand spikes. Dedicated capacity reservation programs commit production floor time to customer server component programs guaranteeing monthly delivery without competition from other programs.
Get a Quote for Server Component CNC Manufacturing
Upload your server hardware component drawing or CAD file and receive a free DFM review and competitive server component CNC manufacturing quotation within 24 hours. CNCPioneer's engineering team will review your server parts design for CNC machining feasibility, confirm dimensional tolerances for server assembly automation compatibility, evaluate custom server hardware CNC machining material selection for RoHS compliance, assess OEM server component machining documentation requirements, identify critical server component dimensions requiring SPC monitoring, develop PPAP qualification scope and timeline for OEM programs, and provide complete pricing at prototype through volume production tiers for server component CNC manufacturing, custom server hardware CNC machining, and server parts CNC fabrication wholesale programs.